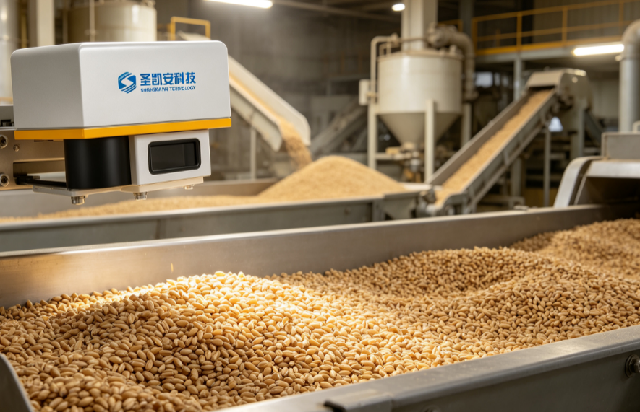
Product Introduction
Infrared online moisture detector for chemical powder, real-time moisture content analysis device for chemical production line powder
一、产品概述
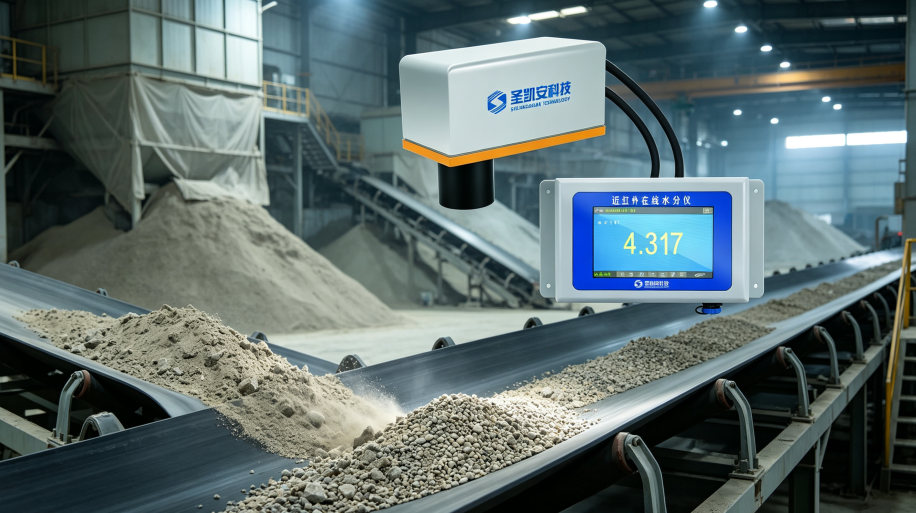
Infrared online moisture detector for chemical powder, real-time moisture content analysis device for chemical production line powder(also known as near-infrared moisture analyzer, online moisture detection system) is aNear-infrared Spectroscopy Analysis PrincipleNon-contact industrial real-time moisture detection equipment. The equipment utilizes the characteristic absorption of specific near-infrared light bands by water molecules, and through optical detection, spectral analysis, and algorithm calculation, accurately measures the moisture content on the surface and inside of materials in real time, without sampling, drying, or contacting materials, and can continuously monitor materials on the production line 24/7.
This equipment is widely adaptable to production lines for various solid particles, powders, flakes, and fibrous materials, completely solving the pain points of traditional sampling testing such as lag, large errors, low efficiency, and inability to control production in real time, providing precise data support for industrial automation production, quality control, energy consumption optimization, and capacity improvement, and is the core detection equipment for modern intelligent manufacturing and refined production.
II. Working principle
Online infrared moisture meterThe optical probe of the equipment emits near-infrared light of specific wavelengths, irradiating the surface of materials moving on the production line. Water molecules selectively absorb specific spectral bands. The probe collects the reflected spectral signals in real time, converts optical signals into electrical signals, and transmits them to the main control system.
The system relies on built-in high-precision algorithm models, filters interference factors such as dust, light, material thickness, and color, quickly calculates real-time material moisture content data, and outputs standard signals to connect withPLC、DCS, industrial control systems, achieving real-time data display, automatic adjustment, over-limit alarm, and completing automated closed-loop control of moisture detection.
III. Core product advantages
- Non-contact non-destructive testing: non-contact with materials, no damage to product form, no wear, no pollution, suitable for high-cleanliness and high-specification production scenarios in food, building materials, chemical, and light industries.
- Real-time continuous detection: millisecond-level response speed,2424-hour continuous online monitoring, real-time feedback of material moisture fluctuations, completely eliminating the lag of laboratory sampling detection mode.
- High detection accuracy and strong stability: equipped with intelligent anti-interference algorithms, automatically compensating for detection errors caused by ambient light, dust, material thickness, and color differences, ensuring stable and accurate measurement data.
- Extremely strong compatibility: supports4-20mA、RS485and other standard industrial signal outputs, seamlessly connecting to factory industrial control systemsPLC, touch screen, host computer, adaptable to automated production line transformation.
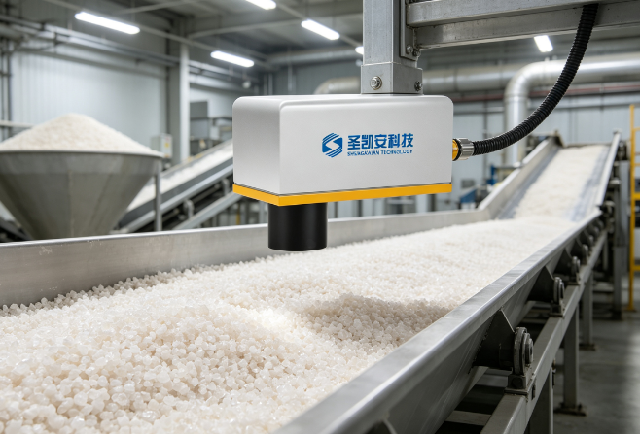
- Easy installation and simple maintenance: modular structural design, flexible installation on belt conveyor lines, chutes, silos, discharge ports, etc., no consumable parts, no frequent calibration required later, extremely low maintenance costs.
- Intelligent data control: supports real-time data display, data storage, historical curve query, over-limit audible and visual alarm, assisting production personnel in timely adjusting process parameters and stabilizing product quality.
- Adapt to complex conditions: whole machine dustproof, moisture-proof, anti-interference design, optional explosion-proof model, adaptable to harsh production environments such as dust, humidity, and strong industrial interference.
IV. Main Functional Features of Chemical Powder Infrared Online Moisture Detector Chemical Production Line Powder Moisture Content Real-time Analysis Device
- Online infrared moisture meterReal-time online moisture content detection, second-level data updates, dynamic monitoring of material moisture changes;
- Intelligent algorithm automatic calibration, no data drift over long-term use, good measurement repeatability;
- Supports storage of multiple material models, one-click switching of tested materials, adaptable to multi-category production;
- Automatic alarm for moisture exceeding standards, real-time data upload, supporting closed-loop control of production processes;
- Modular split structure, host and probe separated, adaptable to various on-site installation conditions;
- Low power consumption design, stable operation, low noise, suitable for long-term continuous industrial operation.
V. Applicable industries and tested materials
This equipment has extremely strong versatility and can adapt to the vast majority of solid industrial materials.Online moisture detection, the core application industries are as follows:
- Paper and packaging industry: paper, paperboard, corrugated paper, containerboard, pulp, etc.;
- Wood and artificial board industry: wood chips, wood powder, shavings, boards, bamboo and wood boards, density board raw materials, etc.;
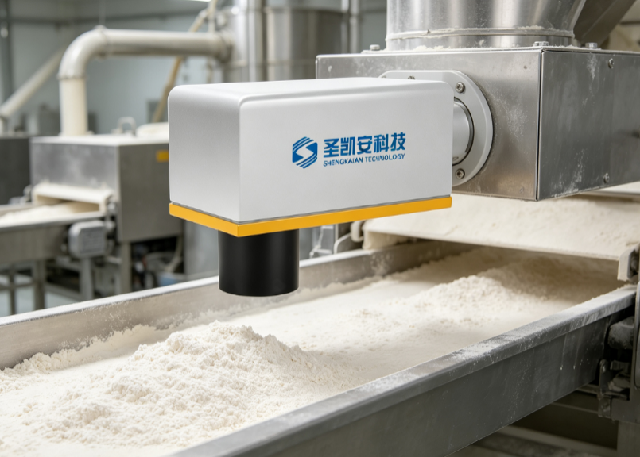
- Grain and feed industry: flour, coarse grains, feed pellets, feed powder, grain raw materials, etc.;
- Tobacco and tea industry: tobacco leaves, cut tobacco, stem silk, various dried teas, processed tea materials, etc.;
- Building materials, mining, and chemical industry: sand, gravel, mineral powder, slag, fertilizer powder, chemical raw material powder, etc.;
- Rubber, plastic, and light industry: plastic pellets, plastic granules, resin powder, rubber and plastic raw materials, etc.;
VI. Equipment application value
- Stabilize product quality: real-time monitoring of material moisture, avoiding finished product moisture content exceeding or falling below standards, reducing defect rate and rework rate;
- Improve production efficiency: replacing manual sampling testing, eliminating sampling, drying, and testing processes, greatly improving production flow efficiency;
- Save production costs: precise moisture control reduces material loss and drying energy consumption, optimizes production processes, and lowers enterprise operating costs;
- Support intelligent manufacturing: achieving production data visualization and process control automation, adapting to factory intelligent and digital upgrade needs;
- Standardized production control: full-process data traceability, meeting industry quality inspection, environmental assessment, and standardized production audit requirements.
VII. Equipment composition
The entire equipment consists ofNear-infrared detection probe (measuring head)+ Intelligent main control transmitter+ Display terminal+ Signal transmission moduleComposition, simple structure, flexible assembly, customizable installation methods and measurement ranges based on on-site conditions, contact details:xiaojianfeng@nesensor.com
Main Application Areas
- Chemical Manufacturing — Monitor moisture content in chemical powders during production to ensure product quality and consistency.
- Pharmaceutical Industry — Verify moisture levels in pharmaceutical powders and granules to meet strict regulatory standards.
- Food Processing — Measure moisture in powdered food ingredients like milk powder, flour, and spices for optimal shelf life.
- Minerals and Mining — Control moisture in mineral powders and ores to improve processing efficiency and reduce energy costs.
Keywords:chemical powder moisture analyzer, online moisture detector, NIR moisture meter, infrared moisture analyzer, real-time moisture measurement, industrial moisture sensor, powder moisture content, process moisture control