Product Introduction
Explosion-proof Near-infrared Moisture Analyzer Online Monitoring Equipment for Aggregates in Special Construction Areas
I. Product Overview of Explosion-proof Near-infrared Moisture Meter for Online Monitoring of Aggregates in Special Construction Areas
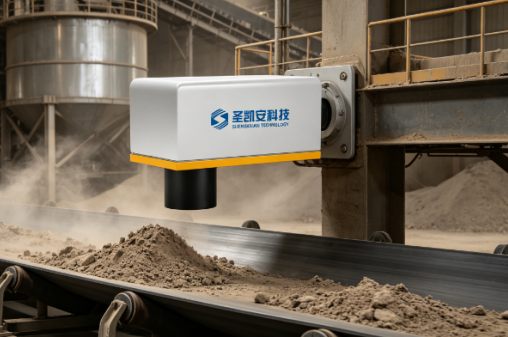
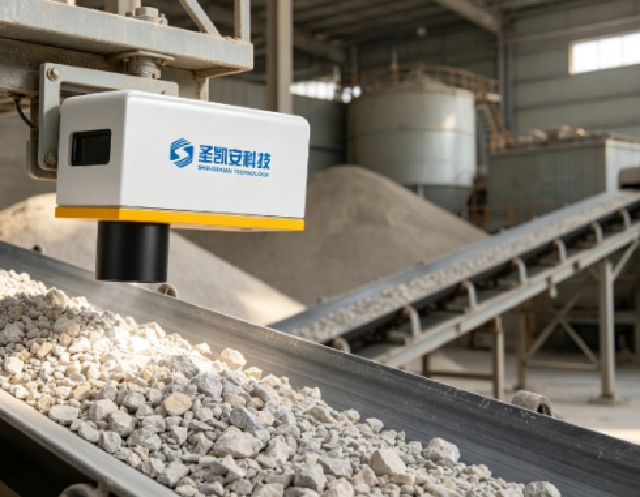
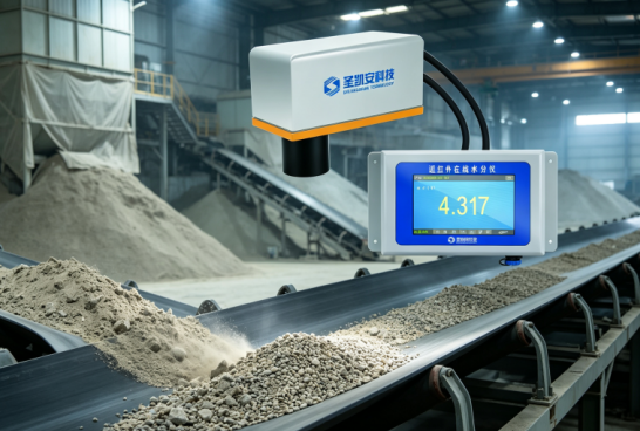
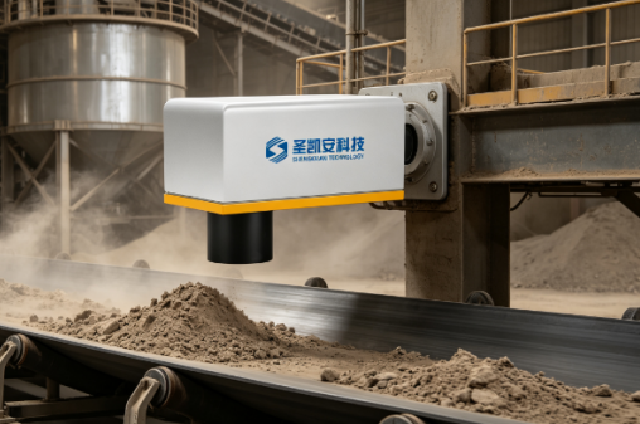
This near-infrared online moisture meter is an industrial-grade real-time detection device custom-developed for the commercial concrete industry, mainly used for online monitoring of surface free moisture in aggregates such as manufactured sand, river sand, and crushed stone on mixing plant conveyor belts. Traditional manual sampling and drying testing methods have long intervals and poor sample representativeness. Minor fluctuations in aggregate moisture content can alter the concrete water-to-binder ratio, causing quality issues such as unstable slump, bleeding and segregation, substandard strength, and pump line blockages. This equipment uses a non-contact optical detection method, allowing rapid moisture measurement while materials are dynamically conveyed on the belt, transmitting moisture content data in real time to the mixing PLC batching system, achieving automatic correction of mixing water and helping commercial concrete enterprises realize intelligent quality control in production.
II. Detection Principle of Explosion-proof Near-infrared Moisture Meter for Online Monitoring of Aggregates in Special Construction Areas
The equipment emits near-infrared light in the characteristic absorption band of water molecules to irradiate flowing sand and gravel materials. By collecting the reflected spectral signals of the materials and combining them with a dedicated aggregate algorithm and temperature compensation model, it performs high-speed calculations to output precise moisture content values. The entire process requires no sampling and no contact with the materials, truly achieving uninterrupted non-destructive testing on the production line.
III. Equipment Composition and Hardware Performance
The entire explosion-proof near-infrared moisture meter system for online monitoring of aggregates in special construction areas consists of a near-infrared moisture probe, a field control host, an automatic air purge dust-proof component, and a mounting bracket. The probe's protection rating is adapted to harsh conditions in mixing plants, including high dust, strong vibration, and large temperature differences. It comes with a lens purge device to reduce contamination of optical lenses by dust. Supports 4 20mA、RS485 Modbus Multiple signal outputs, compatible with the vast majority of new and old mixing control systems on the market, enabling rapid integration and installation whether for new plant support or intelligent upgrades of old sites.
IV. Core Product Advantages
- 24 hour continuous real-time monitoringto eliminate the data lag problem caused by manual testing;
- data-linked batching system,automatically deducting water to adjust the formulato stabilize the concrete water-to-binder ratio and finished product quality;
- Supports independent calibration and modeling for various sand and gravel materials, adapting to aggregates from different mining areas and specifications;
- Optical detection requires no consumables, and later maintenance is simple, reducing long-term usage costs;
- Full data storage, retaining moisture change curves and production logs, with quality inspection records traceable and exportable;
- Automatic alarm for abnormal moisture, avoiding in advance the production losses from batch scrap and site returns.
V. Applicable Scenarios
Mainly applied to aggregate feeding belts in commercial concrete mixing plants, discharge monitoring of sand and gravel production lines, and moisture content control of dry-mix mortar raw materials; suitable for commercial concrete plants supporting housing construction, bridges, highways, and municipal infrastructure, accommodating both new intelligent mixing plants and digital upgrades of traditional mixing plants. A laboratory benchtop moisture meter can serve as a reference device for regular calibration of the online probe's accuracy.
VI. Application value
Through precise and stable aggregate moisture control, it ensures consistent performance of each batch of concrete, reducing product scrap and engineering quality risks; optimizing cement and admixture consumption, saving raw material costs; reducing the workload of quality inspectors in repeated drying and testing, promoting automation and digital upgrades in mixing plant production, and enhancing the market competitiveness of enterprises.
Main Application Areas
- Concrete Mixing Plants — Real-time moisture measurement of aggregates to optimize water addition and ensure consistent concrete quality.
- Construction Material Production — Monitoring moisture in sand, gravel, and other aggregates for accurate batching in asphalt or cement production.
- Special Construction Zones — Explosion-proof design suitable for hazardous areas where flammable gases or dust may be present, ensuring safe online moisture monitoring.
Keywords:explosion-proof moisture meter, NIR moisture analyzer, online moisture measurement, aggregate moisture sensor, construction moisture detector, near-infrared moisture meter, industrial moisture meter, AMT/SFY-HW