Product Introduction
Infrared water-sensitization sensors are available for blast protection.
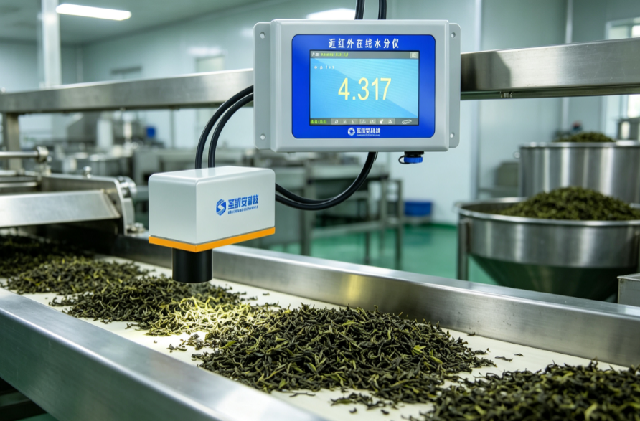
Infrared water-sensitization sensors are available for blast protection.It's an attachment.The principle of near-infrared spectrum analysisIndustrial-scale non-exposure real-time water-bearing detection equipment, specially designed for automated production lines. The core principle of equipment is the exclusive absorption of near-infrared light sources in specific bands by water molecules, the continuous release of stable light sources from working time probes, exposure to dynamic material surfaces of current water lines, the real-time collection of spectral signals after material reflection, the rapid completion of signal analysis and data calculations through built-in high-precision smart algorithms, and the output of accurate water-bearing values in milliseconds. No manual sampling, no exposure to materials, no drying and waiting for the equipment to be completedContinuous, 24-hour monitoring to completely eliminate the lag in traditional methods of testing and to match the full range of industrial production needs.
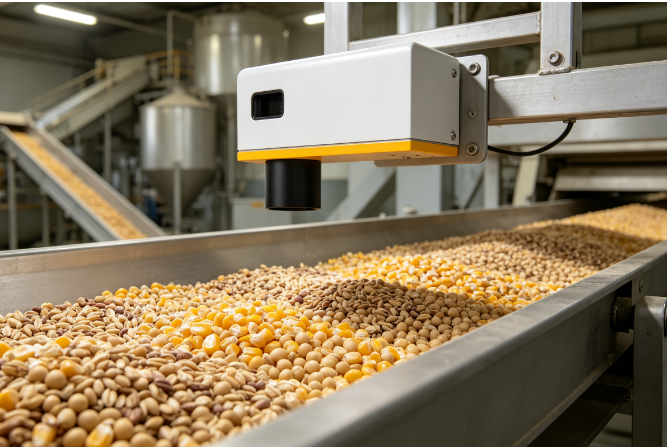
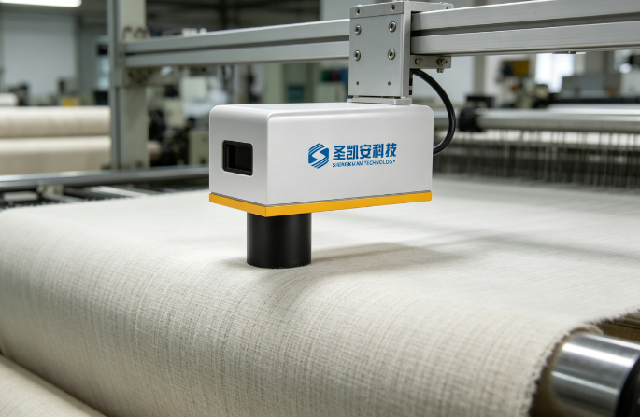
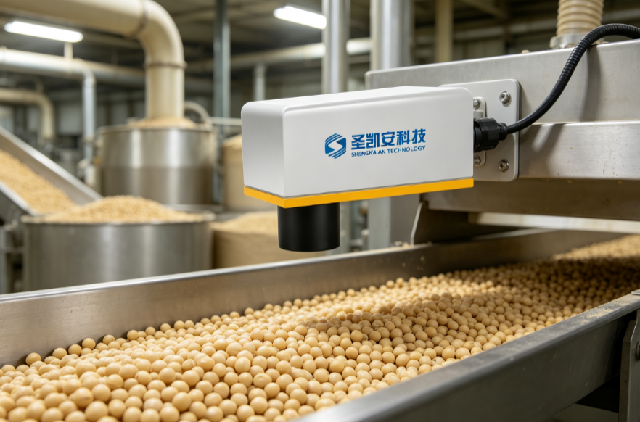
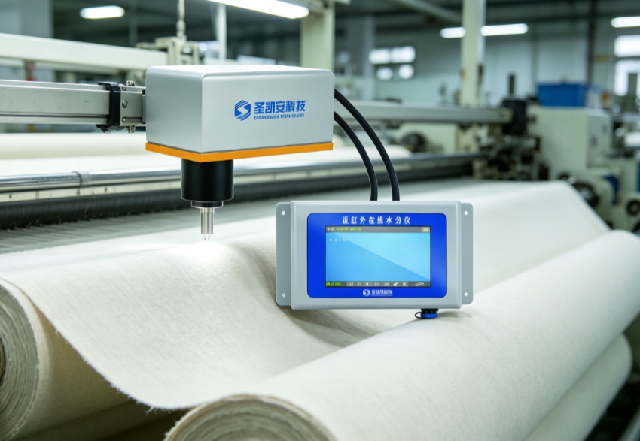
The equipment follows a mature modular structure consisting of high-precision detection probes and smart master transformers, which are simple, flexible and adaptable to a variety of field conditions, such as belt flow lines, material sluices, storage tanks, feed outlets, etc., and are easily debugged without the need to modify the original production equipment. Intelligent anti-disruption compensation algorithms that carry autonomous R & D on board can automatically offset on-site dust, environmental light fluctuations, differences in material colour, uneven external interference in material thickness, effectively avoid detection errors, and guarantee the long-term operation of equipment with accurate, stable and repetitive measurements. At the same time, the equipment is non-removable, does not require frequent calibration, significantly reduces the cost of late transportation and manual inputs, and adapts to complex industrial production environments for long periods of time.
Infrared water-sensoring sensors for chemical mining production line materials are compared to traditional manual drying tests, stationary sampling tests, etc. The equipment's speed of detection, real-time synchronization of data, etc., has fundamentally addressed the industrial pains of the slowness of traditional detection data, the partiality of sampling, the wide margin of error, and the lack of real-time control processes. Device Coding4-20mA analogue, RS485 digital volume double-circuit industrial signal output, automated systems such as seamless docking plants PLC, DCS, OTM, real-time uploading of moisture data, full backtracking of data, automatic alerts of over-standards, automatic fine-tuning of process parameters, completion of production water control closed loops, digitalization of aided production lines and intellectual upgrading.
The equipment is extremely popular and has a variety of solid-state materials, such as powders, particles, tablets and fibres, and is widely used in a wide variety of industries, such as cardboard, wood panels, food flour, feed oils, tobacco tea, textile fabrics, rubber particles, fertilizer and mining materials., the details of the use can be linkedxiaojianfeng@nesensor.comI don't know. Through real-time monitoring of water fluctuations in the production of all-process materials, precision control of production processes can effectively stabilize the quality of finished products and significantly reduce the subproduct rate, while optimizing production processes such as drying and formation, reducing material loss and energy waste and improving overall production efficiency. The equipment has become a core package of modern industrial precision production, standardized controls, reduced efficiency and enabling enterprises to achieve high-quality, intelligent production, thanks to the robust suitability of stable, fast-track peacekeeping。
Main Application Areas
- Chemical Industry — Online moisture monitoring in chemical powders, granules, and pastes to ensure product quality and process control.
- Mining Industry — Measurement of moisture content in ores, concentrates, and bulk materials for efficient processing and quality assurance.
- Food Processing — Moisture control in food ingredients and products to maintain consistency and shelf life.
- Building Materials — Monitoring moisture in sand, cement, and other aggregates for accurate batching and quality control.
Keywords:NIR moisture sensor, explosion-proof moisture analyzer, online moisture measurement, infrared moisture meter, industrial moisture sensor, chemical moisture analyzer, mining moisture sensor, high precision moisture sensor