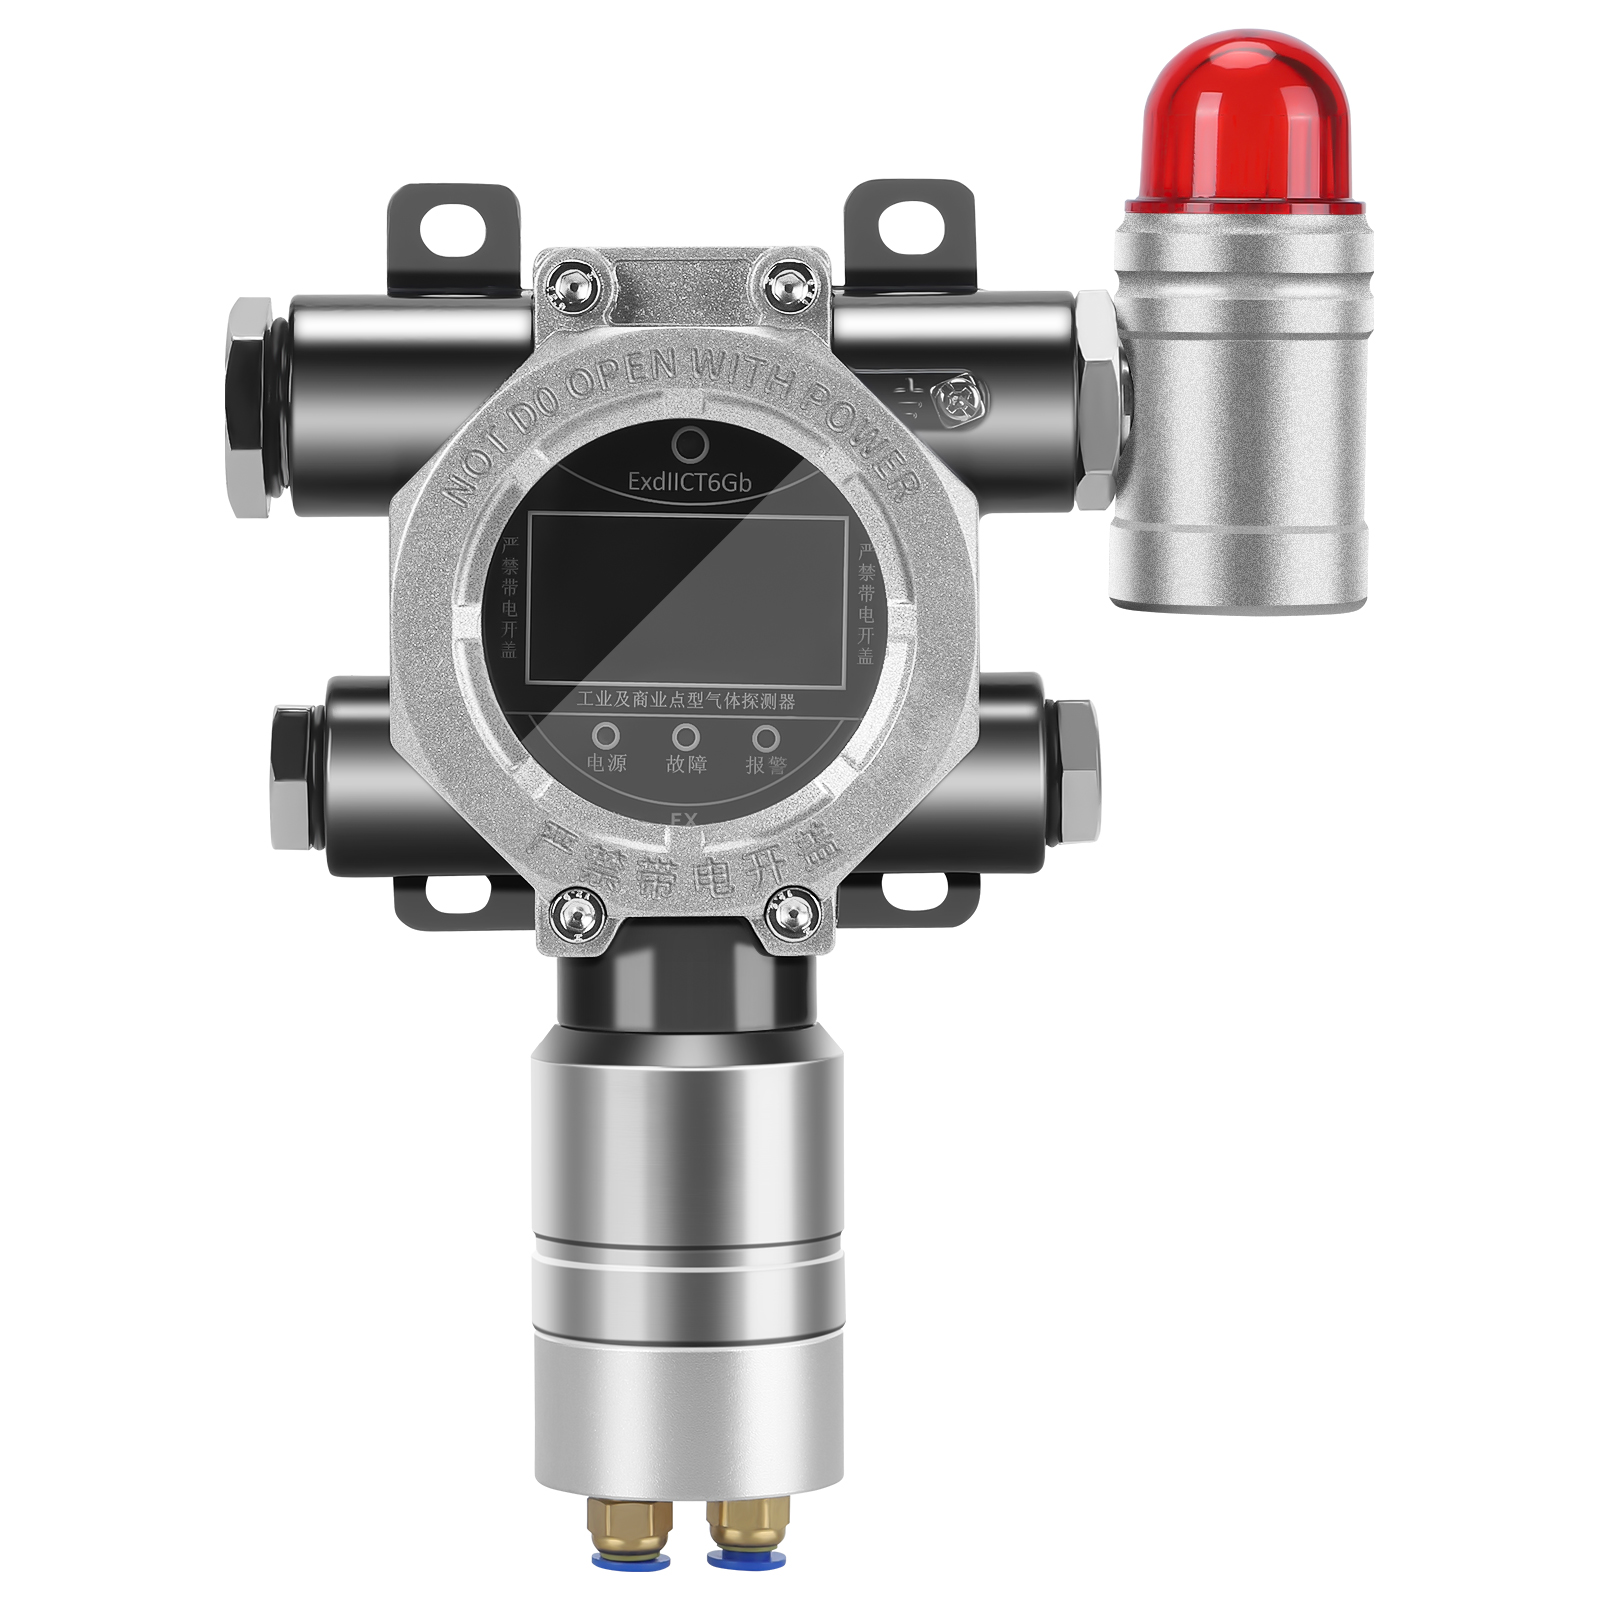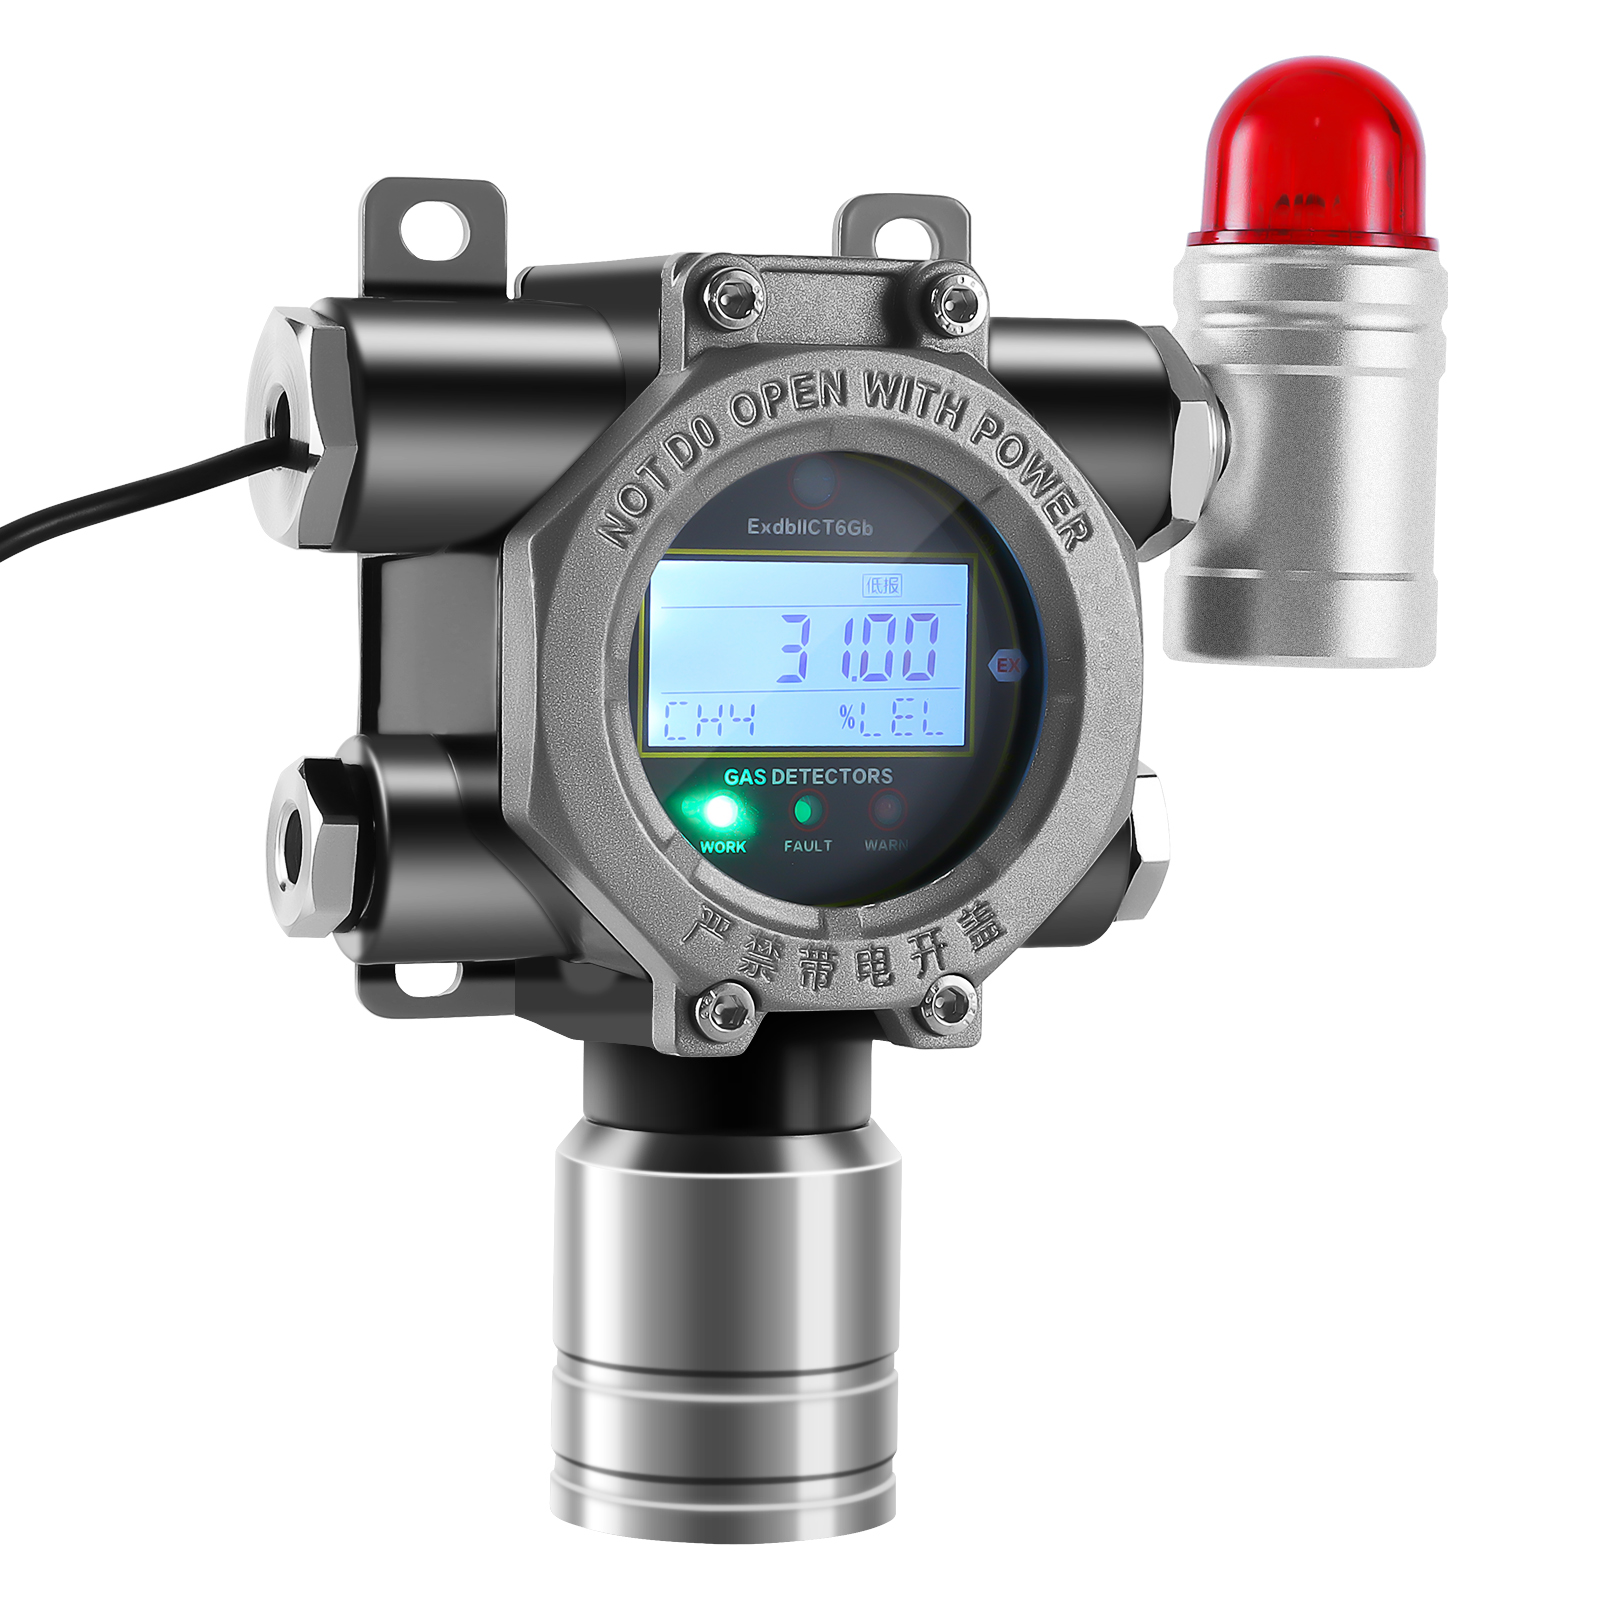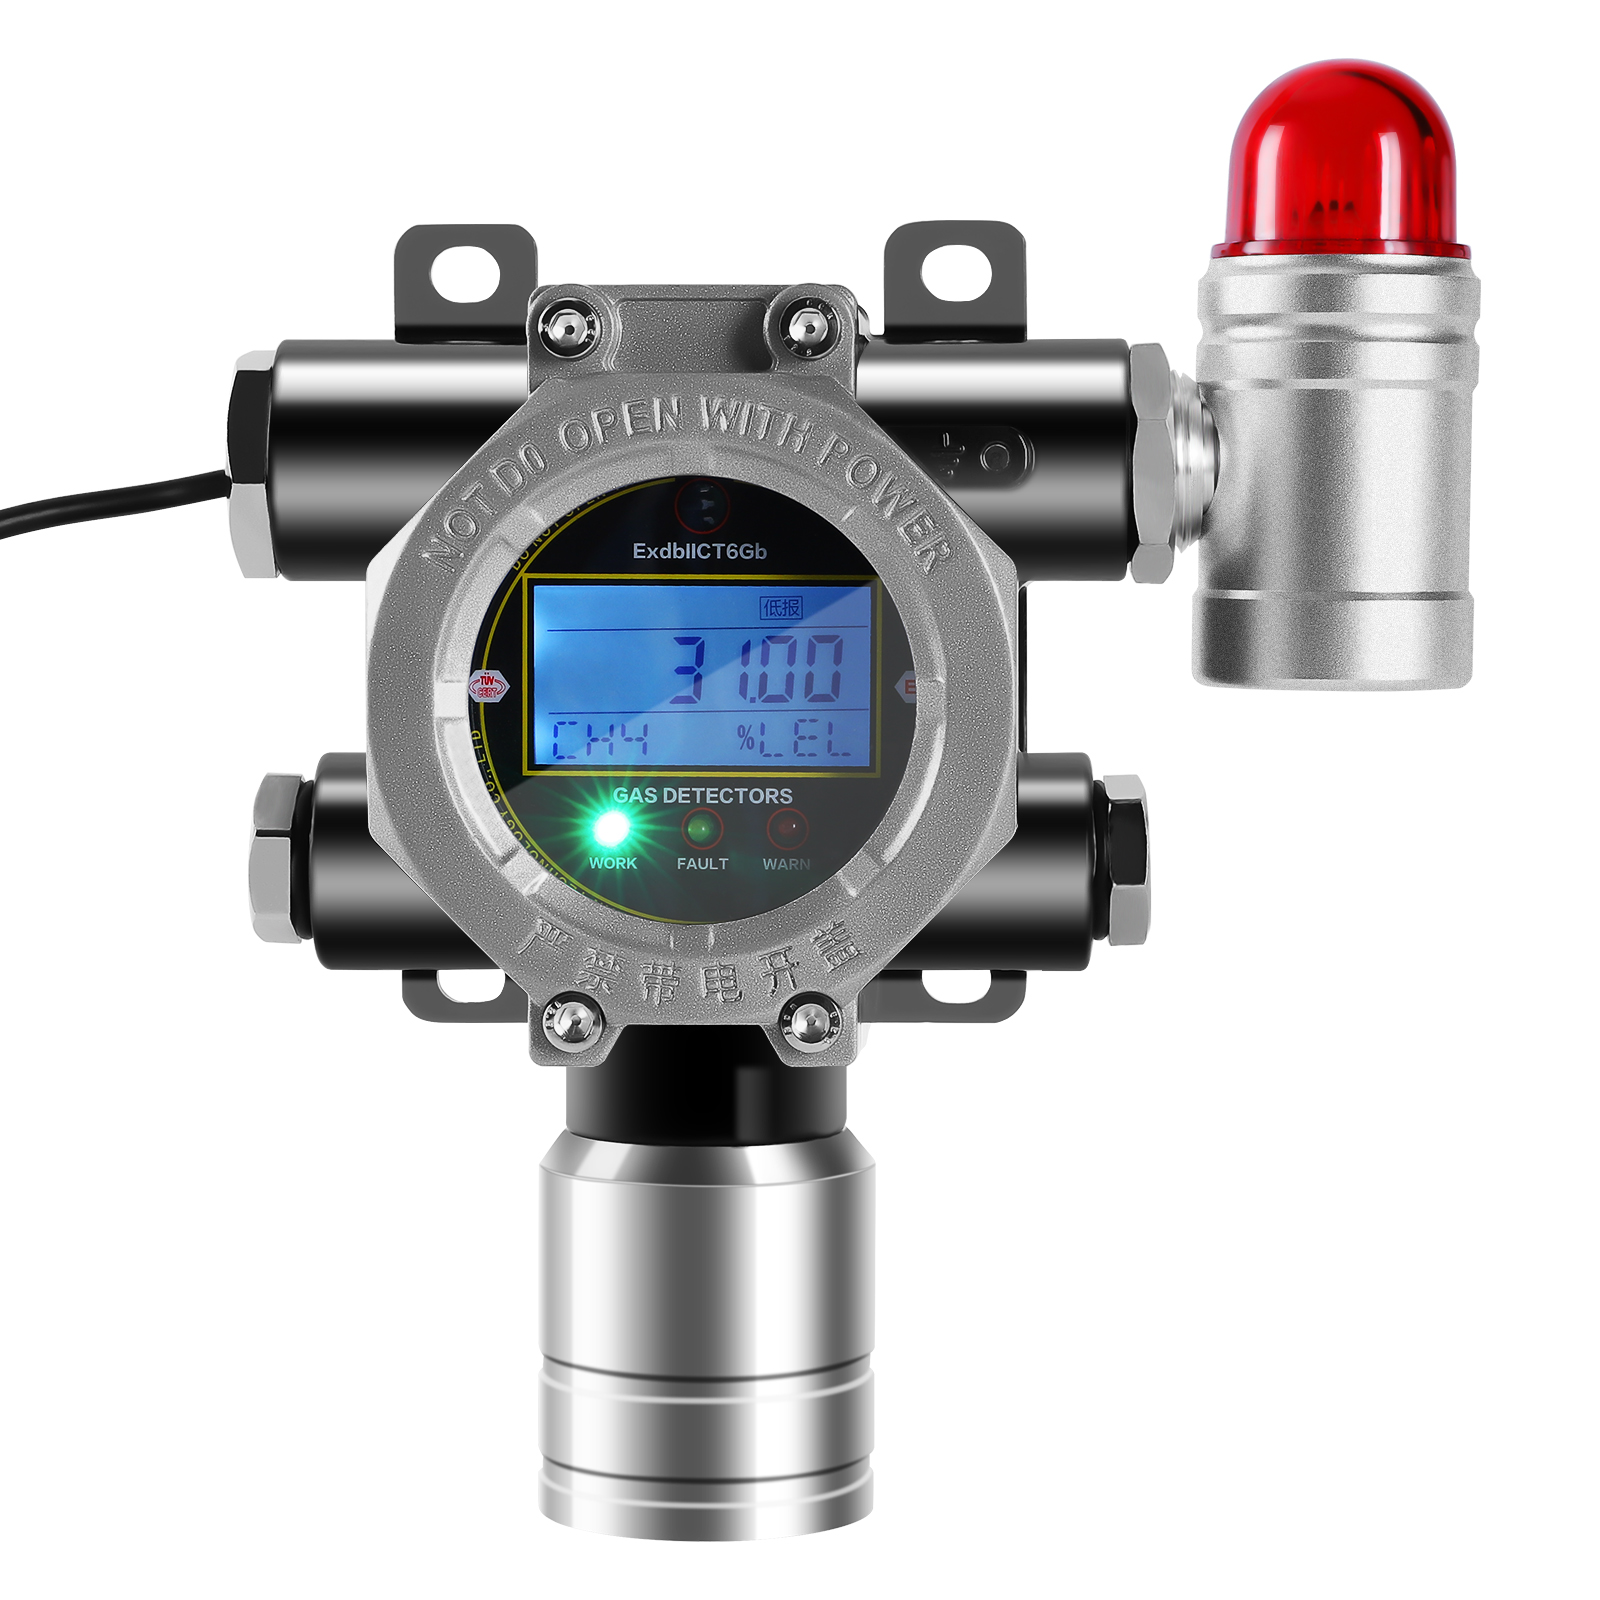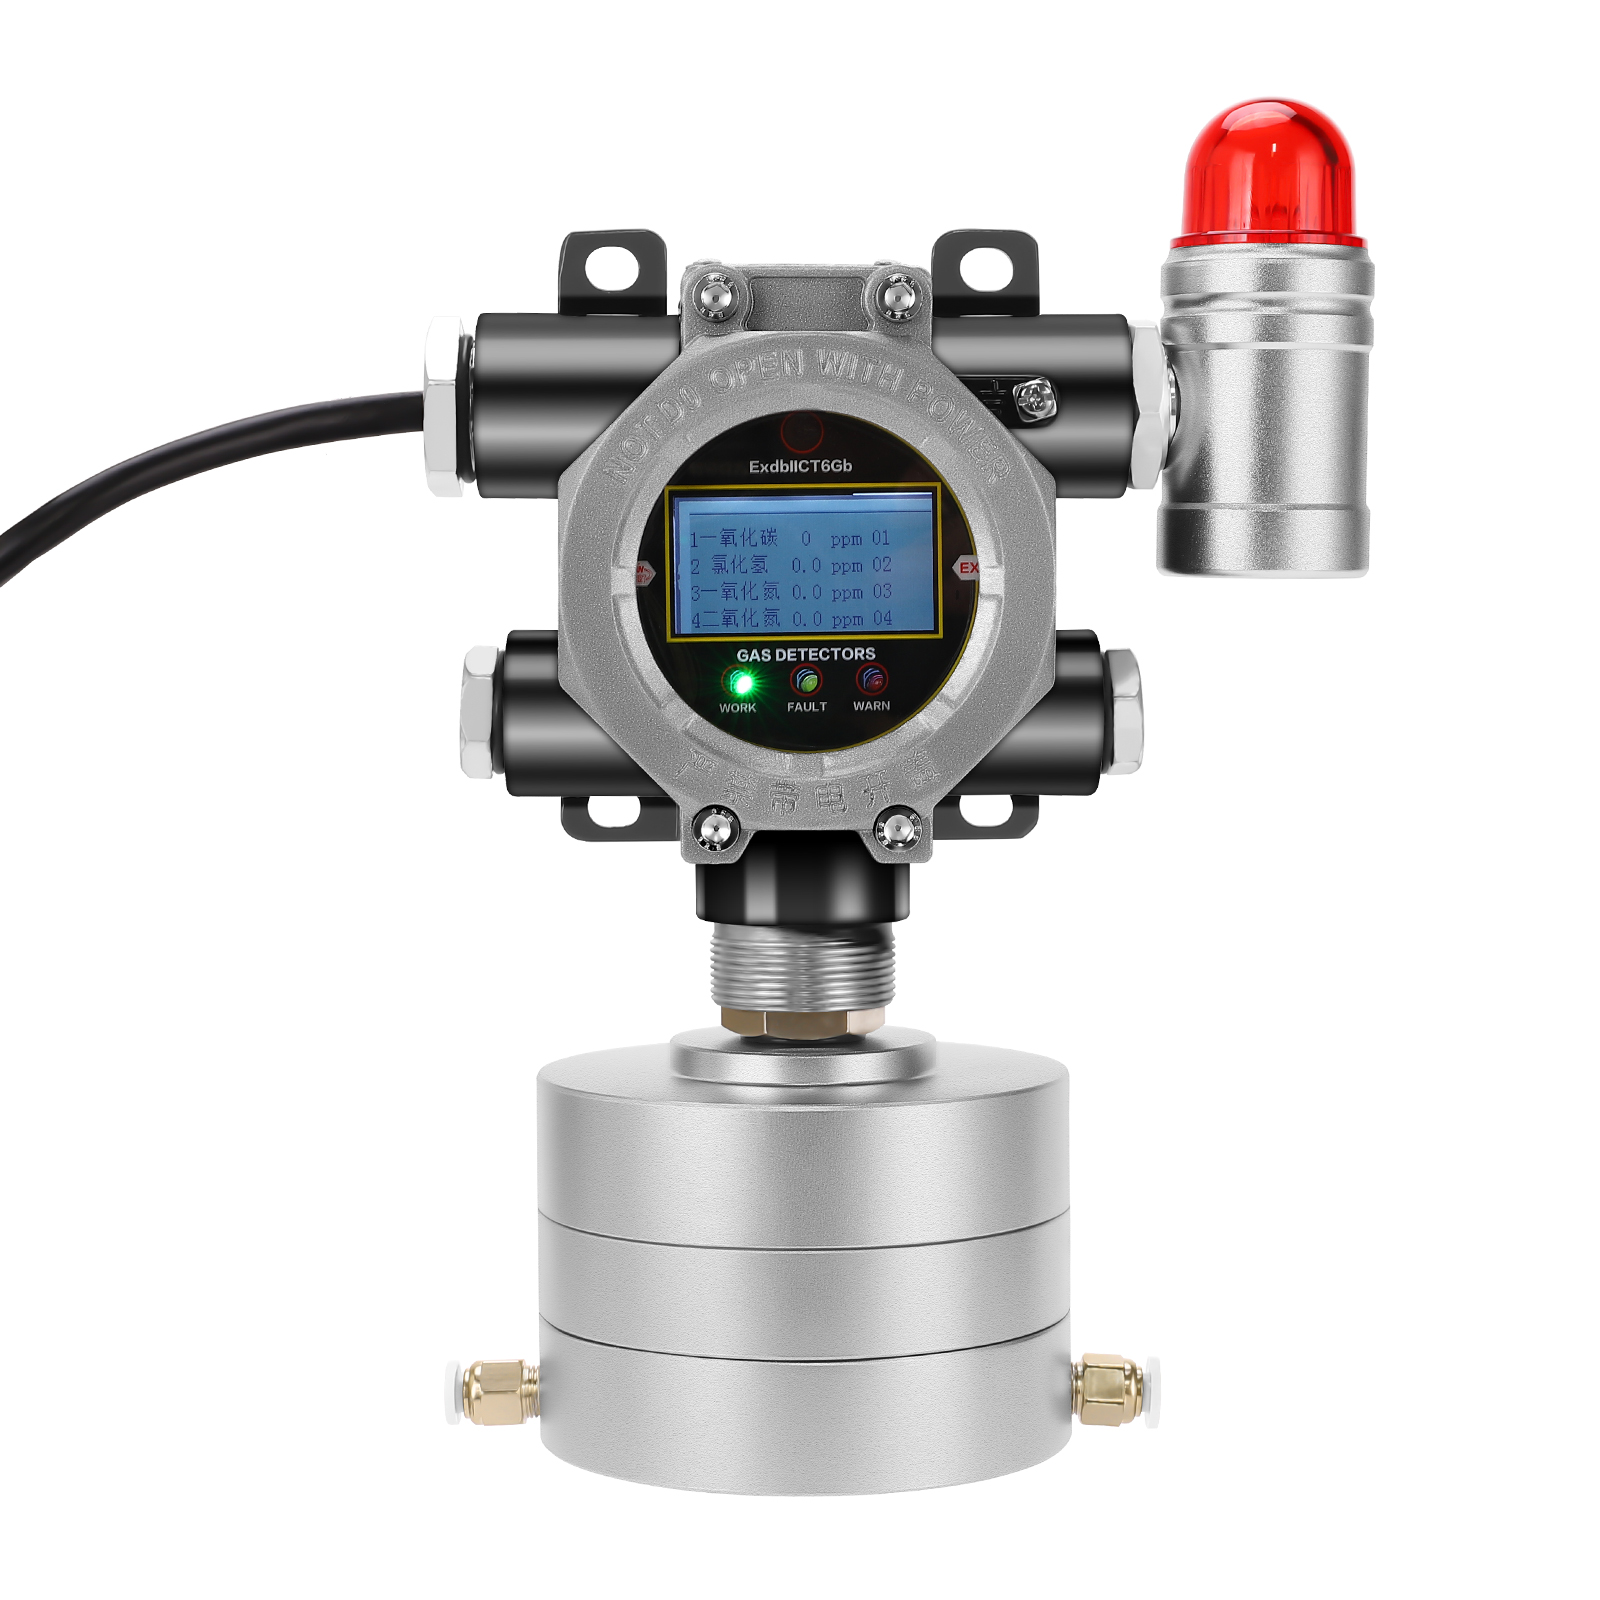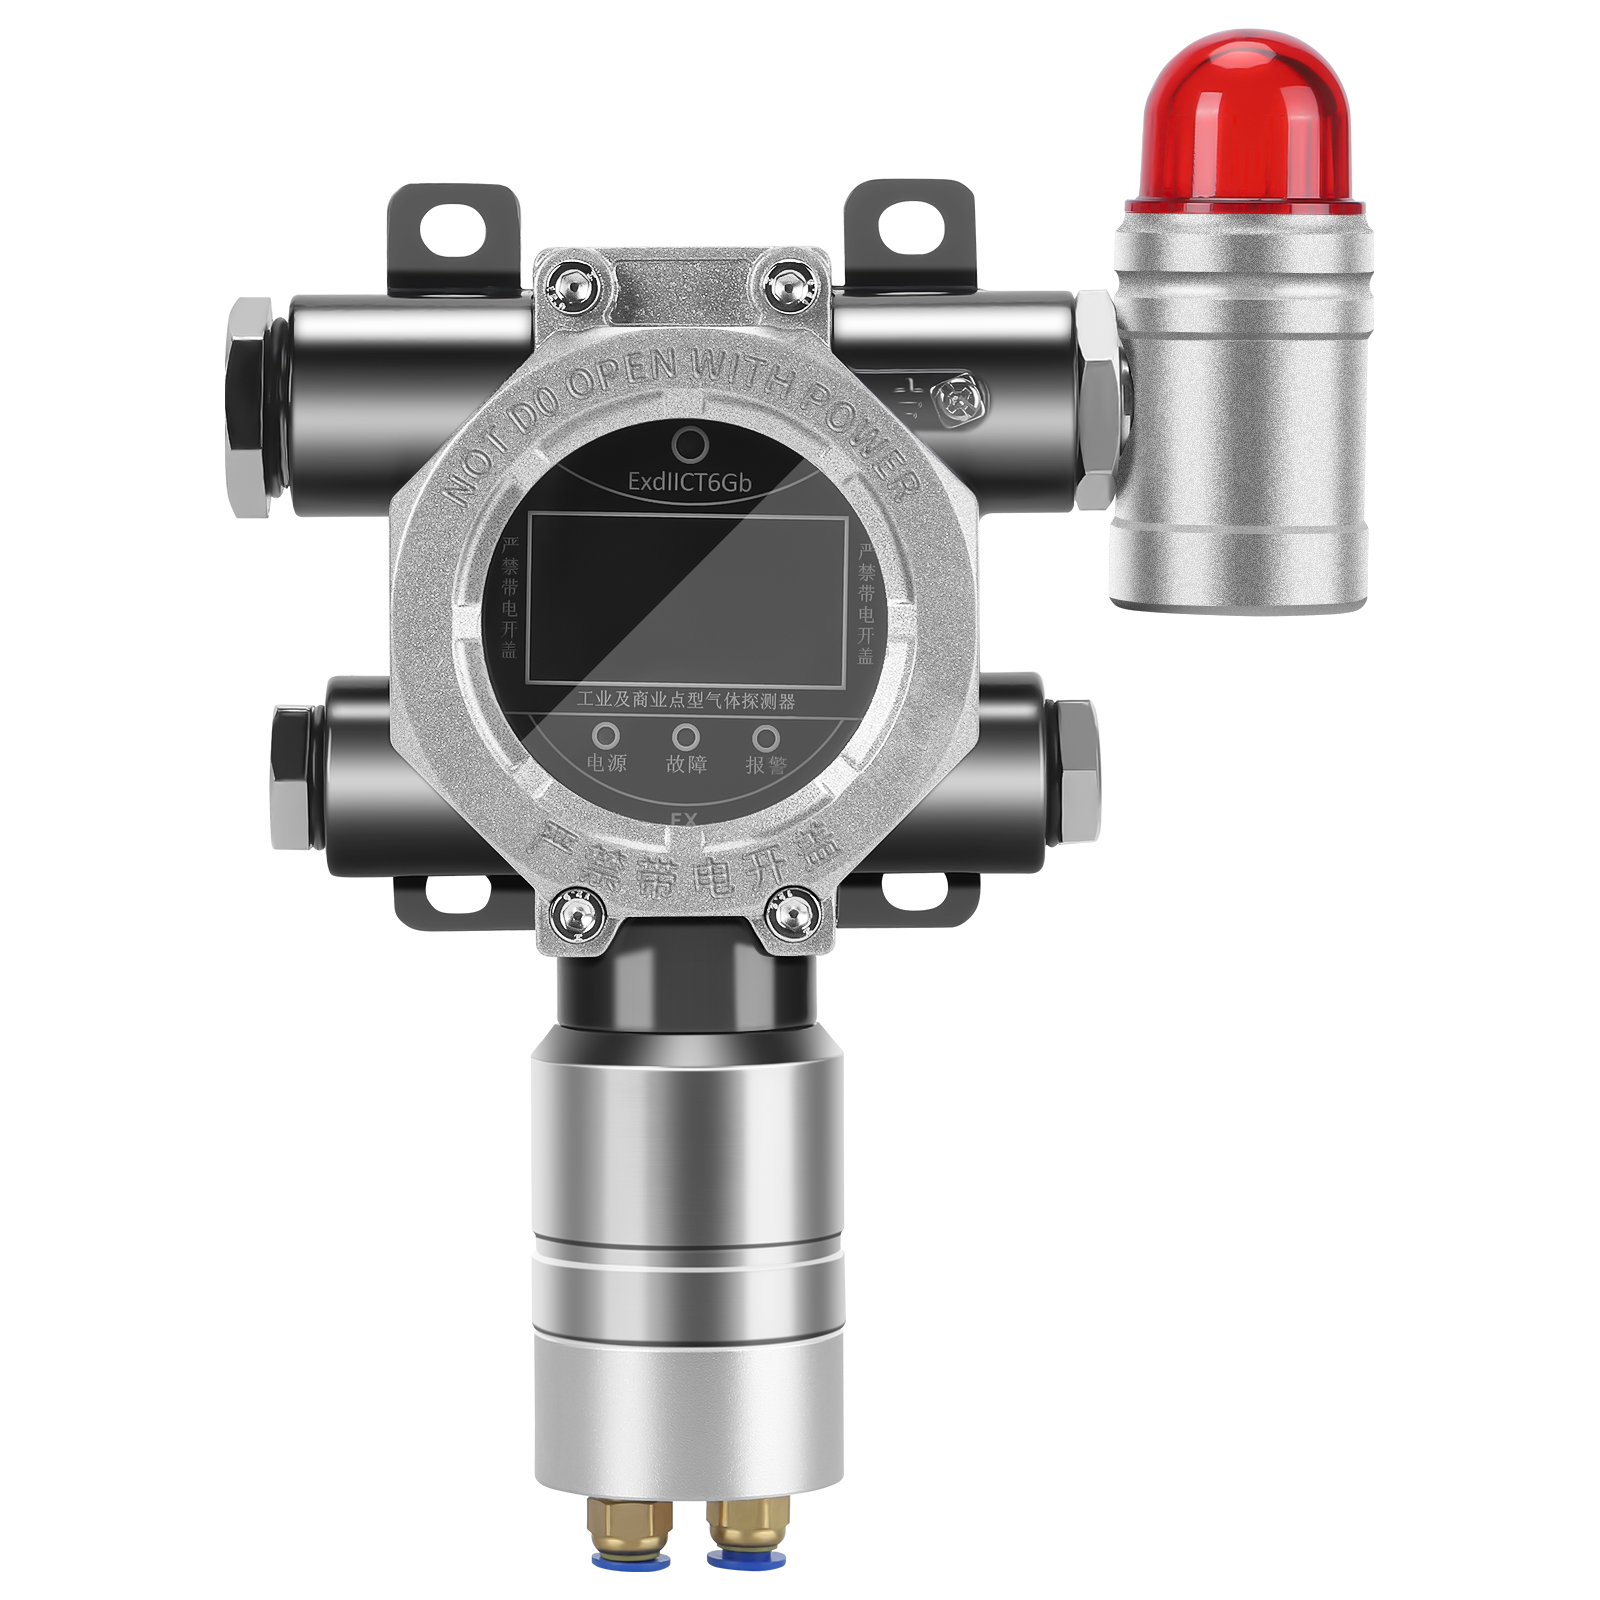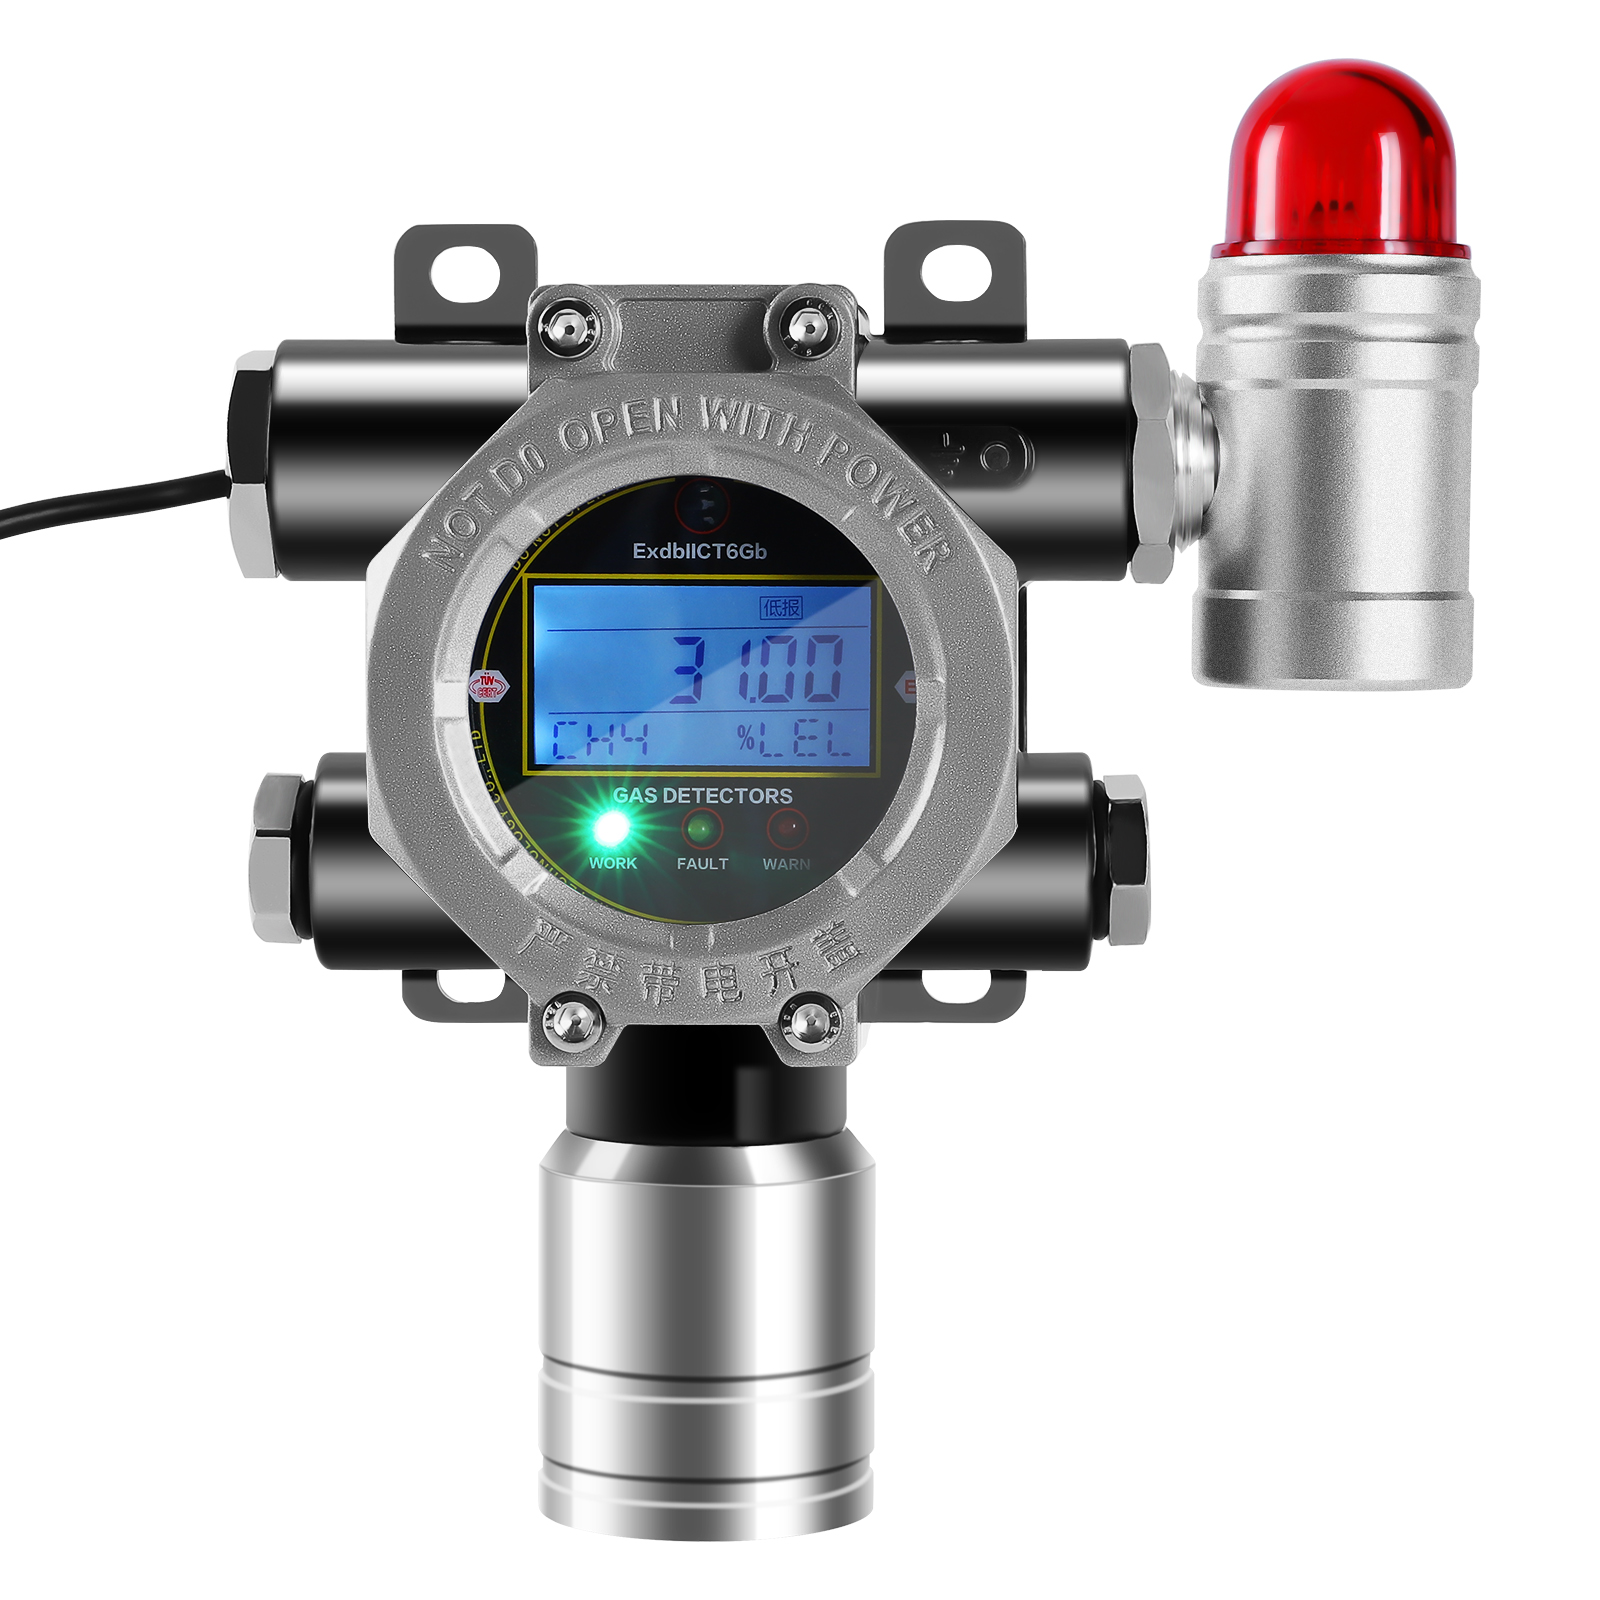
Freon piston unit alarm for fixed safety monitoring of industrial piston refrigeration units - SKA/FLA-BJQ
• Detected gas: Freon (refrigerant, R22/R134a/R410A optional)
• Measuring range: 0~1000ppm
• Resolution: 1ppm
• Alarm point: 500ppm (customizable)
• Accuracy: ±3%FS
• Response time: T90 ≤30s
• Zero drift: ≤±2%FS/year
Product Introduction
Freon piston unit alarm for fixed safety monitoring of industrial piston refrigeration units - Product Overview
The Freon piston unit alarm is an online gas detection device used for fixed safety monitoring of industrial piston refrigeration units. Search keywords: Freon piston unit alarm, fixed safety monitoring of industrial piston refrigeration units, Freon alarm. The alarm is fixedly installed in the piston unit area and can continuously detect Freon concentration. When the concentration exceeds the set threshold, it emits sound and light alarms, and optional relay output can be used to link exhaust ventilation or shut off refrigeration equipment. In fixed safety monitoring of industrial piston refrigeration units, the Freon piston unit alarm can reflect on-site gas risks in real time and help staff respond promptly.
Freon piston unit alarm for fixed safety monitoring of industrial piston refrigeration units - Working Principle
Freon piston unit alarms usually use semiconductor sensors or infrared sensors to output electrical signals by detecting Freon concentration and calculate gas concentration. In fixed safety monitoring of industrial piston refrigeration units, the Freon piston unit alarm converts detection signals into 4-20mA, RS485, or Modbus output, which can be connected to PLC, DCS, and gas alarm control systems. The alarm is fixedly installed near the piston unit or on the wall, has moisture-proof and explosion-proof functions, and its protection rating can reach IP65 or IP66.
Freon piston unit alarm for fixed safety monitoring of industrial piston refrigeration units - Application Scenarios
Freon piston unit alarms are widely used in the piston compressor, oil separator, condenser, and pipeline valve areas of industrial piston refrigeration units. In fixed safety monitoring of industrial piston refrigeration units, Freon piston unit alarms can be fixedly installed near piston units, pipeline valves, and personnel inspection passages. The alarm can be linked with exhaust fans, shut-off valves, and fire protection systems to achieve automatic handling. For large piston units, Freon piston unit alarms can also form a multi-point monitoring network and upload data uniformly to the control room.
Freon piston unit alarm for fixed safety monitoring of industrial piston refrigeration units - Technical Advantages
The Freon piston unit alarm has advantages such as fast response, good stability, and strong anti-interference ability. In fixed safety monitoring of industrial piston refrigeration units, the Freon piston unit alarm uses industrial-grade sensors and explosion-proof housings, making it suitable for long-term operation. The alarm supports sound and light alarms, remote output, and fault self-diagnosis, and is easy to maintain. When selecting a Freon piston unit alarm, attention should be paid to detection range, accuracy, response time, explosion-proof rating, and output signal to ensure it meets the needs of fixed safety monitoring of industrial piston refrigeration units.