Product Introduction
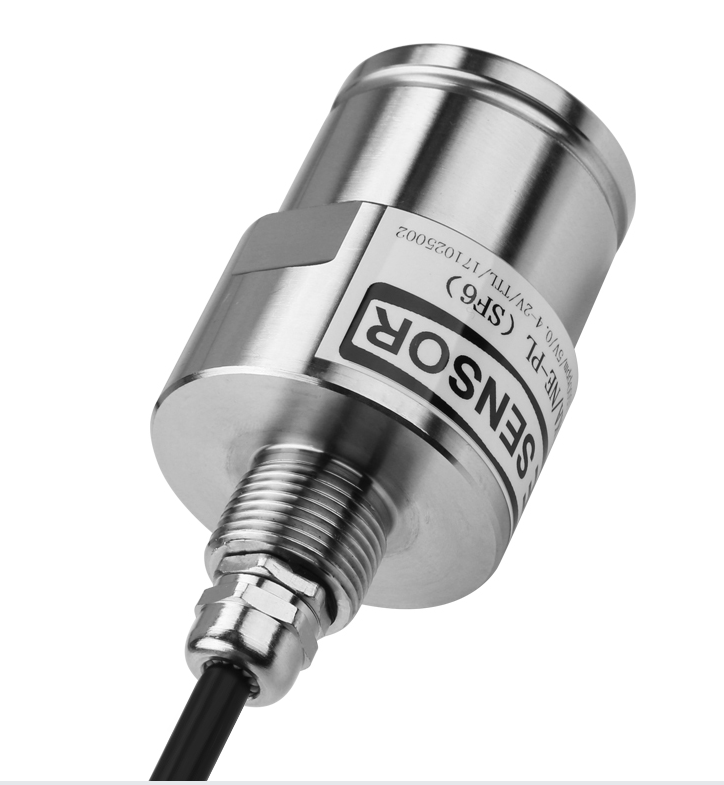
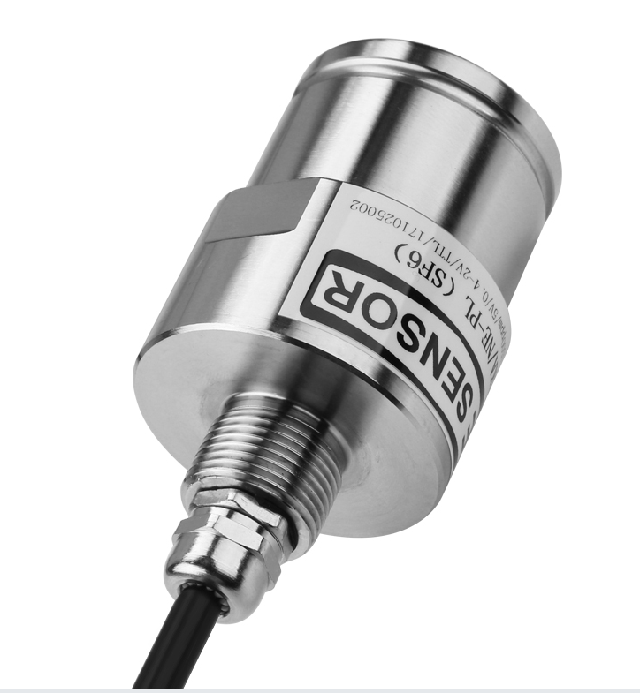
This gas cup-type gas probe is a compact, portable, and high-precision detection instrument developed by Shengkaian using years of experience, specifically for fields with a high risk of gas leakage such as chemical plants, boiler rooms, environmental monitoring, scientific research and security, tunnel construction, and waste treatment plants.
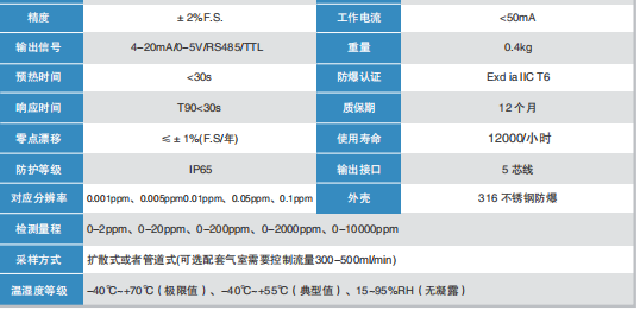
This probe is compatible with sensors based on various principles such as infrared, electrochemical, catalytic, semiconductor, and photoionization. It adopts intrinsically safe technology, comes with temperature compensation, and is precisely calibrated at the factory. Users only need to insert the sensor module into the probe, and the module will automatically upload signals to the control board in real time, with no need for secondary calibration during use. Explosion-proof standard design avoids the risk of installing sensor modules in hazardous locations with power supply. Industrial-grade standard4-20mAAnalog output,Modbus485Standard protocol, providing functions such as remote debugging, troubleshooting, and calibration signals.
II. Technical Advantages
- Intrinsically safe design, certified to explosion-proof standards, safe and reliable performance;
316Stainless steel housing, good corrosion resistance, suitable for various harsh working conditions
- Comes with zero fine-tuning and target point locking functions; when replacing different gas sensors, there is no need to change the existing housing and wiring, just replace the sensor module board;
- The detection unit features automatic diagnosis and problem identification functions, so users need not worry about the instrument's working status;
- Self-calibration can be combined withPLCDirect connection to controller;
- Can be connected to a computer for communication;
- Analog Voltage/Current and serial port output simultaneously, convenient for user operation and maintenance;
- Industrial-gradeEMCModule, capable of calmly coping with interference from electrical and other factors;
- Original imported sensor, optimized with secondary algorithms, fast response speed, low error rate;
- Low power consumption, can be powered by lithium battery;
- Complete range of gas detection types, professional guidance services available.
Main Application Areas
- Chemical Plants — Continuous ethanol vapor monitoring in production, storage and handling areas to prevent leaks and ensure worker safety.
- Boiler Rooms — Detection of flammable ethanol gas accumulation in boiler rooms and fuel supply systems to reduce explosion risk.
- Environmental Monitoring — Ambient ethanol concentration measurement for environmental compliance and emission control at industrial sites.
- Tunnel Construction — Real-time gas leak detection in confined tunnel workspaces where ethanol vapors may accumulate.
- Waste Treatment Facilities — Monitoring ethanol gas release in waste processing and landfill areas to protect personnel and equipment.
Keywords:ethanol gas probe, C2H6O gas detector, gas cup probe, ethanol sensor, explosion-proof gas probe, industrial gas detector, ethanol leak detector, gas detection instrument