Product Introduction
Industrial Online Near-Infrared Moisture Monitoring Device 4-20mA/RS485 Output Moisture Content Analyzer
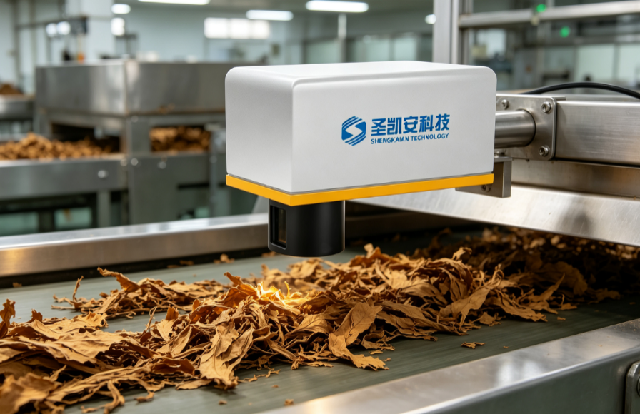
Industrial Online Near-Infrared Moisture Monitoring Device 4-20mA/RS485 Output Moisture Content Analyzeris based onNear-infrared Spectroscopy Analysis PrincipleDeveloped industrial-grade non-contact real-time moisture detection equipment, specially designed for automated production lines. The core principle of the equipment is that water molecules have specific absorption characteristics for near-infrared light in specific bands. During operation, the optical probe continuously emits a stable light source, irradiating the surface of dynamic materials on the production line, collecting the reflected spectral signals in real time, and quickly completing signal analysis and data calculation through a built-in high-precision intelligent algorithm, outputting accurate moisture content values in milliseconds. The entire process requires no manual sampling, no material contact, no drying waiting, and can achieve24-hour continuous monitoring, completely abandoning the lag of traditional detection methods, fully adapting to the needs of industrialized continuous production.
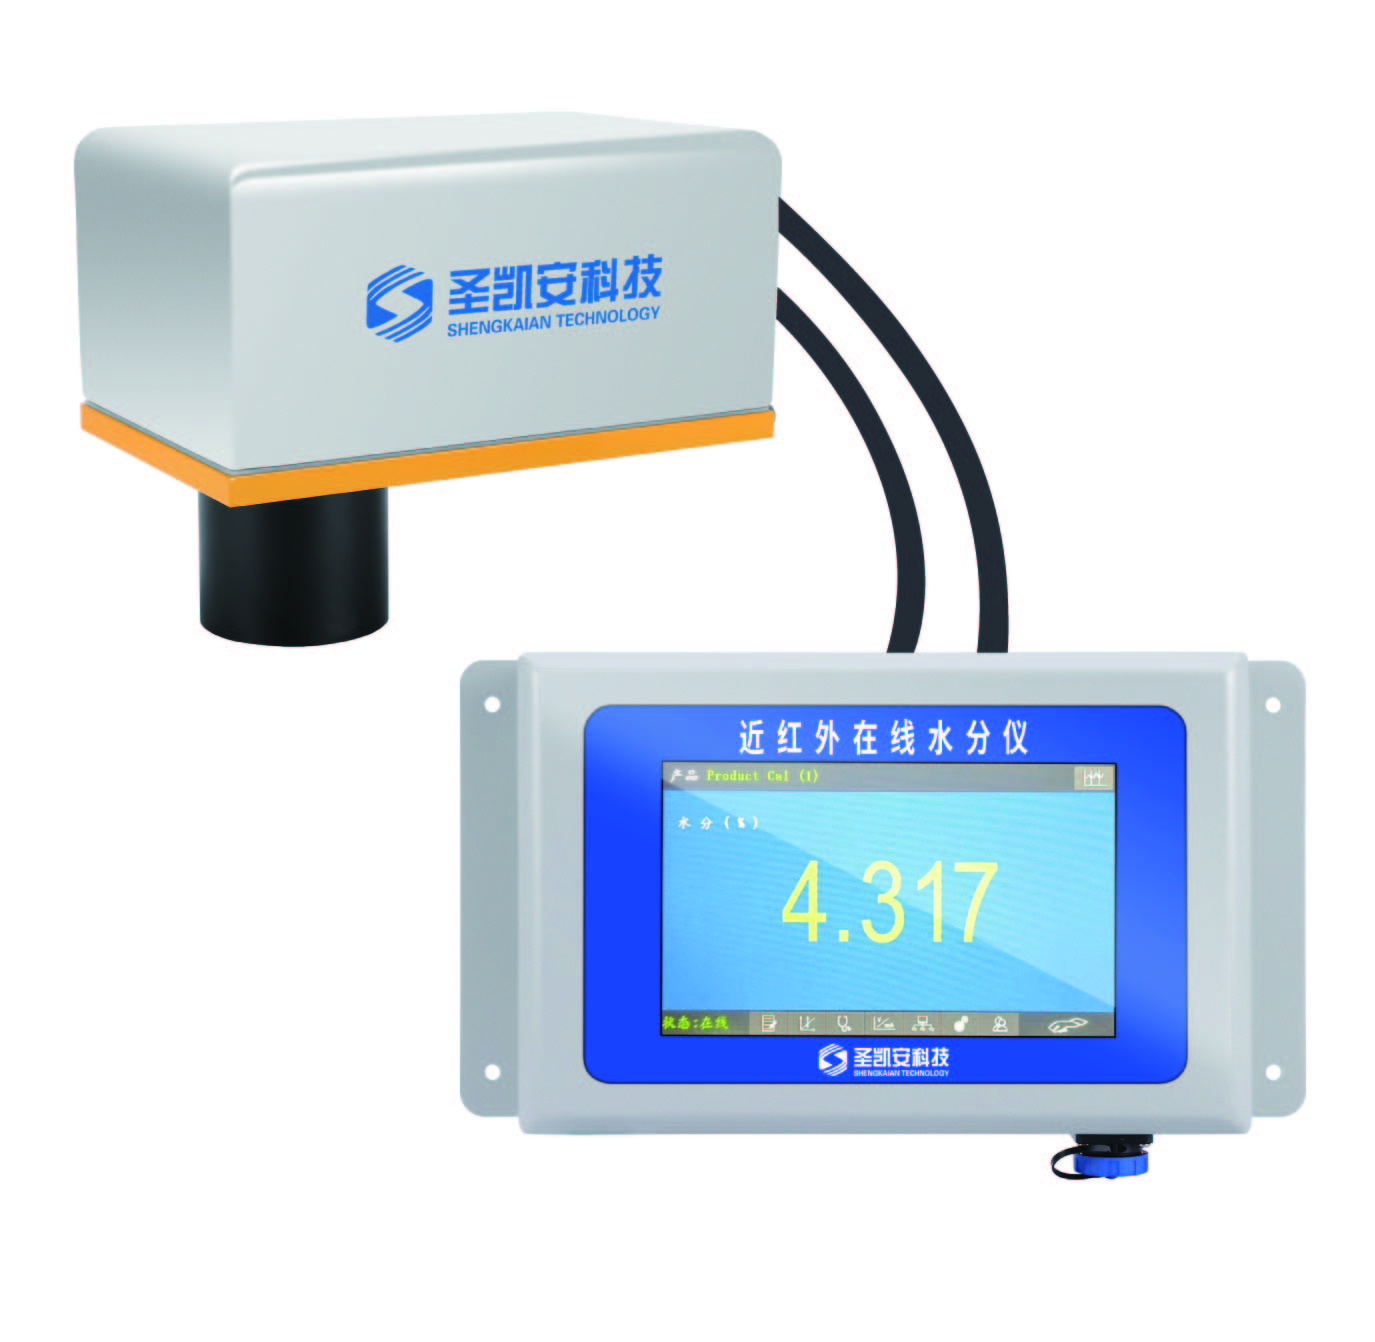
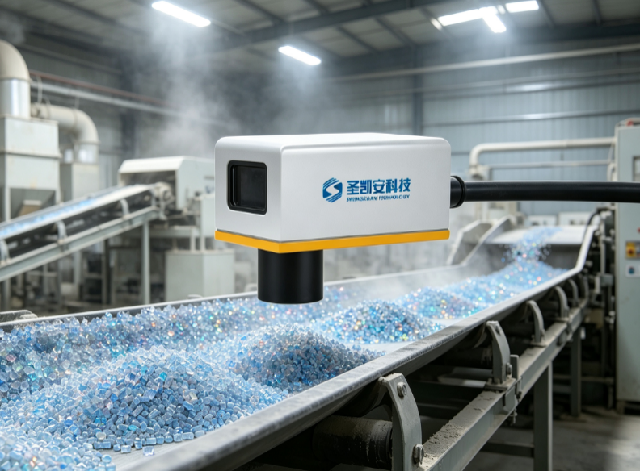
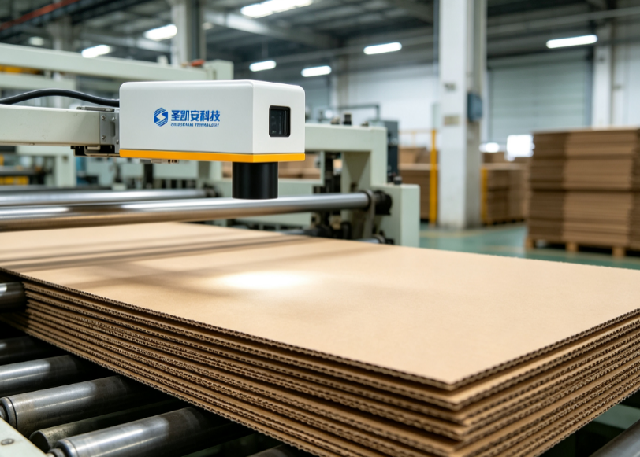
Industrial Online Near-Infrared Moisture Monitoring Device 4-20mA/RS485 Output Moisture Content Analyzer. The equipment adopts a mature split modular structure, consisting of a high-precision detection probe and an intelligent main control transmitter. The structure is simple, installation is flexible, and it can adapt to various on-site conditions such as belt conveyor lines, material chutes, storage silos, and discharge ports. Installation and commissioning are convenient, without the need to modify existing production equipment. The whole machine is equipped with a self-developed intelligent anti-interference compensation algorithm, which can automatically offset external interference factors such as on-site dust, ambient light fluctuations, material color differences, and uneven material thickness, effectively avoiding detection errors and ensuring long-term accurate measurement, strong stability, and high repeatability. At the same time, the equipment has no consumable parts and does not require frequent calibration, greatly reducing later operation and maintenance costs and manual input, suitable for long-term continuous operation in various complex industrial production environments.
Compared with traditional manual drying testing, fixed-point sampling detection and other methods, this equipment has fast detection speed and real-time data synchronization, fundamentally solving the industry pain points of lagging traditional detection data, one-sided sampling, large errors, and inability to adjust processes in real time. The equipment comes standard with4-20mA analog and RS485 digital dual industrial signal outputs, seamlessly connecting to factory PLC, DCS, industrial host computers and other automation systems, enabling real-time upload of moisture data, full traceability of data, automatic alarm for exceeding limits, and automatic fine-tuning of process parameters, completing the closed-loop control of production moisture, and helping upgrade production lines for digitalization and intelligence.
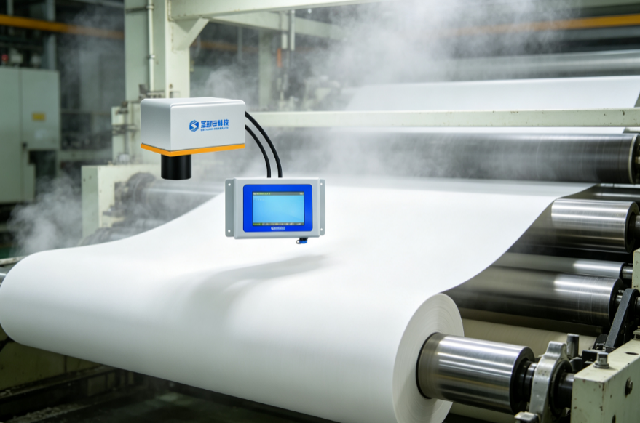
Industrial Online Near-Infrared Moisture Monitoring Device 4-20mA/RS485 Output Moisture Content Analyzer. This equipment has extremely strong versatility, suitable for various solid materials such as powders, granules, flakes, and fibers. It is widely used in industries including paper and cardboard, wood and artificial boards, grain and flour, feed and grain and oil, tobacco and tea, textile and fabric, rubber and plastic granules, chemical fertilizer and chemical industry, mining and building materials, etc. For detailed usage methods, please contact xiaojianfeng@nesensor.com. By real-time monitoring of material moisture fluctuations throughout the production process, it can precisely control production processes, effectively stabilize finished product quality, significantly reduce product defect rates, while optimizing drying, molding and other production steps, reducing material loss and energy waste, and improving overall production efficiency. With stable performance, convenient operation and maintenance, and strong adaptability, this equipment has become the core supporting detection equipment for modern industrial refined production, standardized control, and cost reduction and efficiency enhancement, helping enterprises achieve high-quality and intelligent production.。
Main Application Areas
- Food Processing — Monitor moisture content in grains, powders, and baked goods to ensure quality and consistency.
- Chemical Industry — Real-time moisture monitoring in chemical powders and granules to optimize production processes.
- Pharmaceutical Manufacturing — Ensure precise moisture levels in pharmaceutical powders and granules for product efficacy.
- Building Materials — Measure moisture in sand, cement, and other aggregates for quality control in construction.
Keywords:online moisture analyzer, NIR moisture meter, industrial moisture sensor, 4-20mA moisture transmitter, RS485 moisture analyzer, moisture content analyzer, real-time moisture monitoring, process moisture measurement