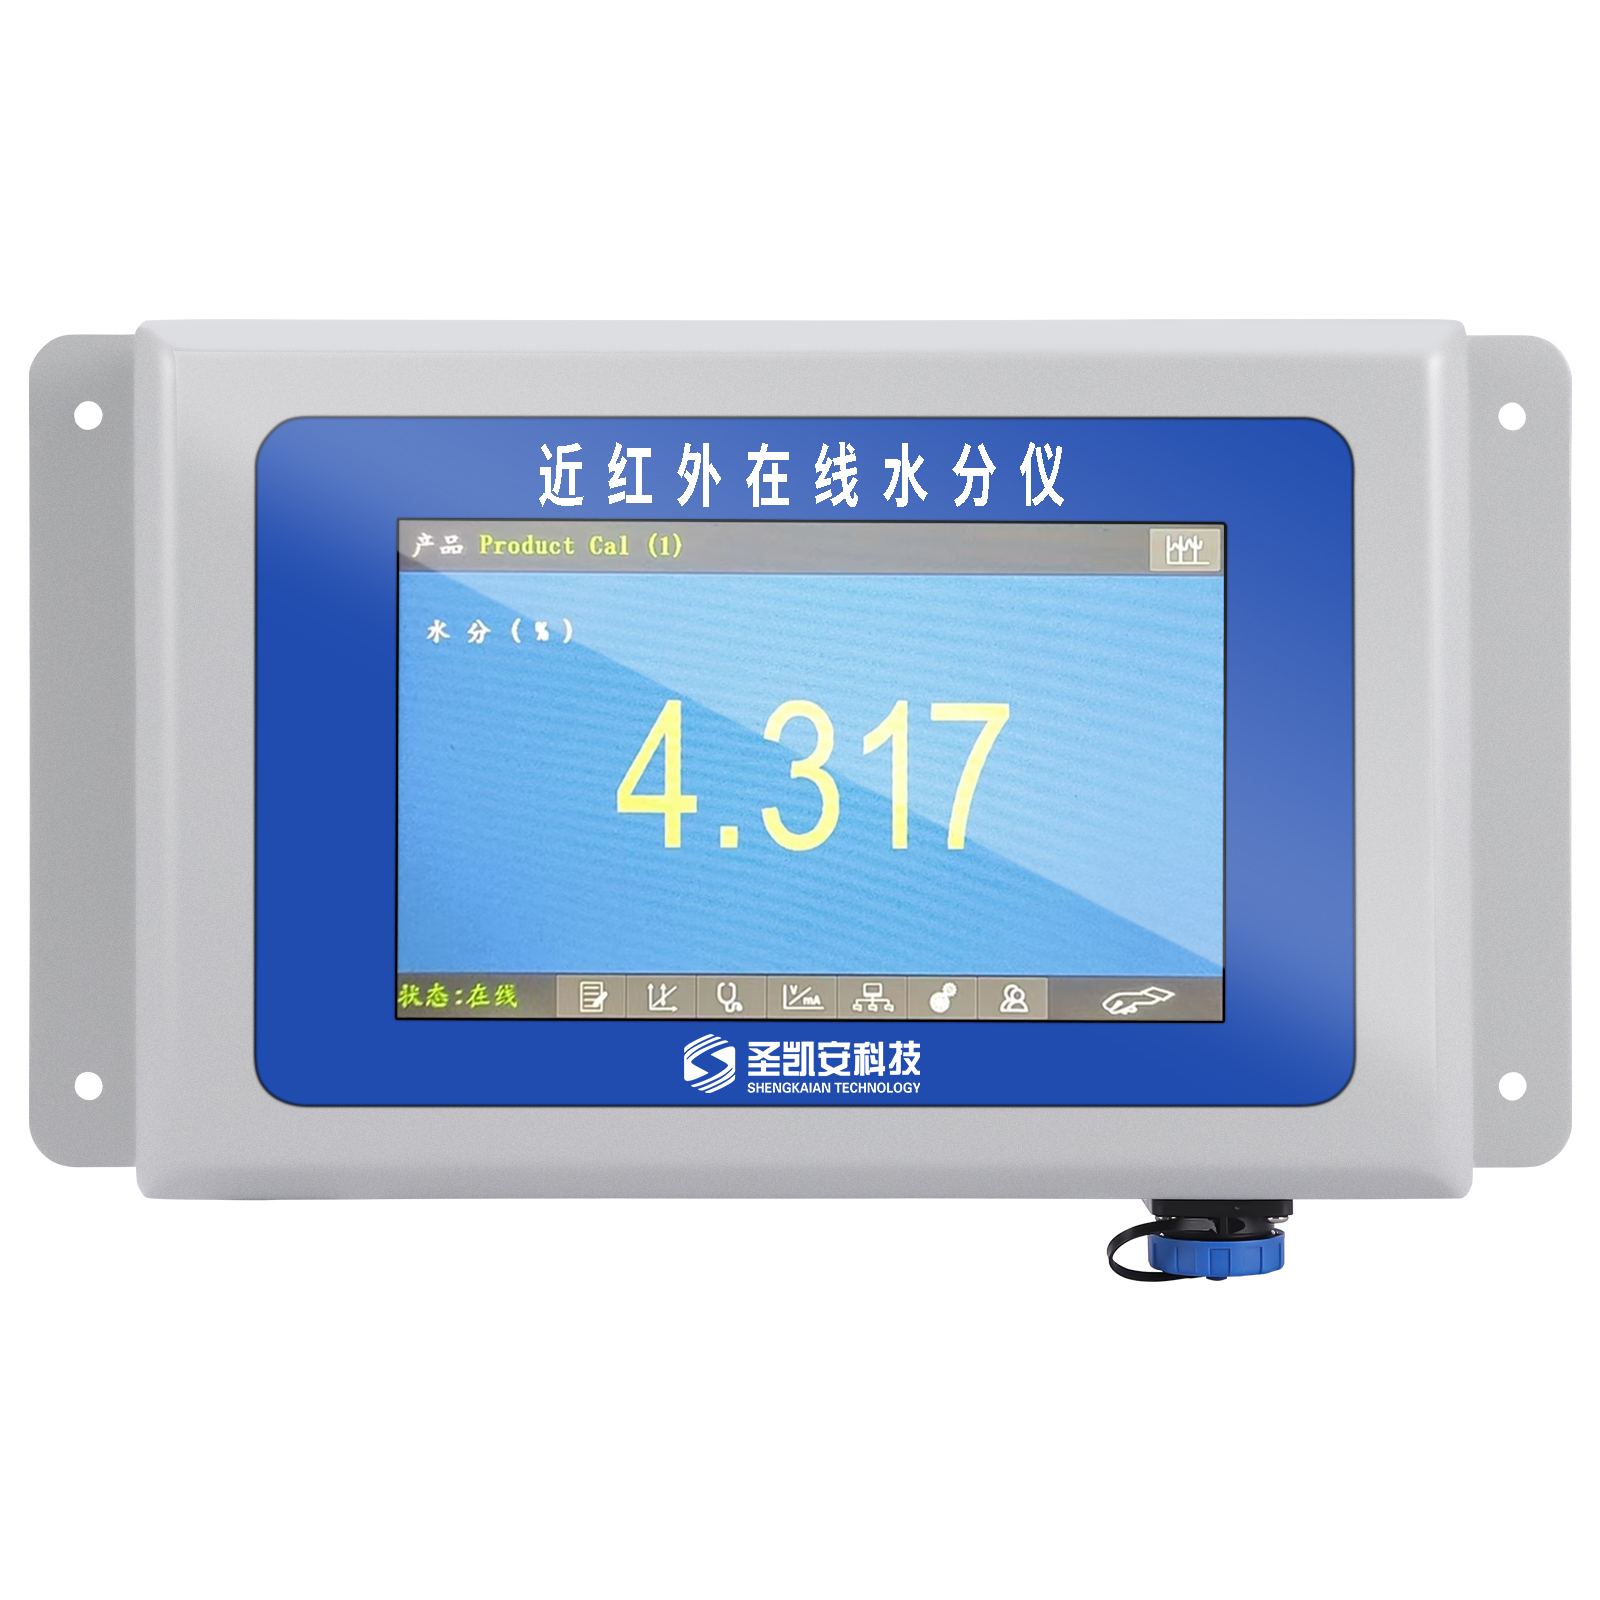
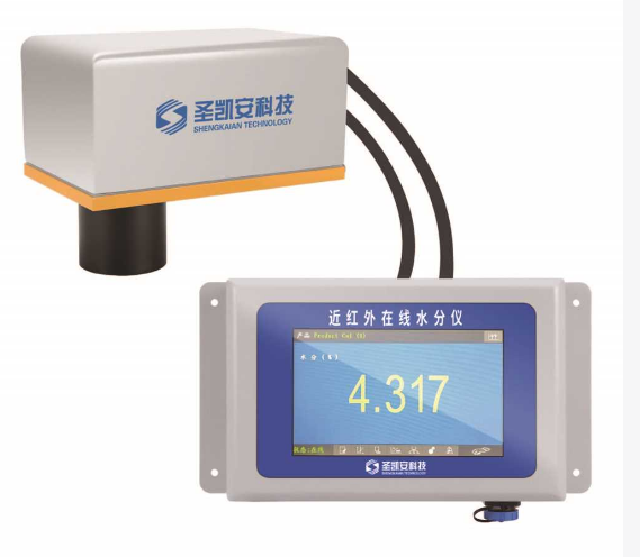
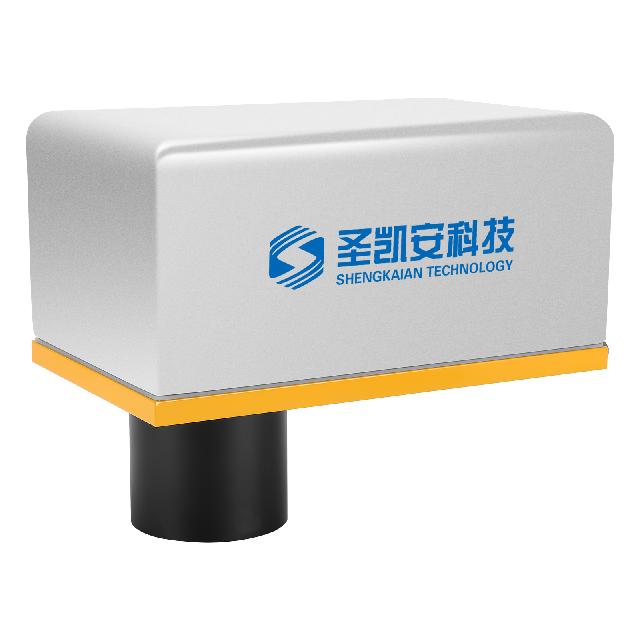
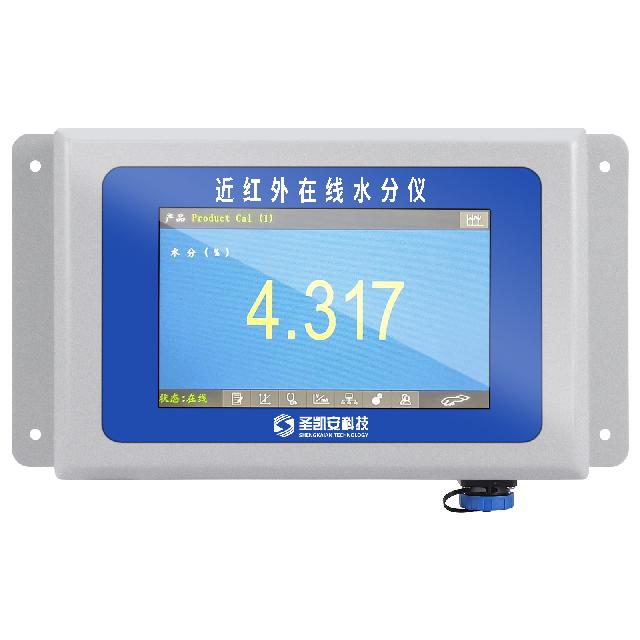
Rice and Soybean Specialized Moisture Meter Online Detection Trace Moisture Monitoring - AMT/SFY-HW
An infrared moisture meter is an instrument that uses the principle that water molecules have strong absorption characteristics for infrared light of specific wavelengths to quickly and non-contact measure the moisture content of materials
Product Introduction
Rice and Soybean Specialized Moisture Meter Online Detection Trace Moisture Monitoring
The online near-infrared moisture tester adopts the most advanced international three-wavelength six-beam near-infrared diffuse reflection principle, enabling rapid continuous measurement on the conveyor belt
for rapid continuous measurement of material moisture content, and non-contact with the measured material, achieving real-time dynamic monitoring of material moisture content, with a response time of only
5ms. Achieved rapid real-time monitoring and feedback of product moisture content, greatly meeting the strict requirements for moisture management in products. Due to the use of non-contact
Contact measurement method causes no damage to the measured material, thereby providing a precise and efficient solution for moisture control in the production process.
solution.
An infrared moisture meter is an instrument that uses the principle that water molecules have strong absorption characteristics for infrared light of specific wavelengths to quickly and non-contact measure the moisture content of materials-1-4. It is widely used in industrial production lines as a real-time quality control and process optimization tool-1-5。
Rice and Soybean Specialized Moisture Meter Online Detection Trace Moisture Monitoring
💡 Working principle
Its core is based on near-infrared spectroscopy technology: near-infrared light of specific wavelengths (such as1.94μm) when irradiating the material, it will be absorbed by water molecules, and the reflected light energy will be correspondingly weakened-2-4. The instrument calculates the moisture content of the material by analyzing the energy loss of the reflected light-1. Common three-wavelength or eight-beam technology can eliminate interference from non-moisture factors such as material color and structure, making the measurement more accurate-1-3。
✨ Core advantages
Non-contact measurement: No contact with the material, no wear or pollution, suitable for high-speed moving production lines-1-6-5。
Real-time online detection: Can provide data continuously and quickly (response time can reach millisecond level), making it convenient for immediate process adjustment-2-6-11。
No frequent maintenance needed: Compared with manual oven method or electrode method, it does not require frequent calibration, has no wearing parts, and has low use and maintenance costs-1-4。
High measurement accuracy: Typical measurement accuracy can reachBetween 0.1% and 0.5%-2-5。
Rice and Soybean Specialized Moisture Meter Online Detection Trace Moisture Monitoring
🏭 Application fields
The application range of infrared moisture meters is very wide, covering almost all industries that need to control moisture-1-3:
| Industry |
Application examples |
| Tobacco industry |
Detect the moisture of tobacco leaves, cut tobacco, and tobacco stems to ensure taste and combustibility-3-4。 |
| Grain and food |
Detect the moisture of grains, flour, biscuits, feed, and other raw materials and finished products-2-6。 |
| Wood processing |
Online detection of moisture in particleboard and density board raw materials and semi-finished products-3-4。 |
| Chemical and pharmaceutical industries |
Measure the moisture content of fertilizers, plastic pellets, chemical powders, and pharmaceutical granules-1-8。 |
| Iron and steel and metallurgy |
Measure the moisture of sintered mixtures, mineral powder, concentrate, and other raw materials, which is a key monitoring point in the sintering process-3-4。 |
| Building materials |
Detect the moisture of quartz sand, ceramic powder, gypsum board, and other materials-3-8。 |
📊 Key technical parameters
Different models of infrared moisture meters have different parameters. The following are some typical parameter ranges for your reference-2-5-11:
| Parameter items |
Typical indicators |
| Measurement Range |
0% ~ 60% or 0% ~ 95% |
| Measurement accuracy |
±0.1% ~ ±0.5% (depending on the material) |
| 分辨率 |
0.01% or 0.001% |
| Measurement distance |
Generally 150mm ~ 400mm |
| Response time |
Up to0.0125 seconds to 1 second |
| Communication interface |
RS485 (Modbus), 4-20mA, RS232, Ethernet, etc. |
| 防护等级 |
Industrial grade usuallyIP65 to IP67 |
🔍 How to choose
Clarify requirements: First, determine whether it is used forOnline production lineOrLaboratory spot check. Online type needs a sturdy shell and real-time communication capability, while laboratory benchtop type focuses more on high precision and sample adaptability-9-10。
Evaluate materials: Different materials (such as dark powders, lump ores, transparent films) have different reflection characteristics for infrared light, and it is necessary to confirm whether the equipment can effectively measure your material-1-8。
Consider the environment: If the installation environment has high dust, high humidity, or high temperature, choose a model with good sealing and cooling protection functions-5-8。
What kind of material do you mainly want to detect? Is it for real-time monitoring on the production line or laboratory testing? Tell me the specific application scenario, and I can help you analyze a more suitable selection plan.
Main Application Areas
- Agricultural Processing — Ideal for measuring moisture in rice, soybeans, wheat, and other grains during drying, storage, and processing to ensure optimal quality and prevent spoilage.
- Food Production — Used in the production of snacks, cereals, and baked goods to monitor and control moisture levels, ensuring consistent texture and shelf life.
- Chemical Industry — Applied in the manufacturing of powders, granules, and pellets to monitor moisture content, which is critical for product quality and process efficiency.
- Pharmaceutical Manufacturing — Ensures precise moisture control in the production of tablets, capsules, and powders, meeting strict regulatory standards.
Keywords:online moisture meter, near-infrared moisture analyzer, trace moisture monitoring, rice moisture meter, soybean moisture meter, industrial moisture sensor, real-time moisture measurement, non-contact moisture meter