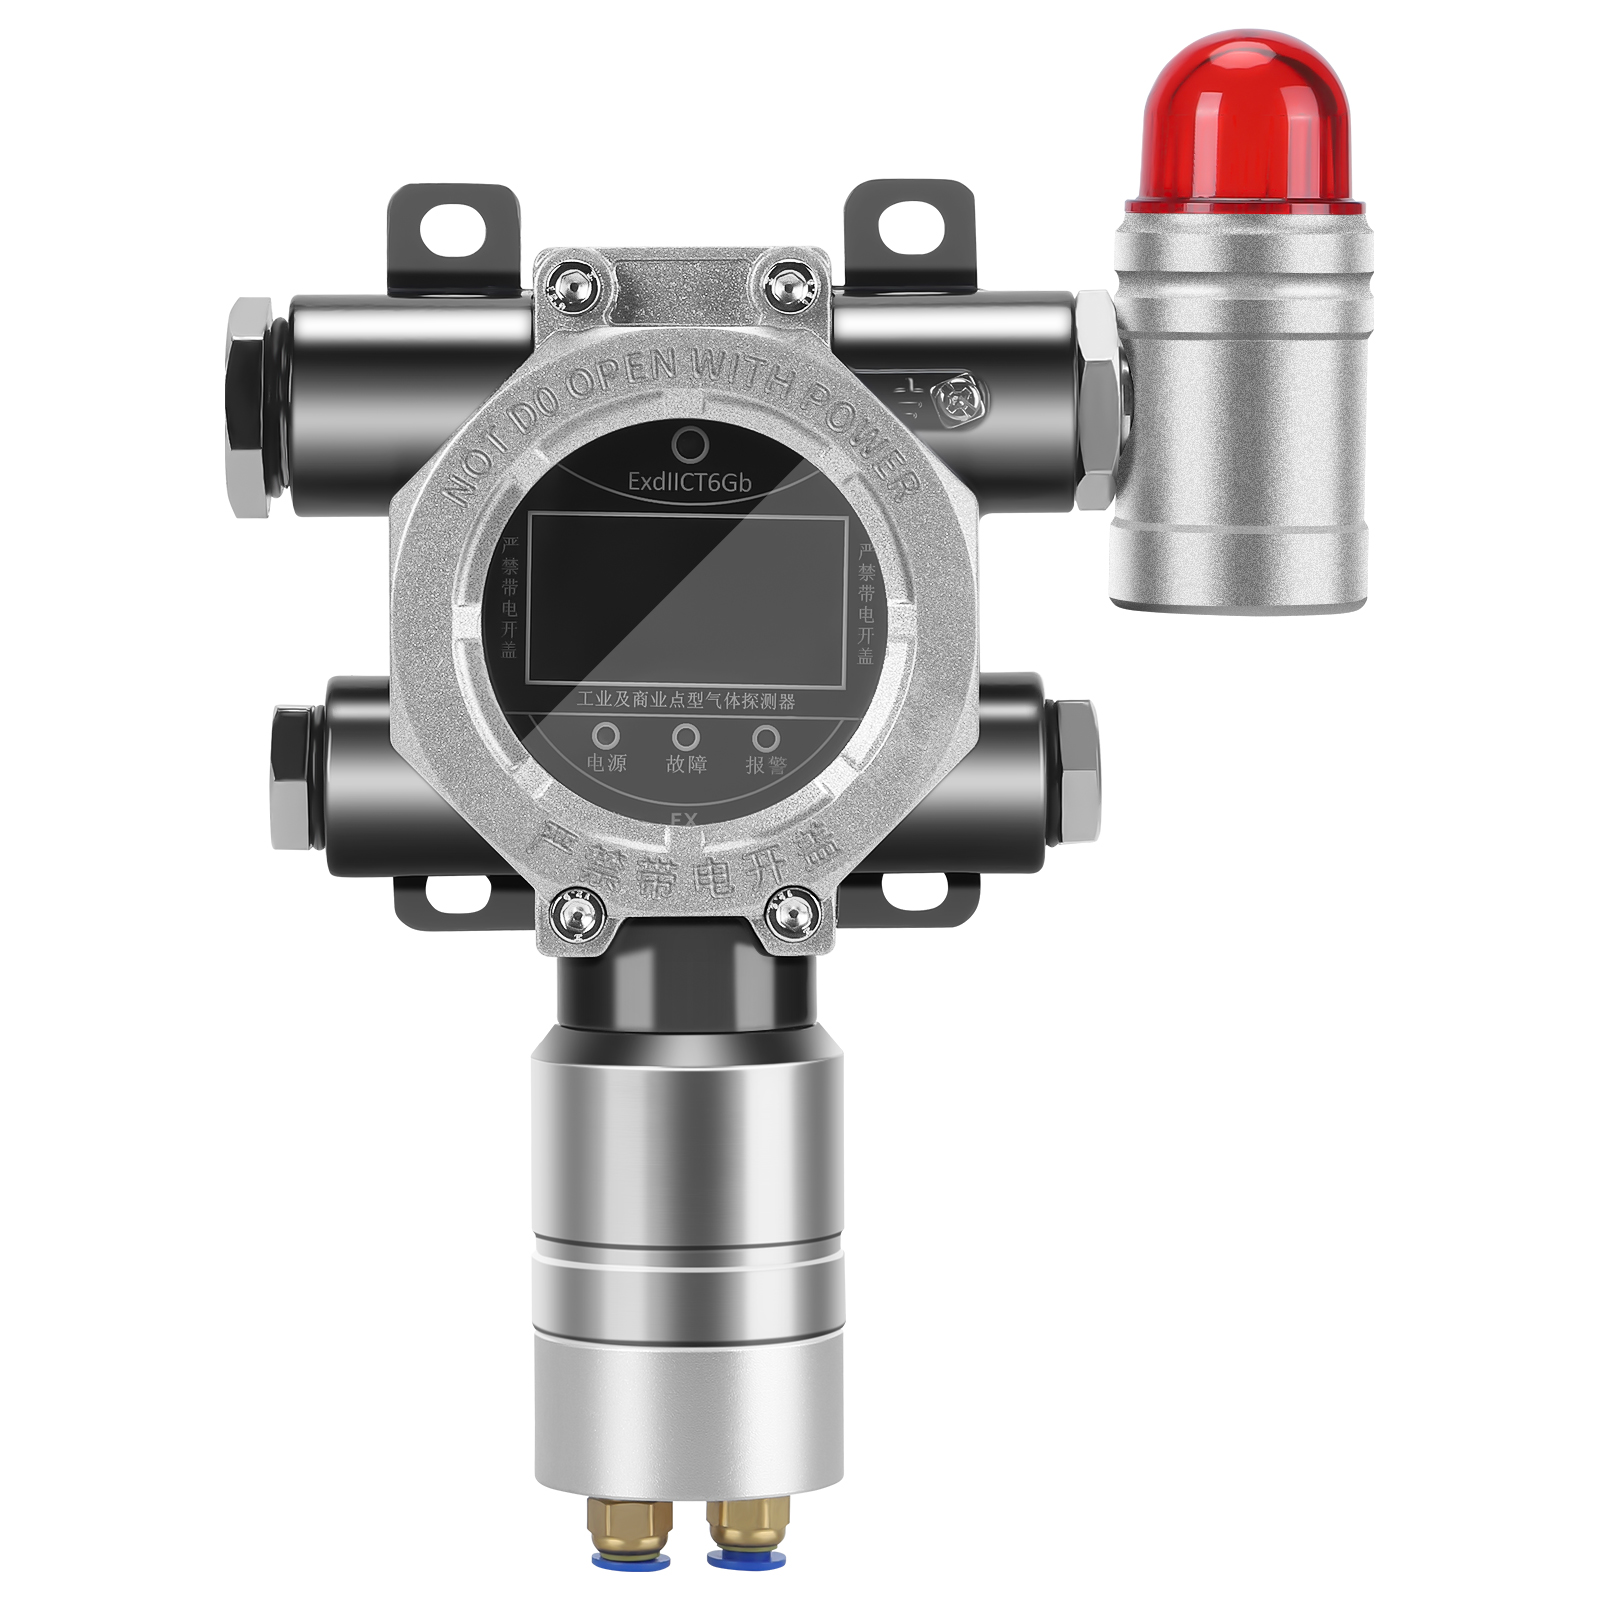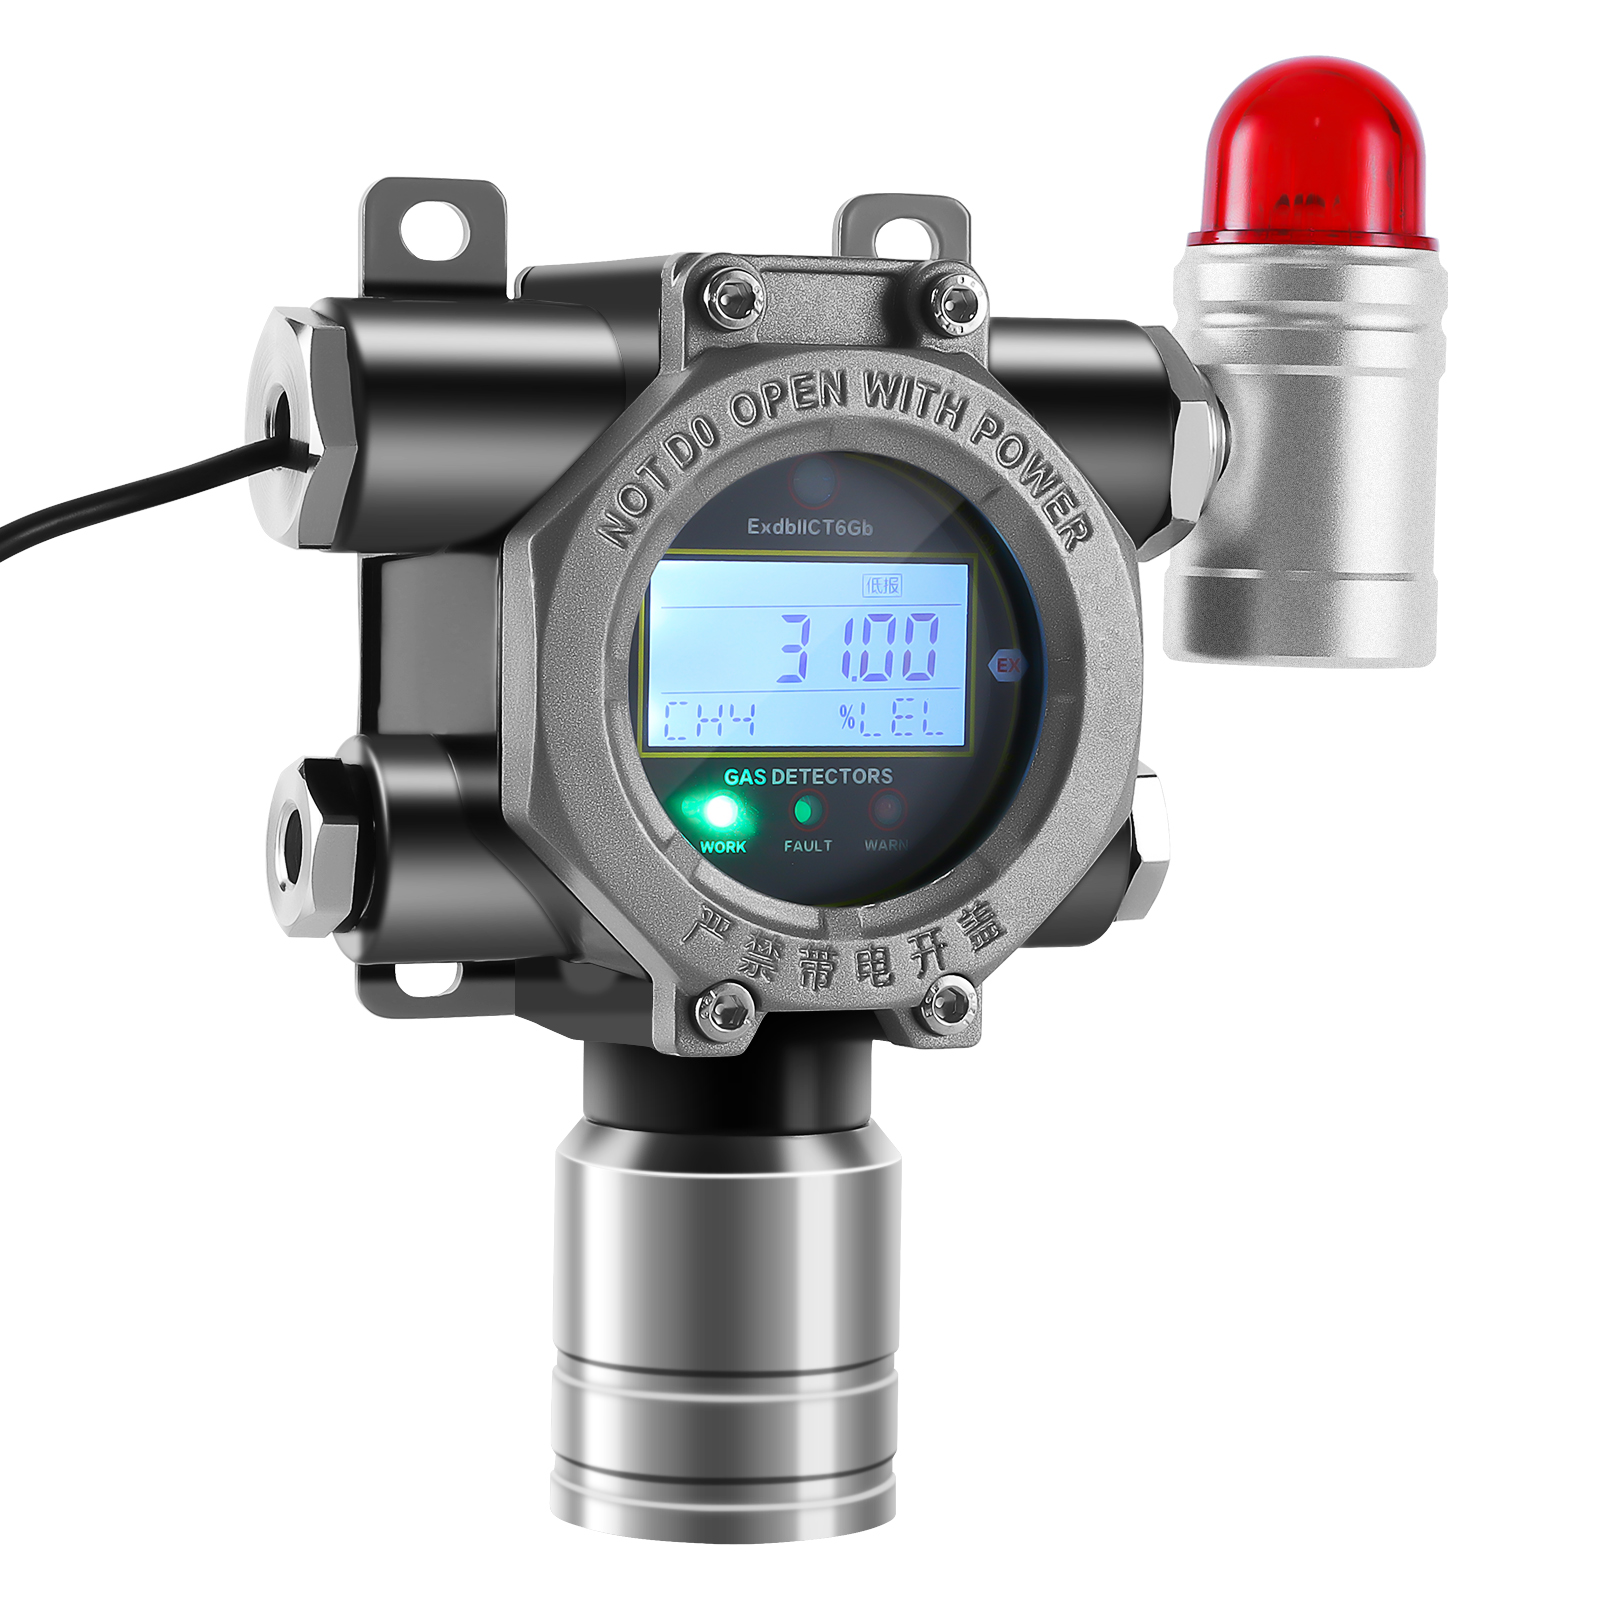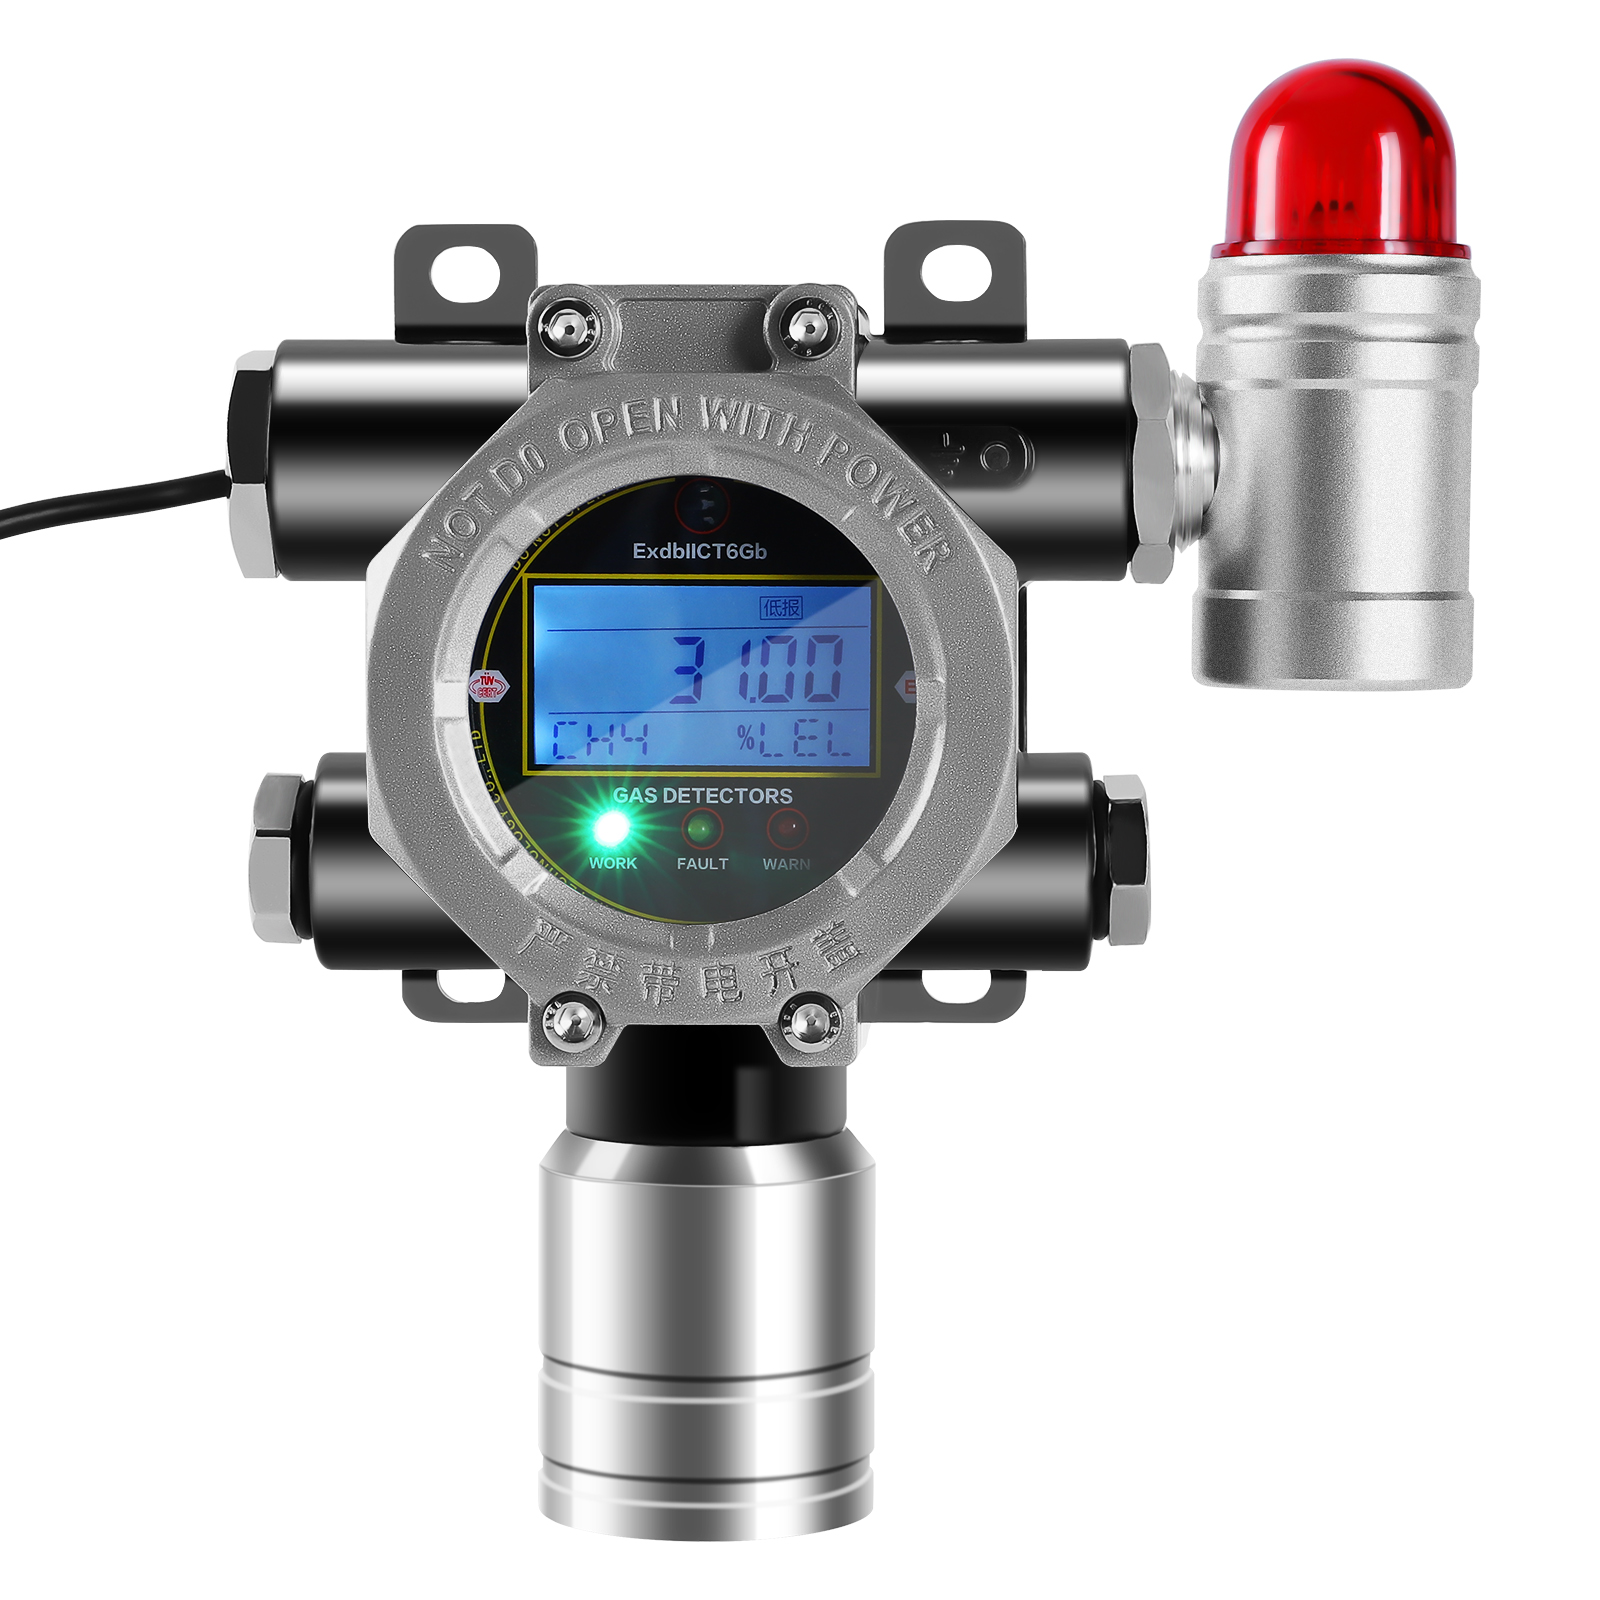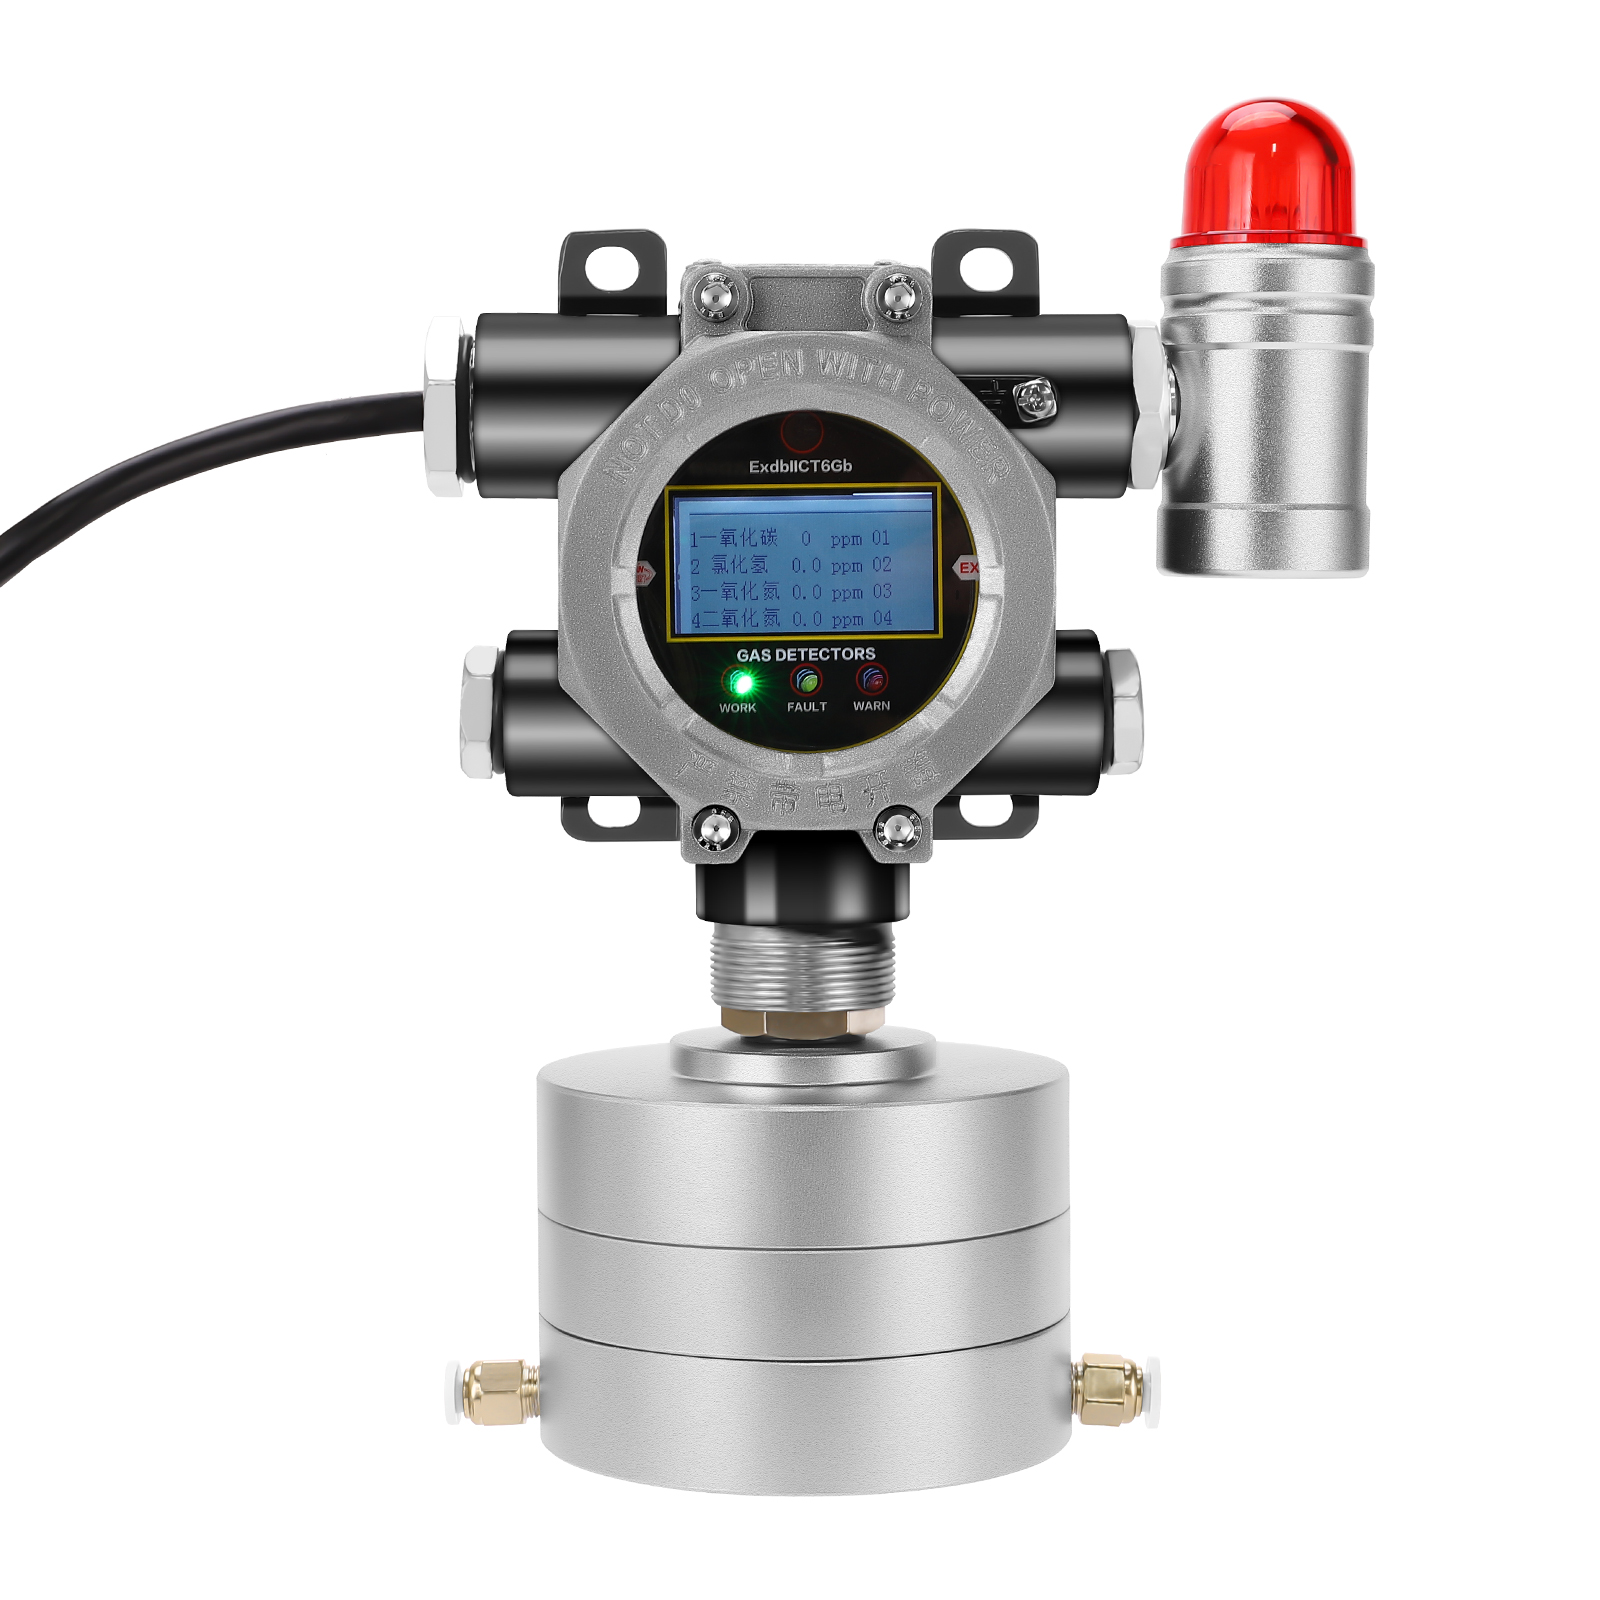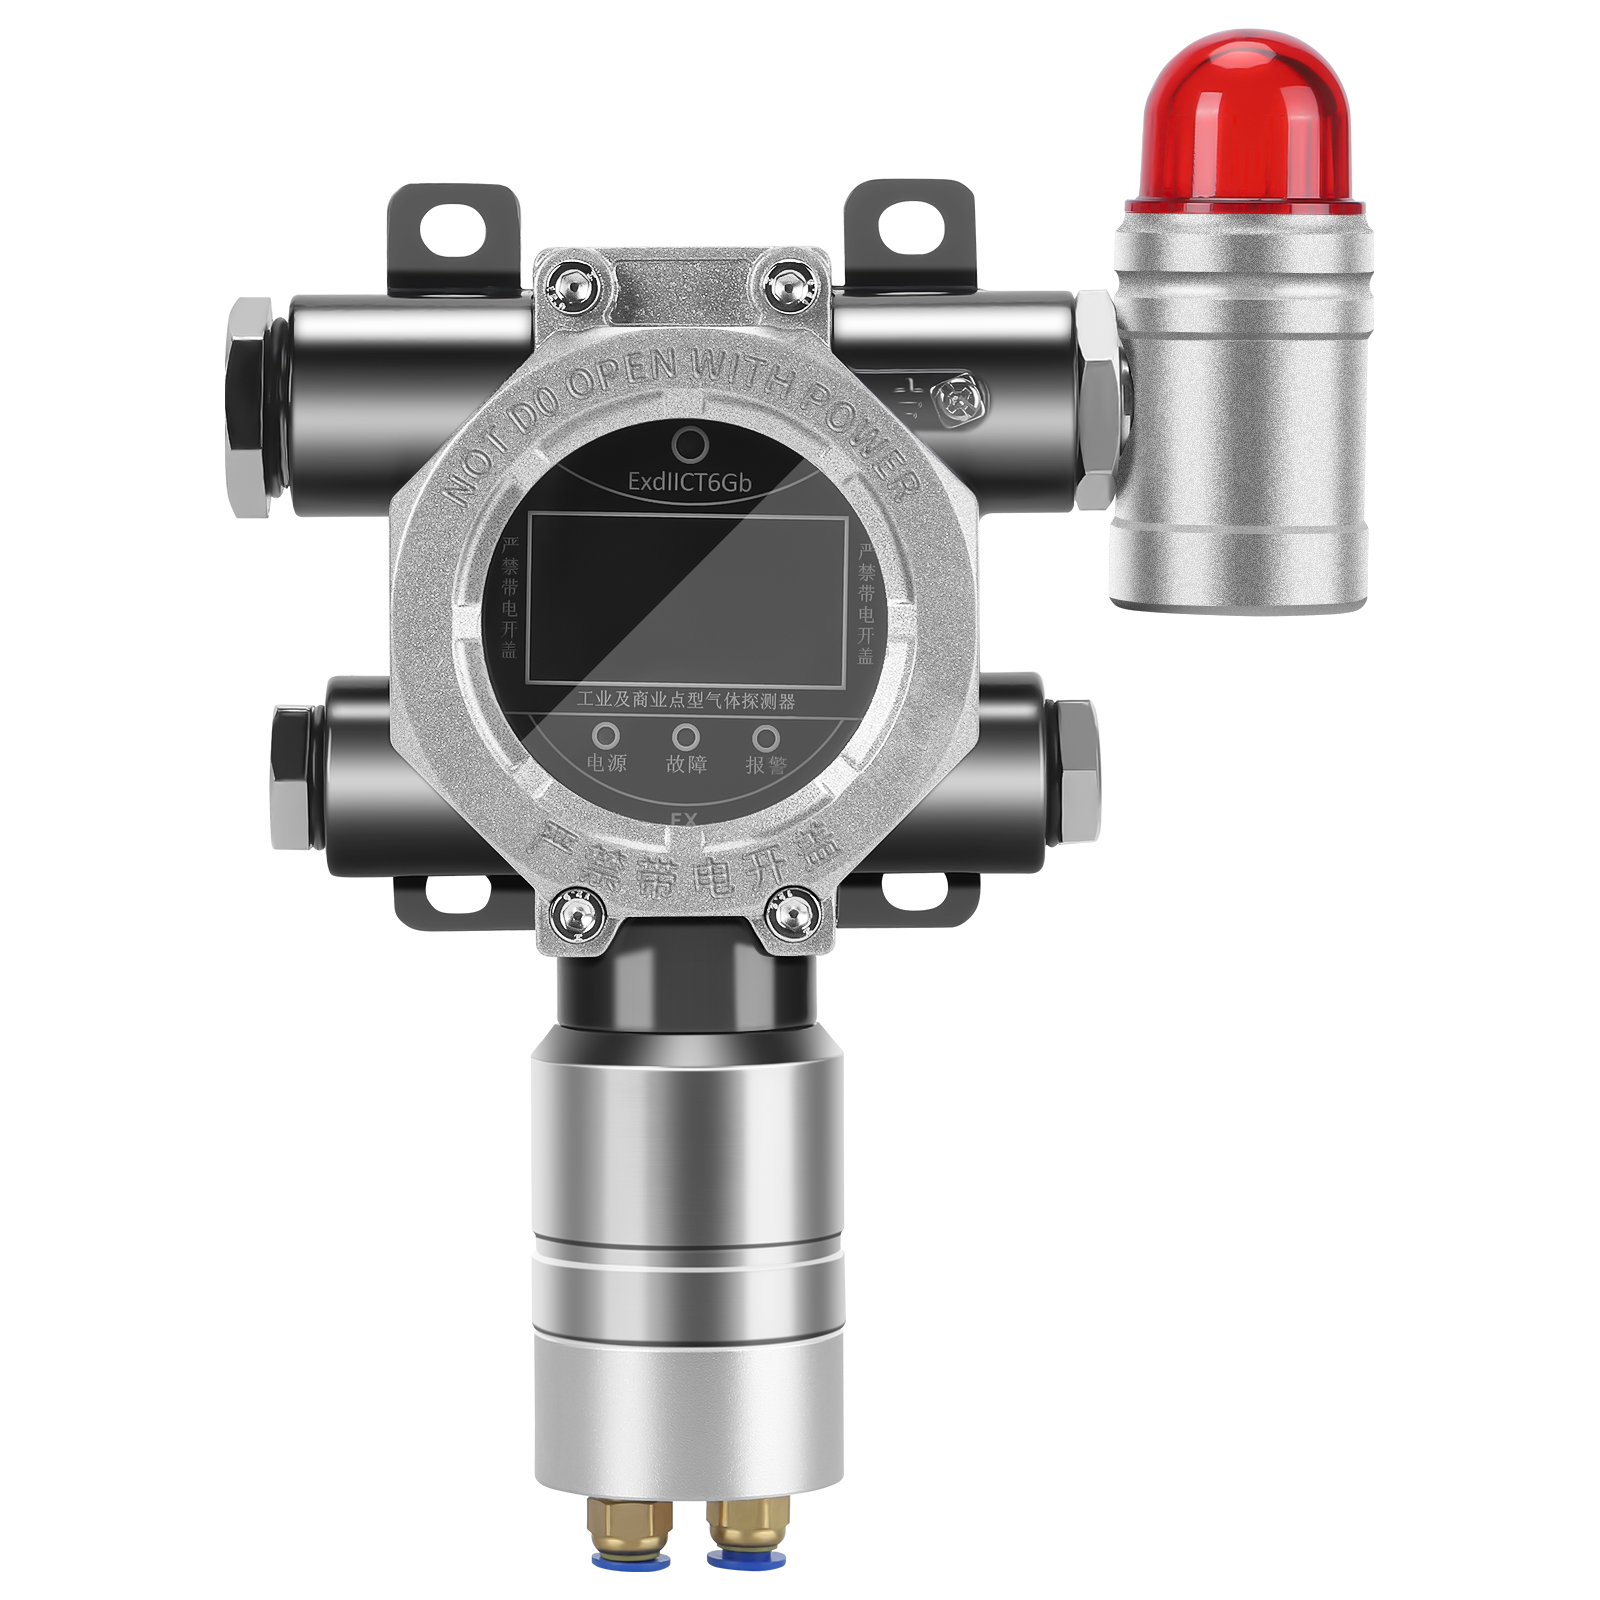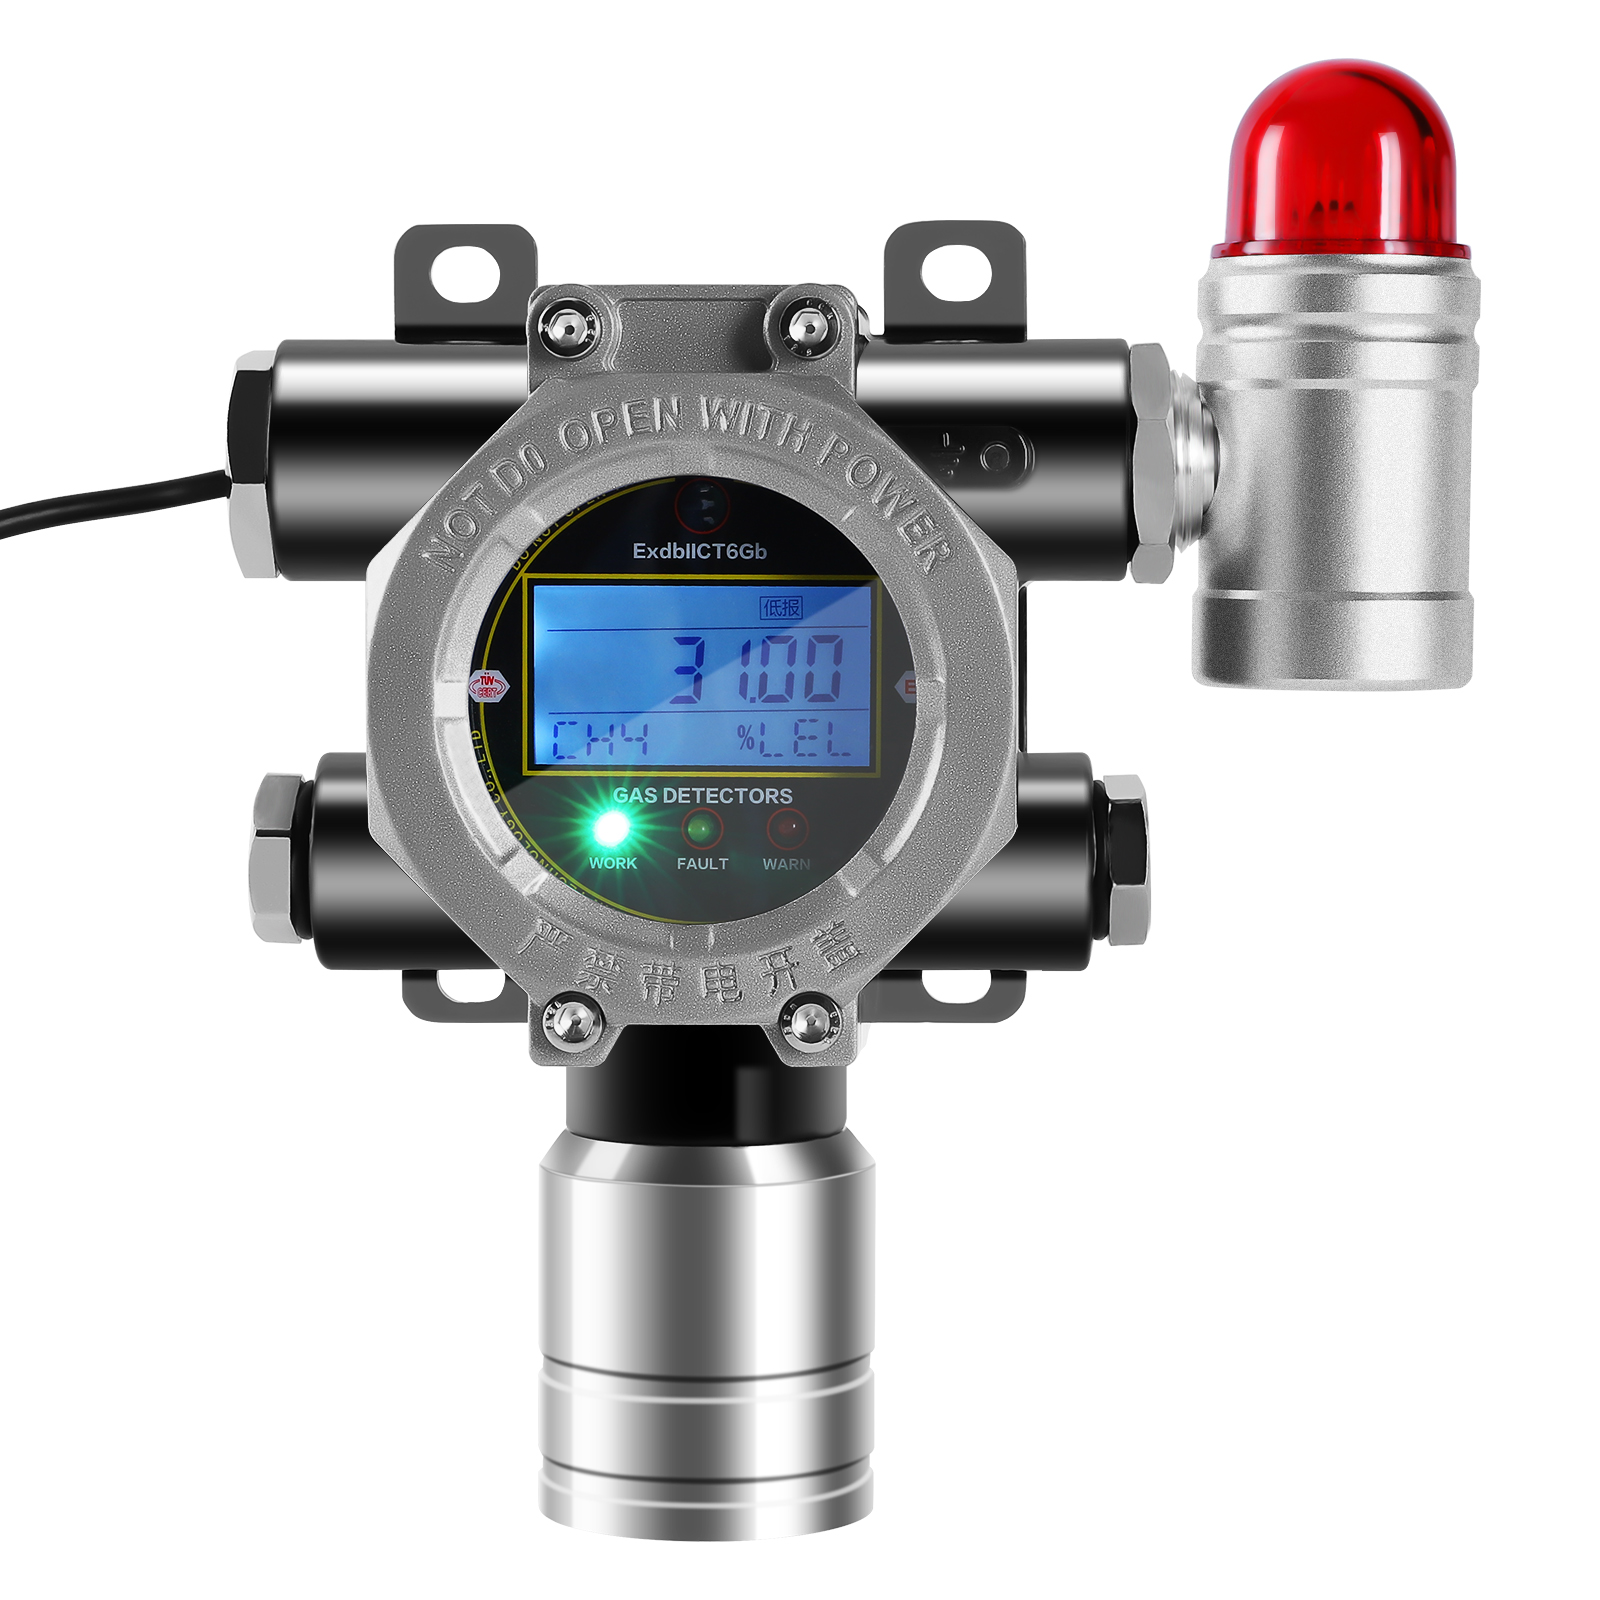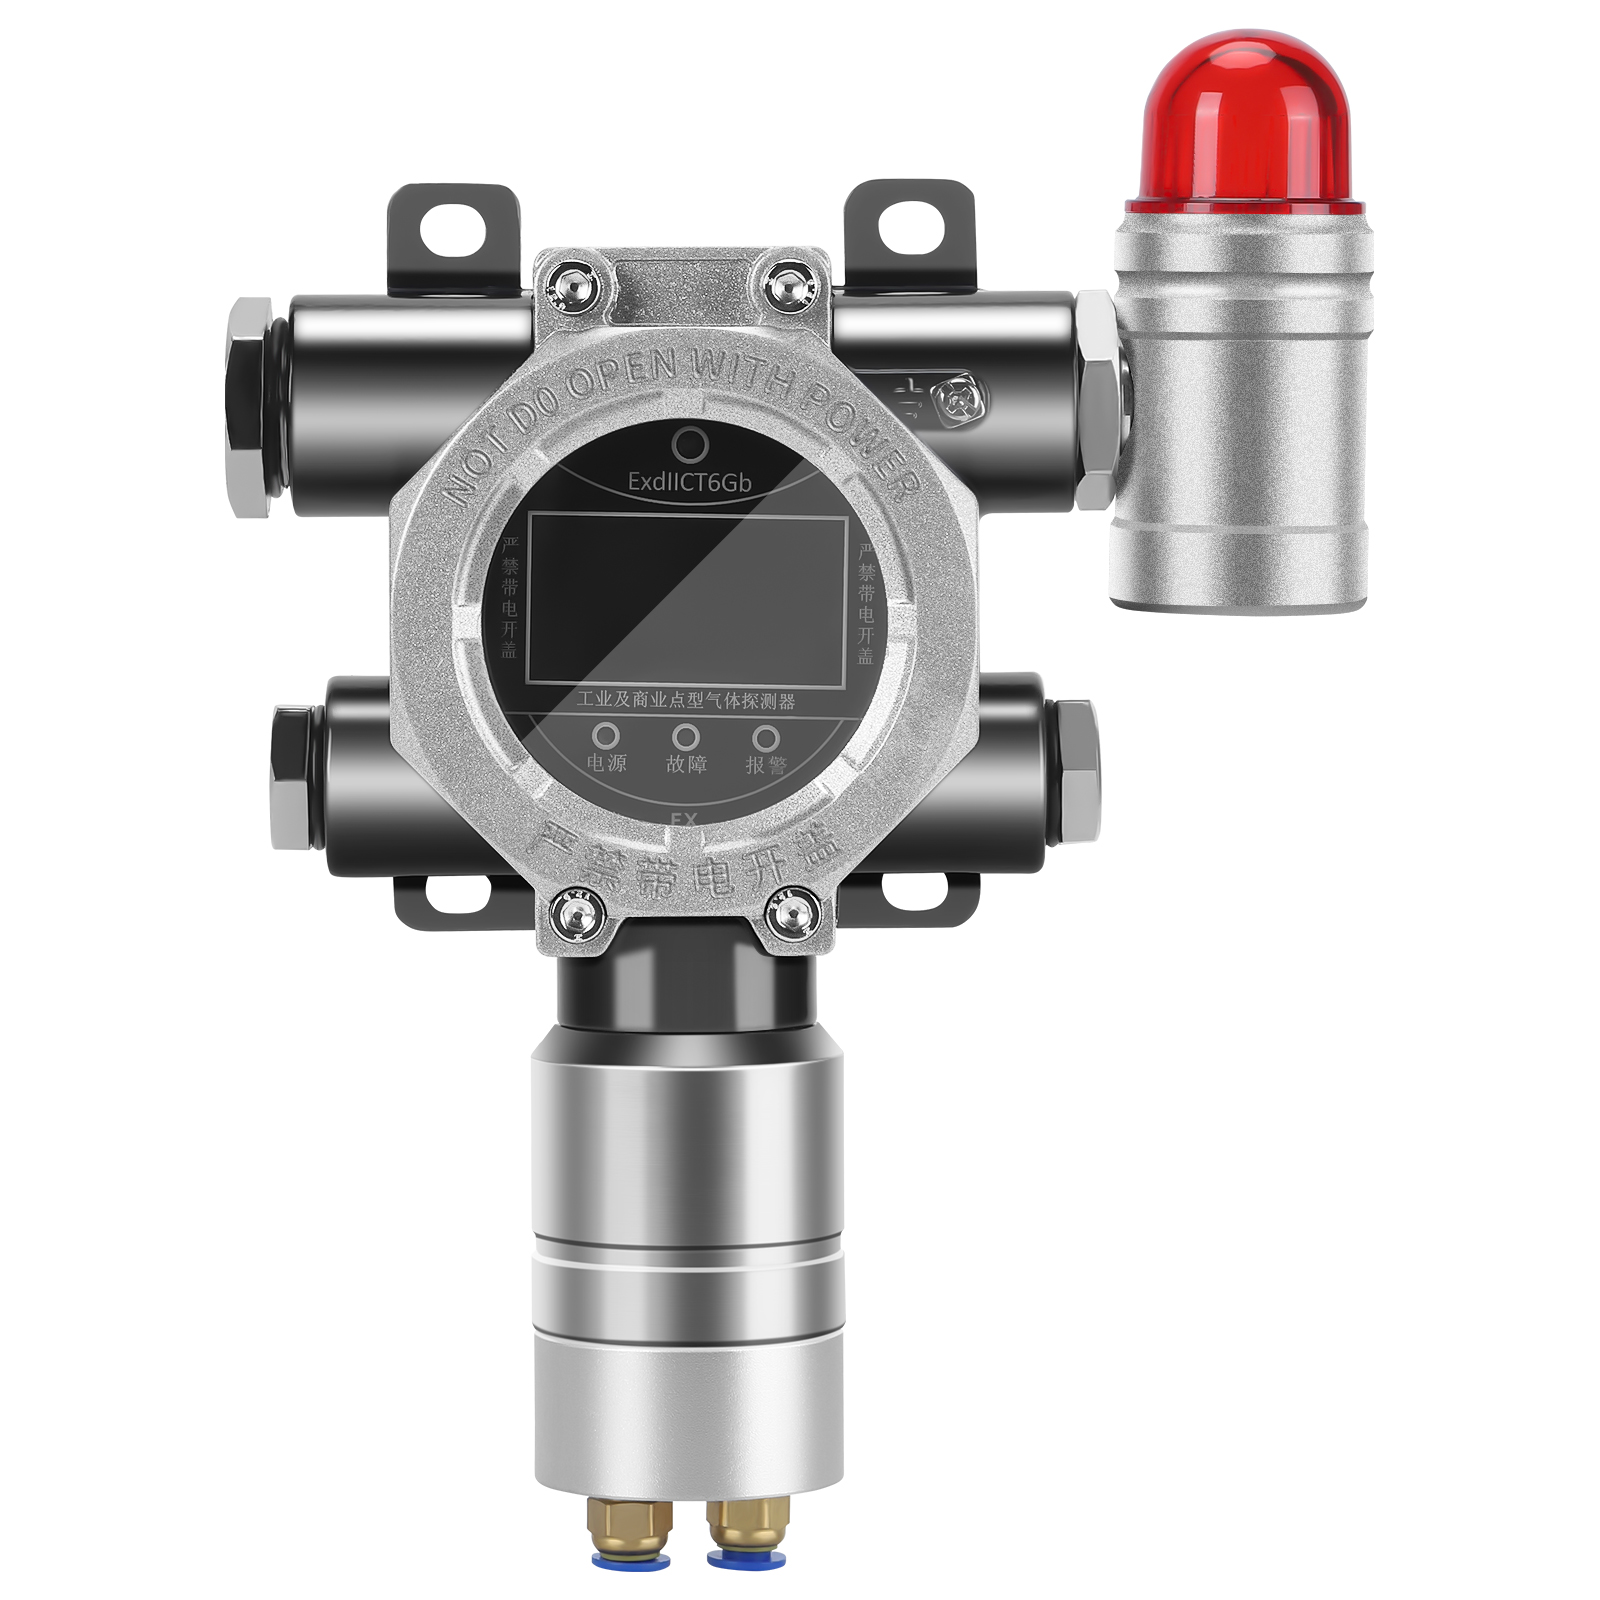
Methane Pump-Suction Detection Transmitter Fixed Safety Monitoring of Gas in Valve Wells - SKA/CH4-BJQ
• Measuring range: 0~100%LEL
• Accuracy: ±3%FS
• Resolution: 0.1%LEL
• Output signal: 4~20mA, RS485 Modbus, relay alarm output
• Power supply: DC24V
• Medium temperature: -20℃~50℃
• Working pressure: 80~120kPa
• Protection rating: IP66
• Explosion-proof rating: Ex d IIC T6 Gb
• Response time: ≤30s
• Alarm setpoint: 25%LEL (adjustable)
• Installation method: wall-mounted
• Warranty: 1 year
Product Introduction
Methane Pump-Suction Detection Transmitter Fixed Safety Monitoring of Gas in Valve Wells - Product Overview
The methane pump-suction detection transmitter is a pump-suction gas detection transmitter device used for fixed safety monitoring of gas in valve wells. Search keywords: methane pump-suction detection transmitter, fixed safety monitoring of gas in valve wells, methane alarm. The transmitter is fixedly installed in the valve well and draws gas from the well into the detection chamber through a sampling pump. It can continuously detect methane concentration and convert the concentration signal into a standard signal output. In fixed safety monitoring of gas in valve wells, the methane pump-suction detection transmitter can achieve active sampling and help operation and maintenance personnel understand the gas risks in the well.
Methane Pump-Suction Detection Transmitter Fixed Safety Monitoring of Gas in Valve Wells - Working Principle
Methane pump-suction detection transmitters usually use catalytic combustion sensors or infrared sensors, draw gas into the detection chamber through a sampling pump, detect methane concentration and output electrical signals, which are converted into 4-20mA, RS485, or Modbus signals after circuit processing. In fixed safety monitoring of gas in valve wells, methane pump-suction detection transmitters support remote calibration and fault self-diagnosis and can be connected to PLC, DCS, and gas alarm control systems. The transmitter is fixedly installed on the well wall or bracket and has an explosion-proof enclosure and a high protection rating, making it suitable for humid and explosion-proof environments in valve wells.
Methane Pump-Suction Detection Transmitter Fixed Safety Monitoring of Gas in Valve Wells - Application Scenarios
Methane pump-suction detection transmitters are widely used in gas valve wells, valve chambers, inspection wells, and underground pipeline nodes. In fixed safety monitoring of gas in valve wells, methane pump-suction detection transmitters can be fixedly installed on the well wall or bracket and collect gas in the well through a sampling tube. The transmitter can be linked with exhaust fans, shut-off valves, and fire protection systems to achieve automatic handling. For urban gas pipeline networks, methane pump-suction detection transmitters can also form a multi-point monitoring network and upload data uniformly to the control room.
Methane Pump-Suction Detection Transmitter Fixed Safety Monitoring of Gas in Valve Wells - Technical Advantages
Methane pump-suction detection transmitters have advantages such as active sampling, fast response, and good stability. In fixed safety monitoring of gas in valve wells, methane pump-suction detection transmitters use explosion-proof design and corrosion-resistant materials, making them suitable for humid and explosion-proof environments. The transmitter supports remote calibration, fault self-diagnosis, and remote communication, making maintenance convenient. When selecting a methane pump-suction detection transmitter, attention should be paid to detection range, accuracy, response time, explosion-proof rating, and sampling distance to ensure it meets the needs of fixed safety monitoring of gas in valve wells.