Product Introduction
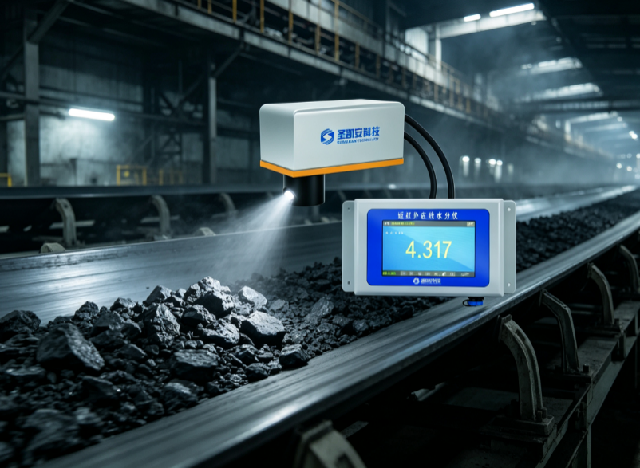
Rubber powder near-infrared on-line water monitoring systems.
Overview of products
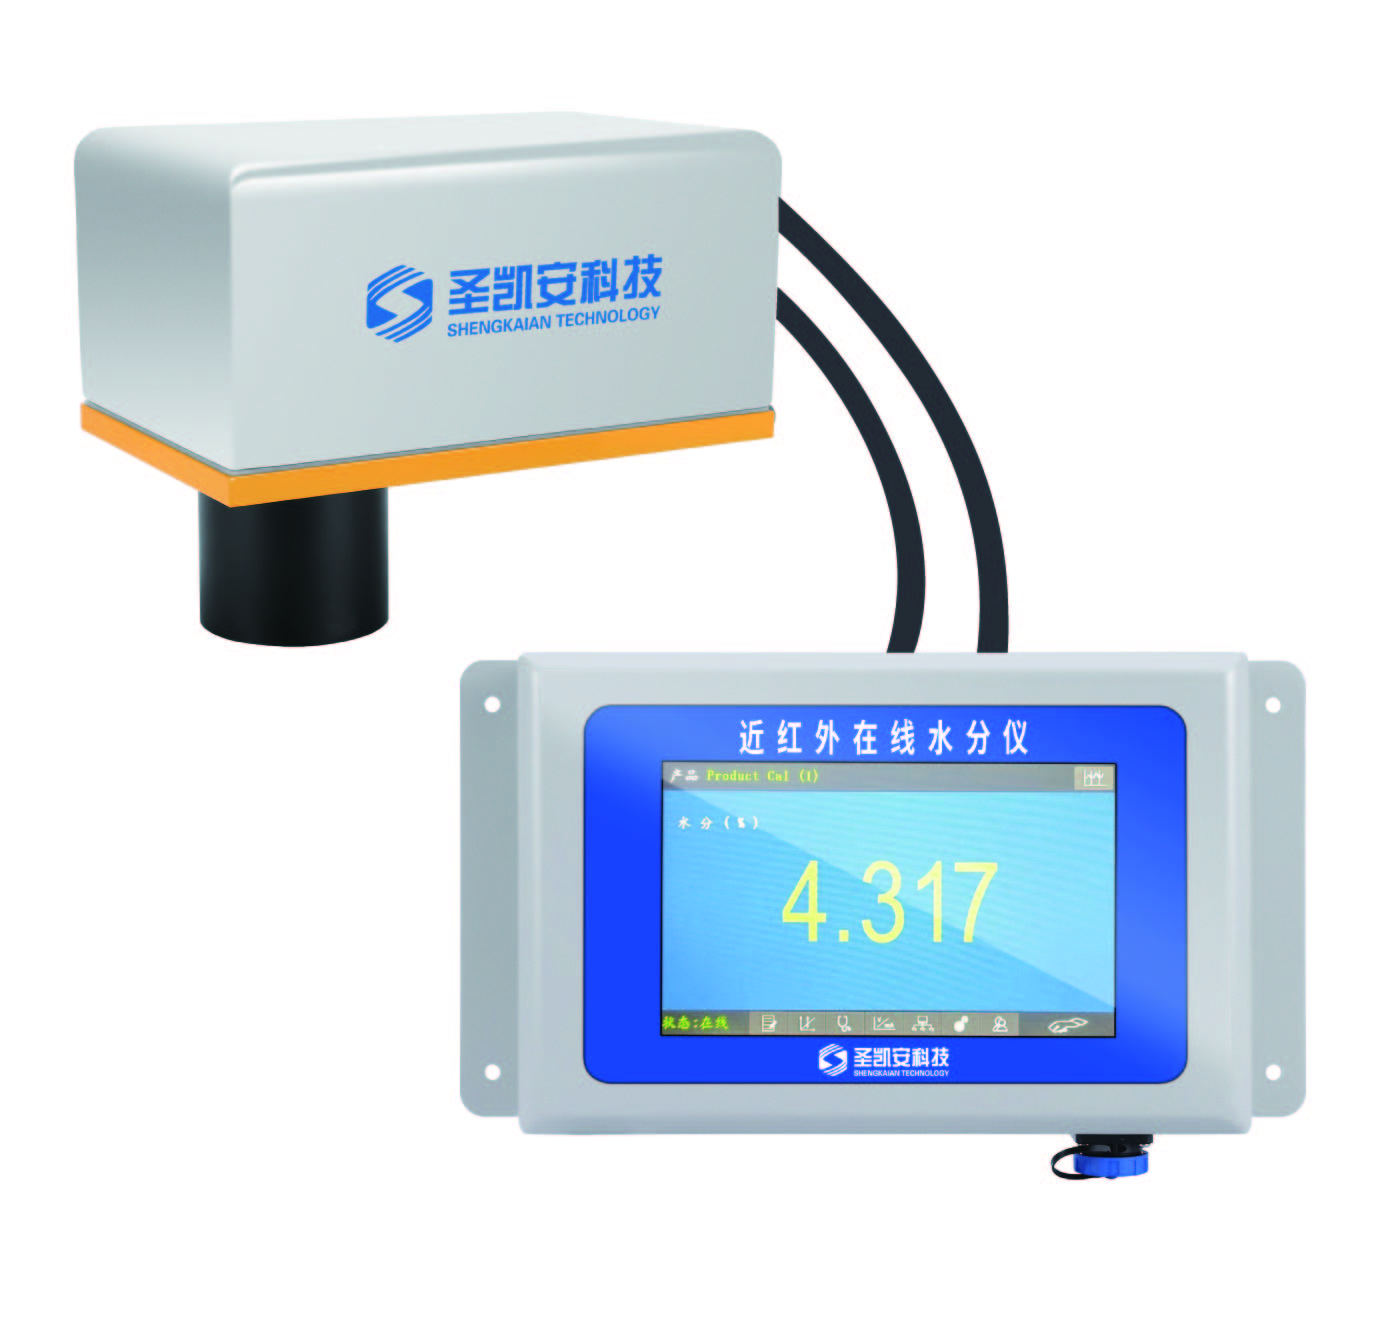
Rubber powder near-infrared on-line water monitoring systems.It's based on...The principle of near-infrared spectrum analysisNon-exposure industrial real-time moisture detection equipment. The equipment uses water molecules to characterize the absorption properties of near-infrared light in a given wave range. Through optical detection, spectroscopy analysis and algorithms, the surface and internal water content of materials are measured in real time, without sampling, drying or contact with materials, and continuous on-line monitoring of current water line materials is conducted around the clock.
The equipment is widely adapted to all types of solid particles, powders, tablets and fibres production lines. It completely addresses the pain points of the slow, faulty, inefficient and inert production of traditional samples. It provides accurate data support for industrial automated production, quality control, optimization of energy consumption and upgrading of capacity. It is the core detection equipment for modern smart manufacturing and precision production.
II. Rationale
Rubber powder near-infrared on-line water monitoring systems.The equipment optical probes launch a specific wavelength near-infrared light source, irradiated on the material surface of the fluid line movement, and the water molecule produces selective absorption of a specific spectrum band. The probe collects a spectral signal in real time after the material is reflected and converts the light signal into a telecommunications transmission to the master control system.
The system produces real-time water content data for the material, based on a built-in high-precision algorithm model that filters interference factors such as dust, light, material thickness, colour, etc., and also produces a standard signal interfacePLC、DCS, Industrial control systems to achieve real-time data display, automatic control, ultra-restrictive alarms and automated closed loop control for water detection.
Core product advantages
- Non-contact non-destructive detection(b) High-level, high-level production sites such as food, building materials, chemicals, light work, etc., without exposure to materials, product patterns, wear and tear, pollution.
- Continuous real-time testing: millisecond response speed,24Hourly on-line monitoring, real-time feedback of water fluctuations in material, and a complete departure from laboratory sampling delayed detection models.
- High accuracy and stability.(b) Carrying smart anti-disruption algorithms that automatically compensate for detection errors resulting from environmental light, dust, thinness of materials and colour differences, and measuring data stable and accurate.
- Very compatible.: Support4-20mA、RS485For standard industrial signal output, there's no gap between factory systems,PLC, touch screens, top machines, adapted to automated production line modifications.
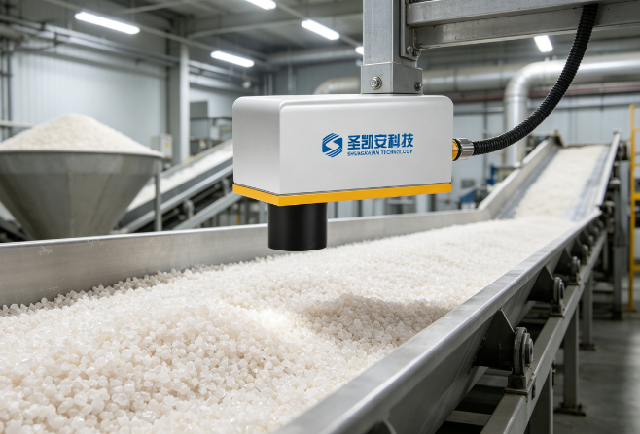
- Installation easy, maintenance simple(c) Structure modular design that is flexible enough to be installed in such positions as belt-flowing waterlines, sluices, silos, vents and so forth, with no loss of material, free of frequent calibration at a later stage, and minimal transport costs.
- Smart data controlSupport for real-time data, data storage, historical curve queries, ultrasound alerts, which assist producers to adjust process parameters in a timely manner and stabilize product quality.
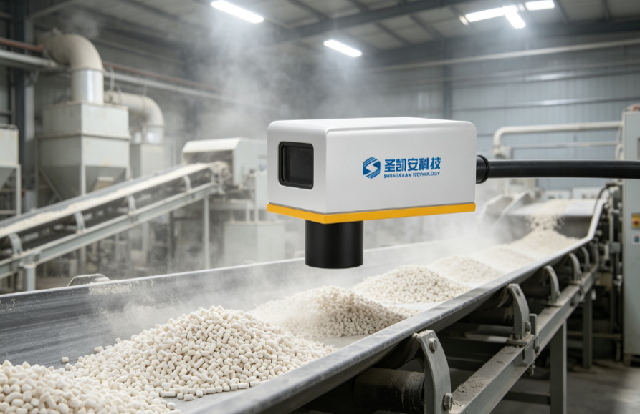
- Compatible complex work(b) A whole machine of dust, tide, anti-disruption design, with the option of blast control, suitable for poor production environments such as dust, damp, industrial interference, etc.
IV. MAIN FUNCTIONS
- Infrared hydrometer onlineReal-time online water content testing, second-level data updates, dynamic monitoring of material moisture changes;
- (a) Automatic calibration of smart algorithms, long-term use of data without drift and good measurement of duplication;
- Support for the storage of multi-group material models, one-key switching of detection material, and multi-product production;
- (b) Water over-alert automatic alert, real-time uploading of data, and closed-ring regulation of assistive production processes;
- (b) Modularized structure, separation of the mainframe from the probe and adaptation of all types of field installation;
- Low-utility design, stable operation, low-noise, suitable for long-term continuous industrialization.
Applicable industry and detection material
This rubber powder is close to the Infrared Water Monitoring System.Water online testingThe core application industry is as follows:
- Paper packaging industryPaper, cardboard, cardboard, cardboard, cardboard, pulp, etc.;
- Wood panels industry(b) Wood crumbs, wood powder, cut flowers, slabs, bamboo and planks, density sheet materials, etc.;
- Food feed industryFlour, groceries, feed particles, fodder powder, grain raw materials, etc.;
- Tobacco and tea industry(a) Smoke leaves, smoke wires, barbs, various types of dry tea, tea preparation, etc.;
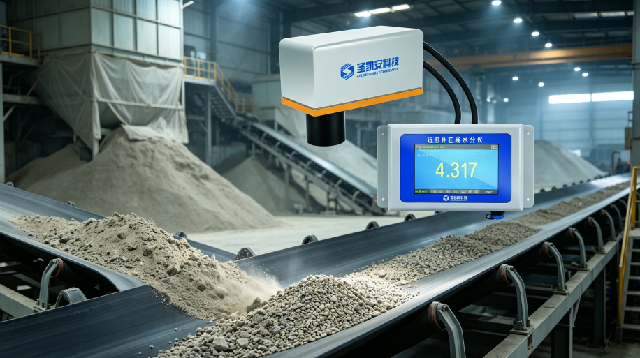
- Construction materials, chemical industry(a) Sandstones, ore powder, sludge, fertilizer powder, powdered chemical materials, etc.;
- Rubber Light IndustriesPlastic particles, plastic particles, resin powder, rubber materials, etc.
VI. Value of equipment applications
- Steady product quality(a) Monitoring material moisture on a real-time basis to avoid excess or non-achievement of the water content of finished products and to reduce secondary and back-to-work rates;
- Improving productivity(a) Alternative manual sampling tests to eliminate sampling, drying, testing processes and significantly increase production flow efficiency;
- Production cost savings• Quality control of water to reduce material loss, dry energy consumption, optimize production processes and reduce business operating costs;
- Aided intelligence manufacturing(a) Visualization of production data, automation of process regulation, intelligent adaptation plants, digital upgrading needs;
- Standardized production controlThe data are retroactive and meet industry quality checks, environmental reviews, standardized production audits.
VII. Composition of equipment
Equipment set byNear-infrared detection probe (head)+ Smart master carrier+ Show Terminals+ Signal Transfer ModuleComposition, simple structure, flexible assembly, installation and measurement according to field conditions Cheng, contact:xiaojianfeng@nesensor.com
Main Application Areas
- Rubber Powder Production — Real-time moisture monitoring during rubber powder milling and drying processes to ensure consistent product quality.
- Rubber Recycling — Monitoring moisture content in recycled rubber powder to optimize processing parameters and improve efficiency.
- Rubber Compounding — Ensuring precise moisture levels in rubber compounds to maintain batch-to-batch consistency and prevent defects.
- Quality Control — Continuous inline measurement for quality assurance, reducing waste and rework in rubber manufacturing.
Keywords:rubber powder moisture analyzer, NIR moisture meter, online moisture monitoring, rubber processing moisture control, near-infrared moisture sensor, industrial moisture analyzer, rubber powder moisture measurement, AMT/SFY-HW