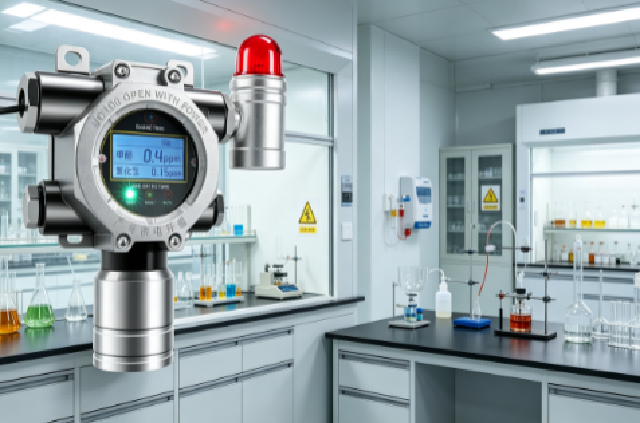
Product Introduction
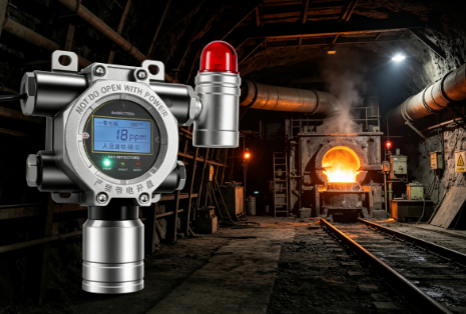
Nitrogen oxide detectors in smelters Industrial smelting gas concentration monitoring
Overview of products
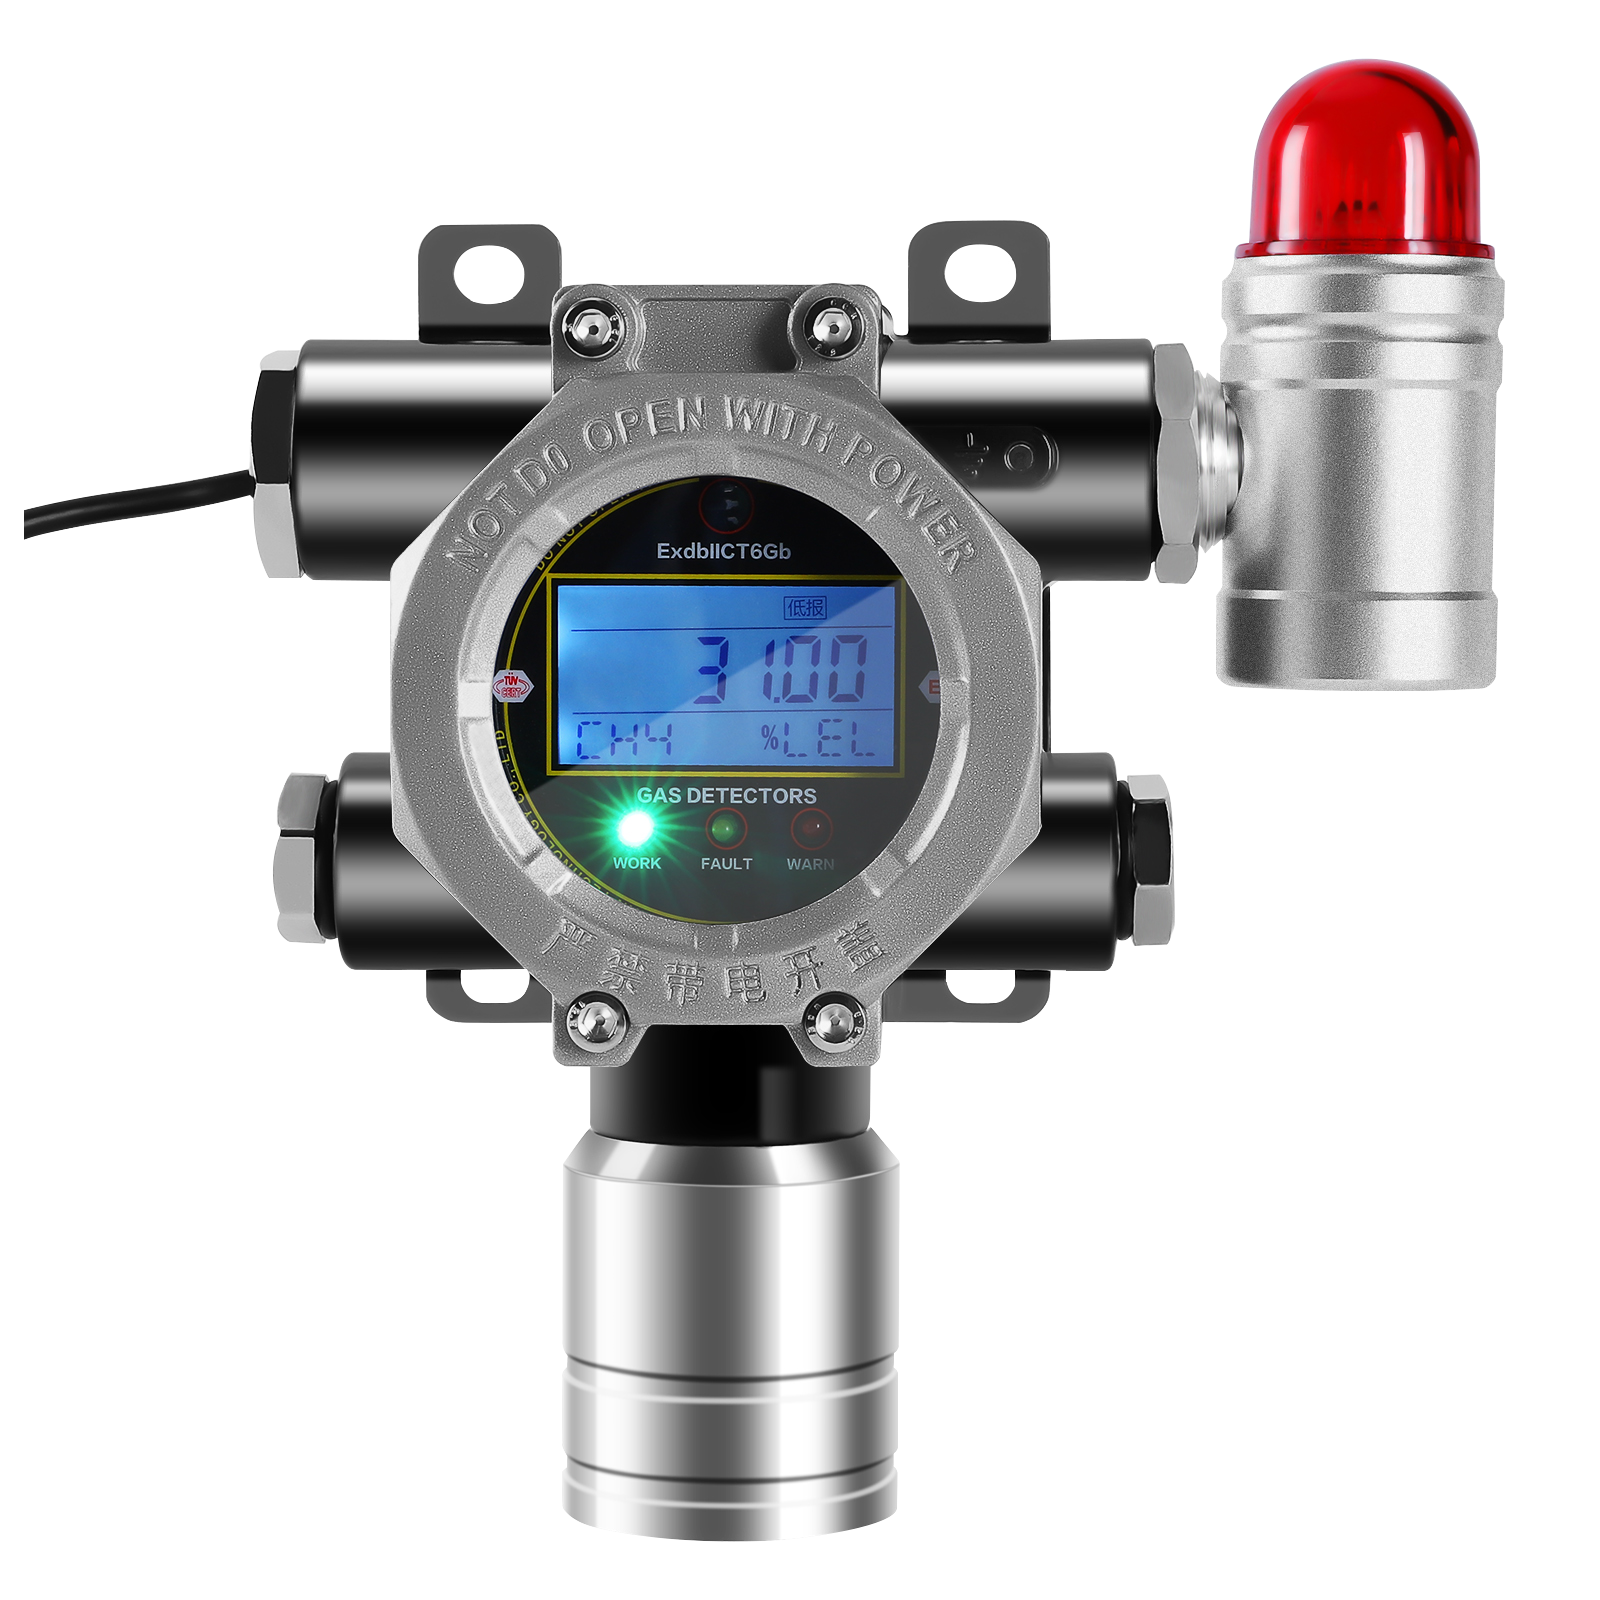
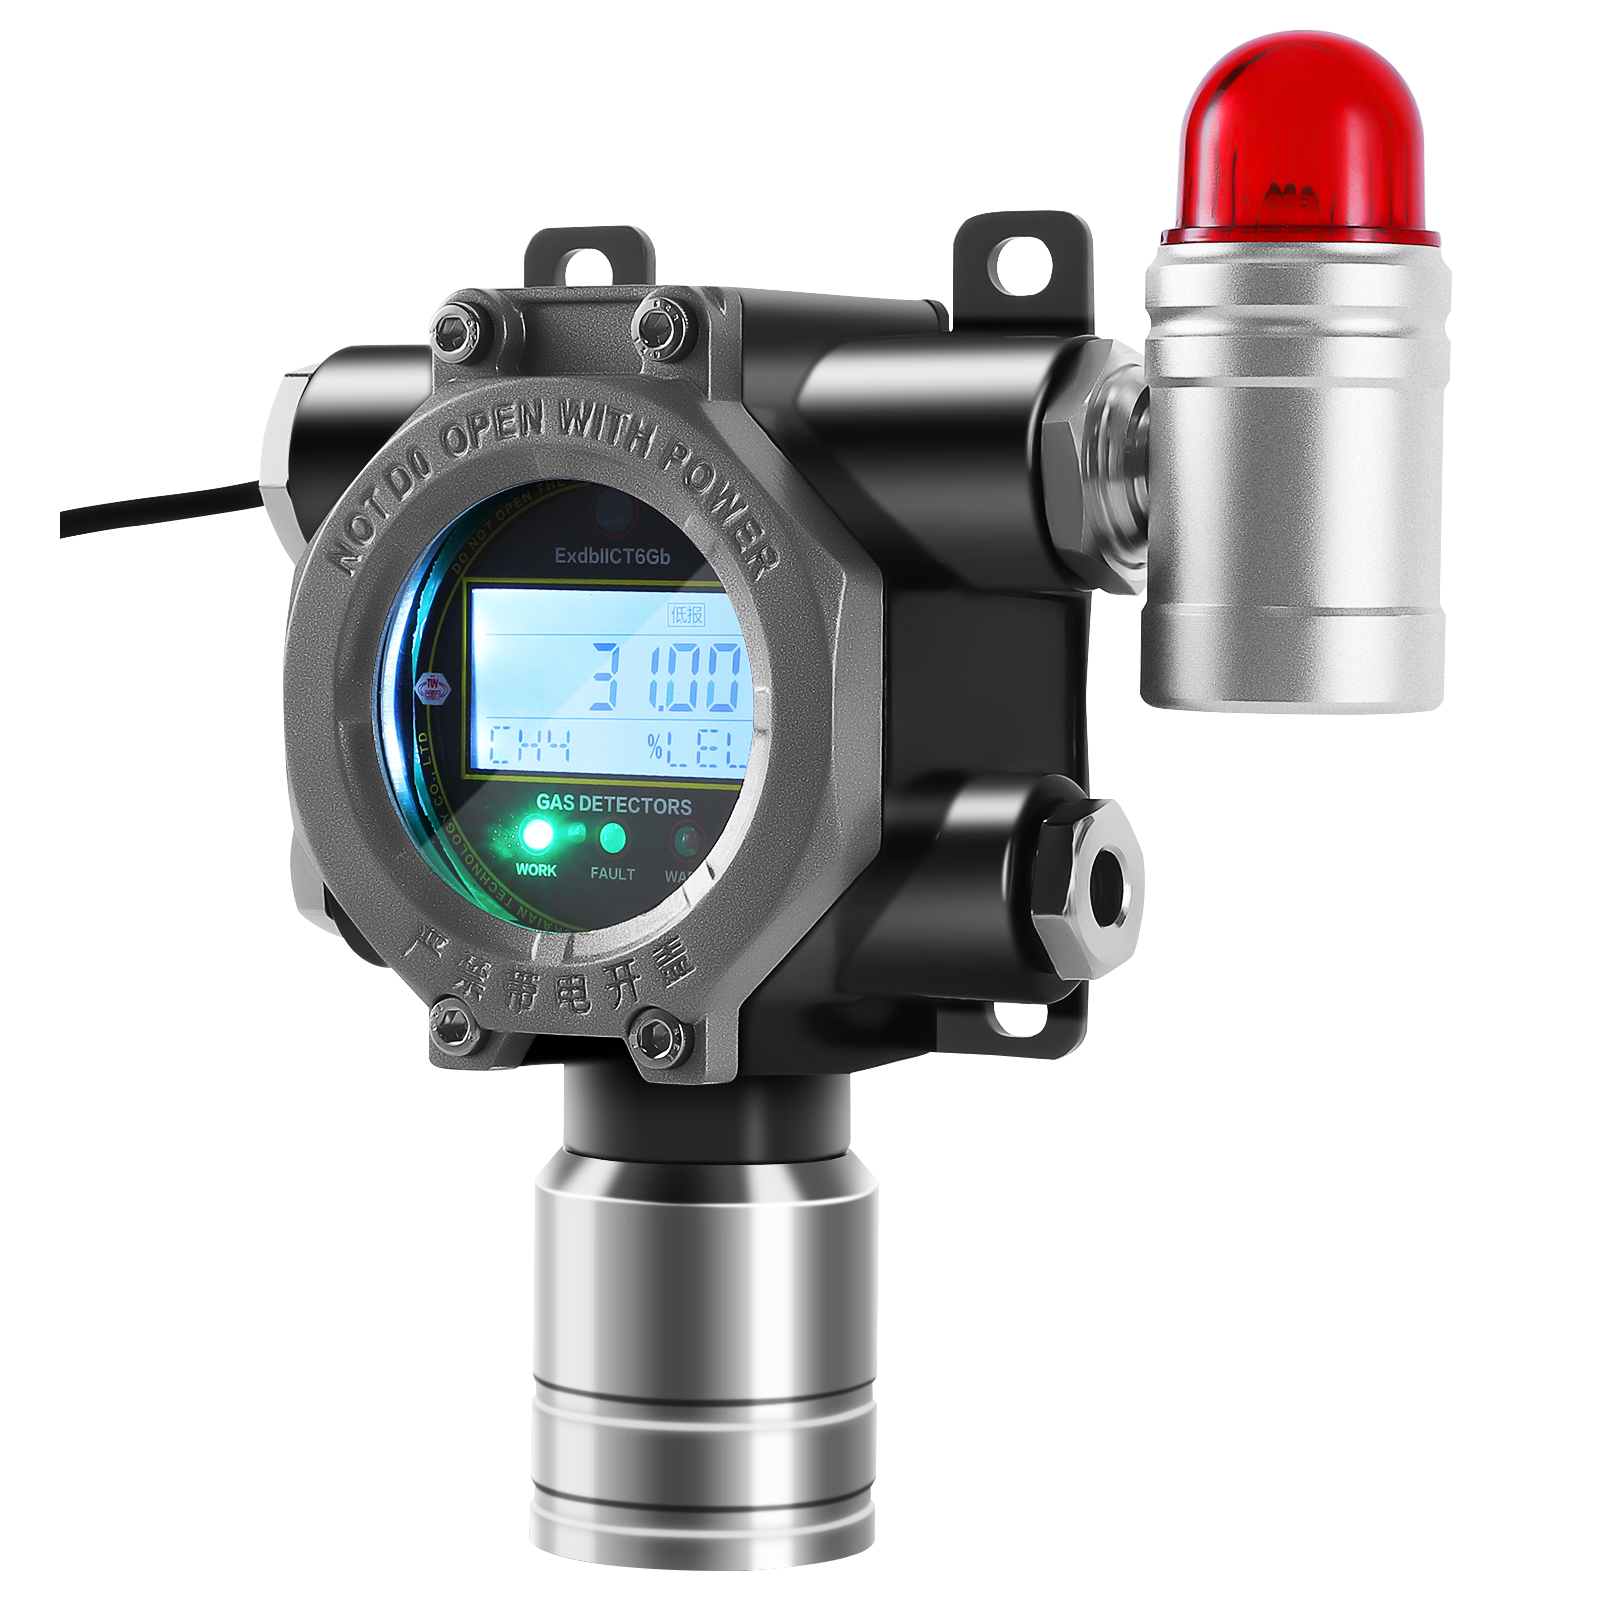
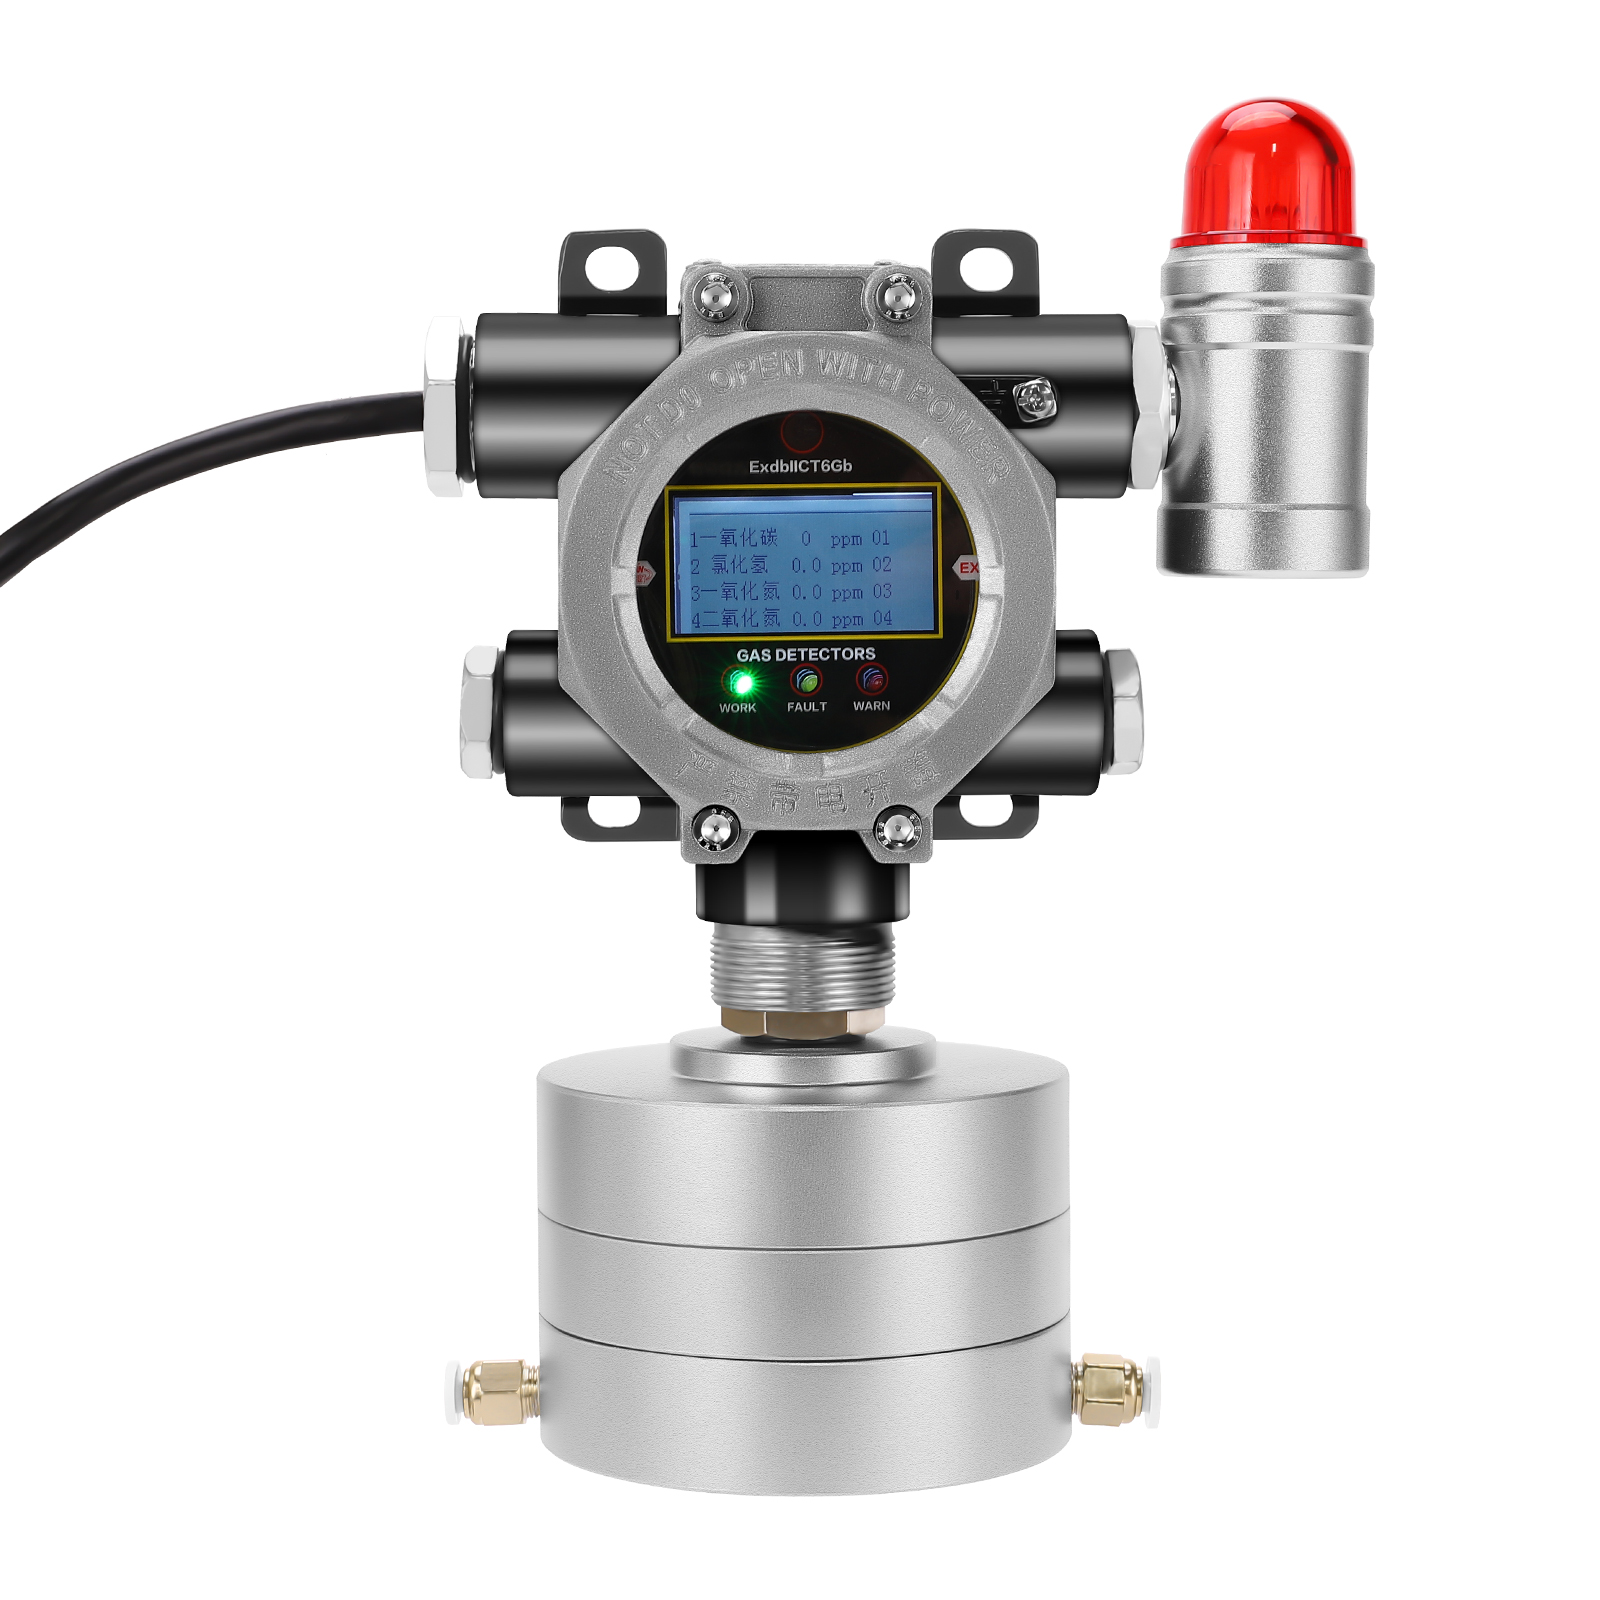
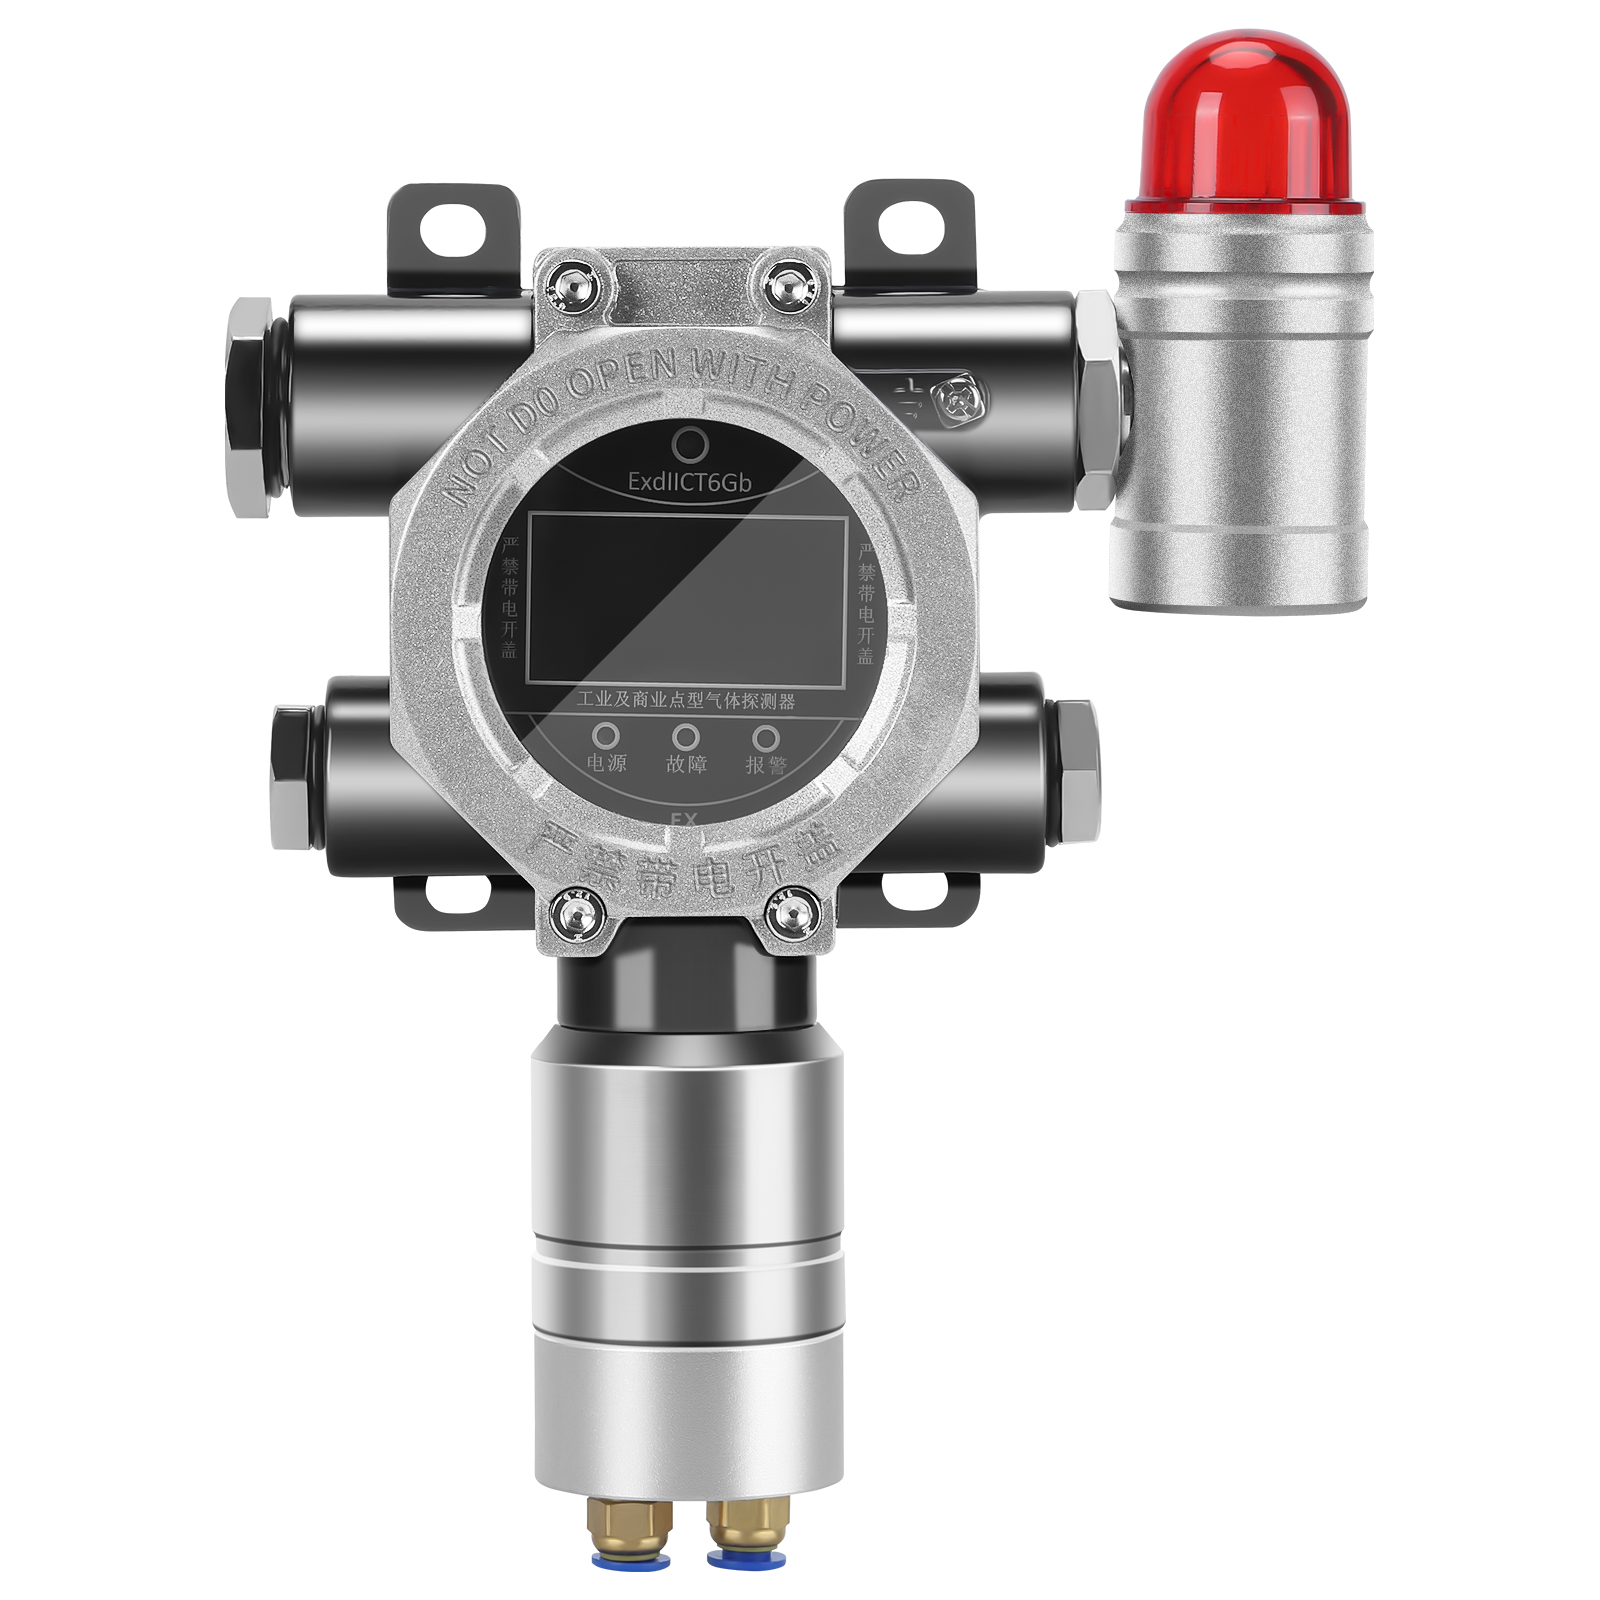
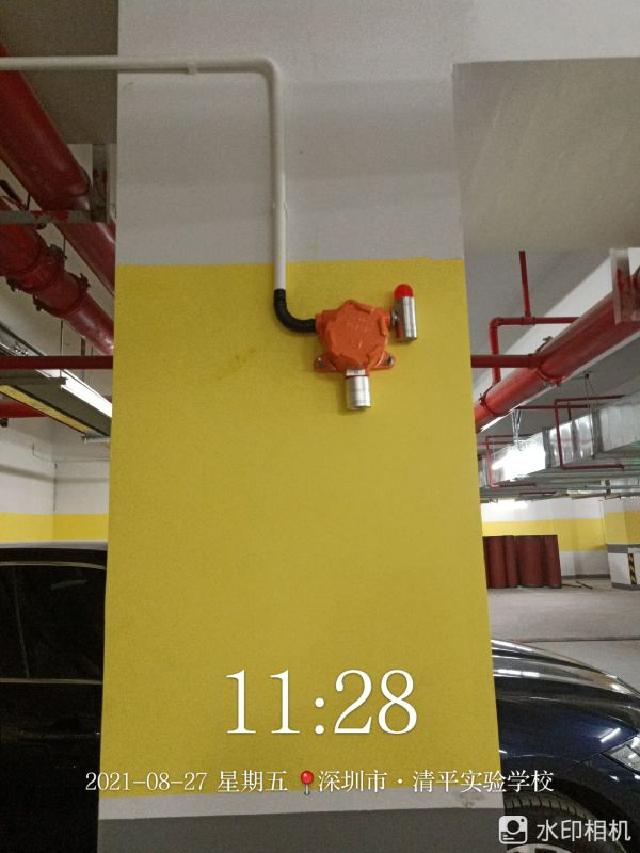
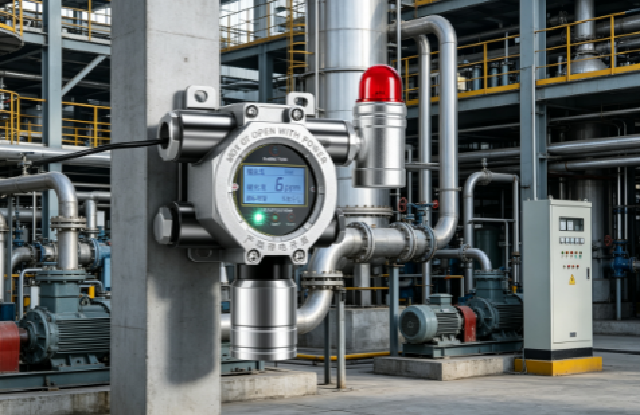
An industrial composite gas detector is a multi-principled, high-stable, blast-proof industrial gas concentration online monitoring device. Equipment integrates a variety of mainstream detection sensor techniques, which automatically match the best detection methods according to the type of gases detected, and are suitable for the monitoring of multiple industrial gas leaks such as flammable gases, toxic and harmful gases and volatile gases. The whole machine uses industrial insulation structures, diffuse sampling,24Hour-to-hour on-line monitoring design with adaptive, low-utility, high-output, long-life and broadly appropriate featurespetrochemicals, coal-chemicals, precision chemicals, coating sprays, sewage treatment, pharmaceutical workshops, metallurgy mines, gas fields, storage stores, lithium new energy, food processing, municipal tunnelsIndustries and public places with the risk of flammable explosive and toxic harmful gases can provide accurate monitoring of on-site gas leaks, concentrations, etc., and provide reliable data support and security for safe production in the plant area, early warning of gas leaks, secure containment ring controls, and help enterprises to comply with safe production.
Core test principles
This device is compatibleCatalytic combustion, electrochemical, semiconductor, infraredThe four main principles of mainstream detection, covering all-product industrial gas detection needs, fit for different gas detection scenarios, and complete upgrading of accuracy and applicability. Catalytic combustion principles are used primarily for the detection of flammable gases, using temperature and resistance changes resulting from non-flammation of gases on the surface of catalytic elements, precision conversion of gas concentrations, good linearity and high stability; electrochemical principles for toxic trace gases, such as carbon monoxide and hydrogen sulfide, generating corresponding current signals through electrode oxidation reaction, with a strong and low sensitivity; semiconductor principles for wide-spectrum gas screening, which are responsive, cost-effective and environmentally adaptable; and infrared principles for detection of gases based on a spectral absorption characteristic, with a high degree of interference, no risk of poisoning and a high degree of long-term stability. Multi-principle modular design that can be adapted to achieve a truly multi-purpose, fully-covered landscape.
III. Product function and structural advantages
Smelting workshop nitrogen oxide detector Industrial smelting waste gas concentration monitoring using standardized industrial structure design with low overall power1.2W, energy-efficient and stable, suitable for long-term uninterrupted service. AdoptSpreading sampling methodsThere is no need for external air pumps, and natural gas dispersion is used to carry out detections, which are simple, easy to maintain and are not easily blocked. The whole machine is designed to be blast-proof and has a reliable blast-proof capability that fully meets the standards for blast-proof installation at hazardous sites. Equipment to support continuous online working mode, available24Continuous collection of data on gas concentrations, real-time monitoring of changes in environmental gases and elimination of safety monitoring of blind areas. At the same time, the equipment has excellent insulation capabilities and routine insulation electrical resistance.≥100MΩIn high-humid environments, work remains stable, with a strong resistance to wet heat and disturbance.
IV. Signal output and system adaptation
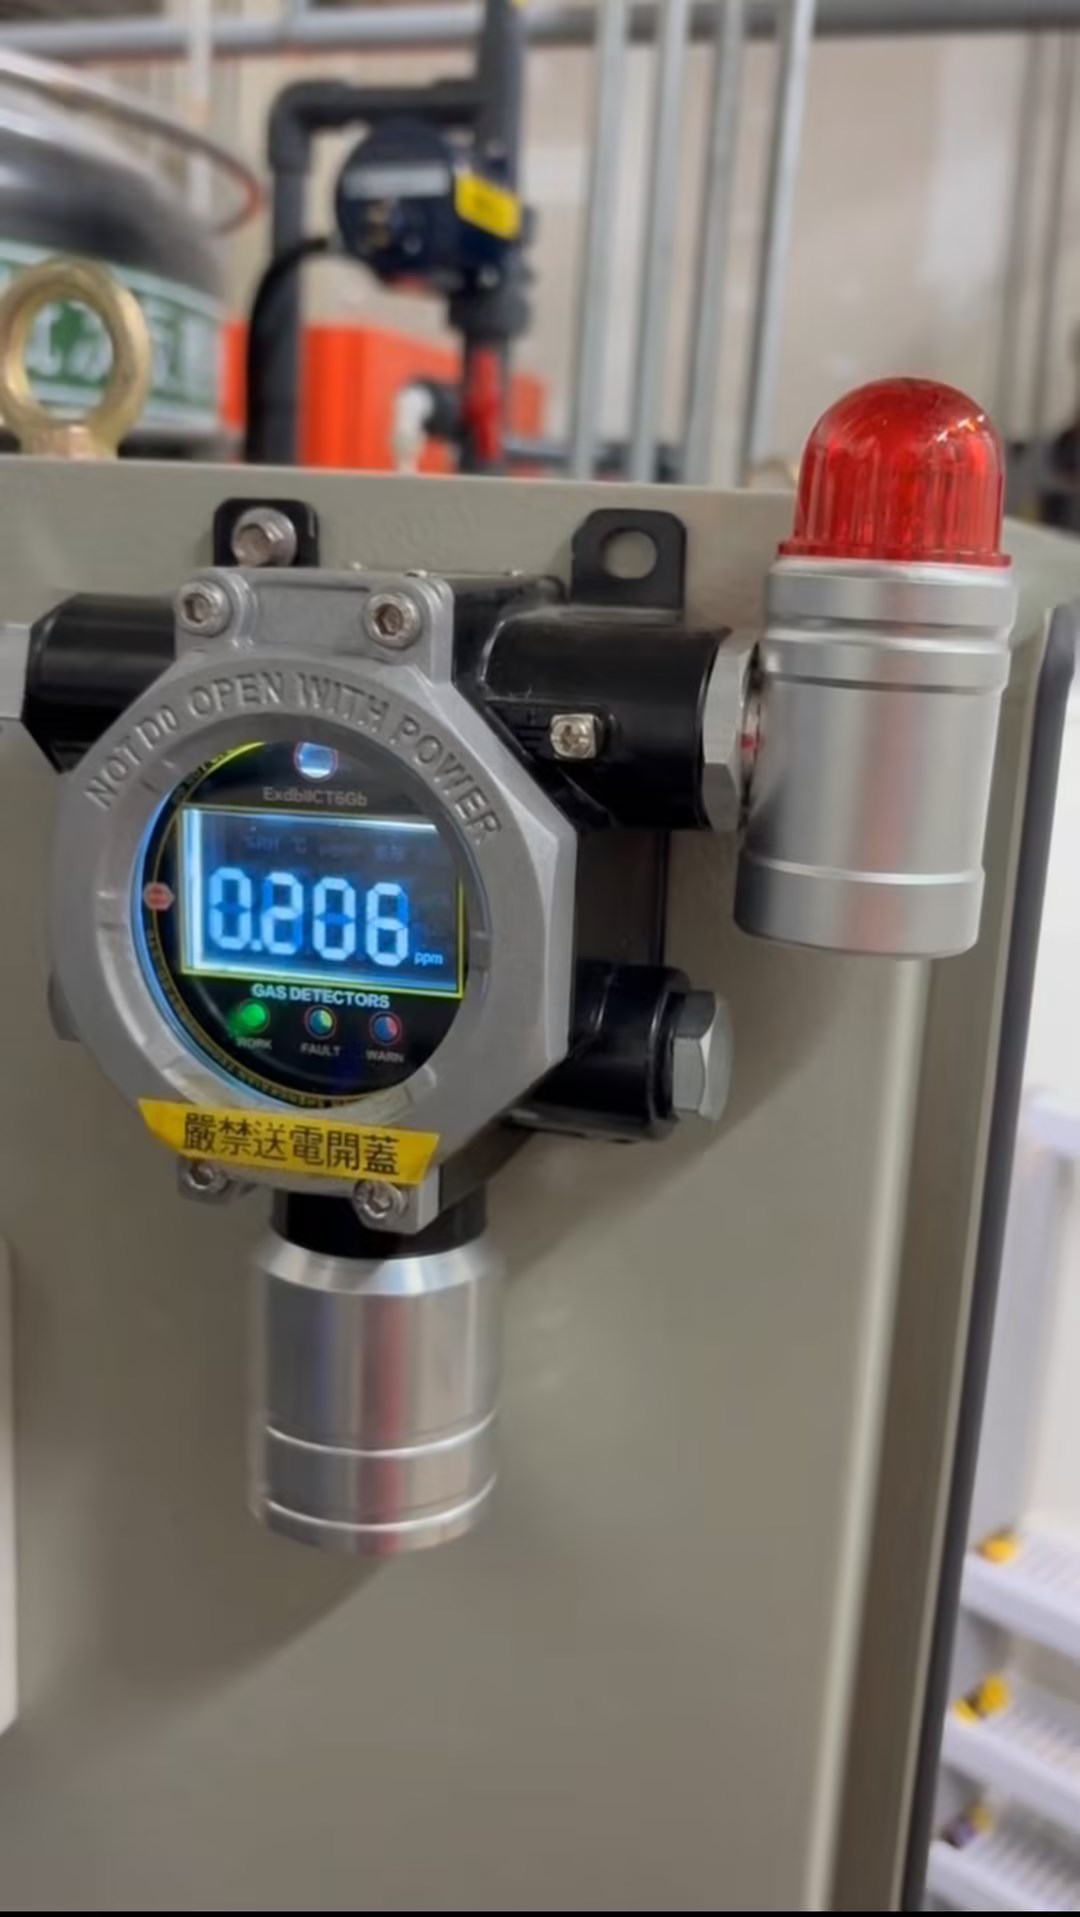
Device carries multiple generic signal output, compatibleDC24VPower supply, support4‑20mASimulation,RS485Digital signal, two bus, wireless transmission four modes of output, seamlessly connected industryPLC、DCSControl systems, gas alarm hosts, upper control platforms and cloud-connected platforms. Auto-activation, such as on-site real-time concentration displays, ultra-platform alerts, remote data uploads, historical data records, etc., can be achieved through on-site alerts, remote monitoring, wind-connection, power-connection disconnections, etc., and the enabling plant will be intelligent for gas monitoring, digitalization of controls, and automating security.
Environmental adaptation and storage performance
Industrial smelting waste gas concentration monitoring has the capability to work in a wide area, distinguishing between flammable and toxic gases in the exclusive working zone: Flammable gases are detected at temperatures-40℃~70℃The temperature for the toxicity gas detection is as follows:-10℃~55℃It is suitable for harsh industrial field environments such as cold and high temperatures. Work Humidity≤95%RH, without condensation, can operate steadily in damp, heavy dust conditions over a long period of time. Fit to atmospheric pressure86KPa~106KPaIntersections may be used at different altitudes and under different conditions. Easy storage conditions, storage temperature range-50℃~80℃storage humidity≤95%RHThe long-term preservation of the warehouse stock, the idle storage of equipment and the overall service life of the equipment can be up to three years, significantly reducing the cost of later replacement and transport for the enterprise.
VI. Application value
The composite gas detector, based on its core advantages of multi-principle compatibility detection, blast-proof dust, ultra-low power use, multi-sign compatibility, high environmental adaptability and long operational life, addressed the poor suitability, vulnerability, frequency of transport and limited range of scenes of the traditional single gas detector and covered the multi-industry core monitoring scene.Petrochemicals/Coal-chemical sites(b) Monitoring of flammable gases such as crude oil, natural gas, coal-chemical materials and toxic gas leaks such as hydrogen sulfide, carbon monoxide, and high-risk conditions in suitable plant areas, response workshops, storage tanks and loading stations;Paint/Lithium new energy scene• Explicit monitoring of volatile paint gases, organic solvents, lithium electrolyte volatile flammable gases, suitable for dustless workshops, dry production lines, storage workshops;Municipalities/Environment sceneFor sewage treatment plants, underground corridors, tunnels, real-time monitoring of harmful gases such as biogas, hydrogen sulfide and avoidance of security hazards in closed space;Pharmaceuticals/Food processing scenesMonitoring of gases such as alcohol, organic solvents and ammonia for medical purposes to meet the monitoring needs for safe production in cleaner workshops;Gas/Mining• Sites such as gas-resilient pressure stations, pipeline networks, metallurgy mines, and real-time protection against the risk of flammable and toxic gas leaks. Equipment allows for the full monitoring of the risk of flammable, toxic and hazardous gas leaks from industrial sites, early warning of hazards, avoidance of explosions, poisonings, etc., and helps enterprises to improve their safety monitoring systems, comply with standards of production and effectively reduce safety risks and transport costs, which are the core security monitoring equipment necessary for industrial endangered sites and high-risk scenarios.
Detailed technical parameters for equipment
| Parameter Item |
Technical specifications |
| Test principles |
Catalytic combustion, electrochemical, semiconductor, infrared |
| Detection of gases/Countpoint |
Measurement range, alarm point: see device signs |
| Electricity/Signal Output |
DC24V;4-20mA、RS485Two buss, wireless. |
| Full power. |
1.2W |
| Working temperature |
flammable gas:-40℃~70℃;toxic gases:-10℃~55℃ |
| Work Humidity |
≤95%RH(No Condensing) |
| Atmospheric pressure |
86KPa~106KPa |
| Insulation. |
Normal≥100MΩ;94%RHHigh-wet environment≥1MΩ |
| Working methods |
24Hours of continuous online monitoring |
| Explosive-proof mode |
Detonation |
| Sampling method |
Proliferation |
| Storage temperature |
-50℃~80℃ |
| Storage humidity |
≤95%RH |
| Useful life of equipment |
Three years. |
Main Application Areas
- Smelting Industry — Continuous monitoring of nitrogen monoxide levels in smelting furnaces and workshops to ensure worker safety and compliance with emission regulations.
- Industrial Safety — Early detection of toxic NO gas leaks in industrial plants, triggering alarms and automatic ventilation systems to prevent accidents.
- Environmental Monitoring — Used in environmental monitoring stations to measure NO concentrations in ambient air, aiding in pollution control and assessment.
- Chemical Processing — Monitoring nitrogen monoxide in chemical reactors and storage areas to prevent hazardous exposure and ensure process safety.
Keywords:nitrogen oxide detector, NO gas monitor, smelting gas detection, industrial gas sensor, electrochemical NO sensor, fixed gas detector, real-time gas monitoring, safety alarm system