Product Introduction
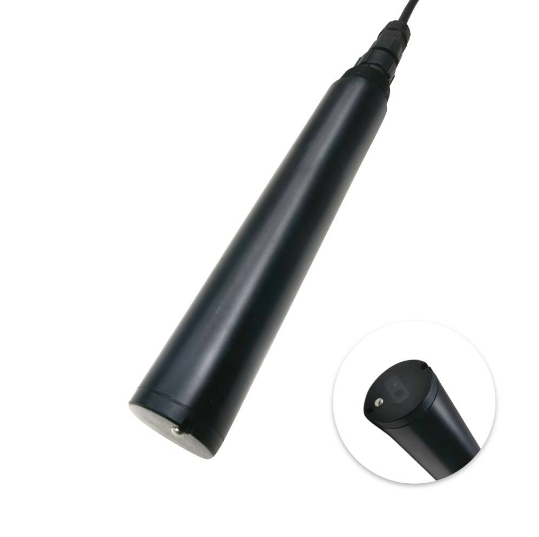
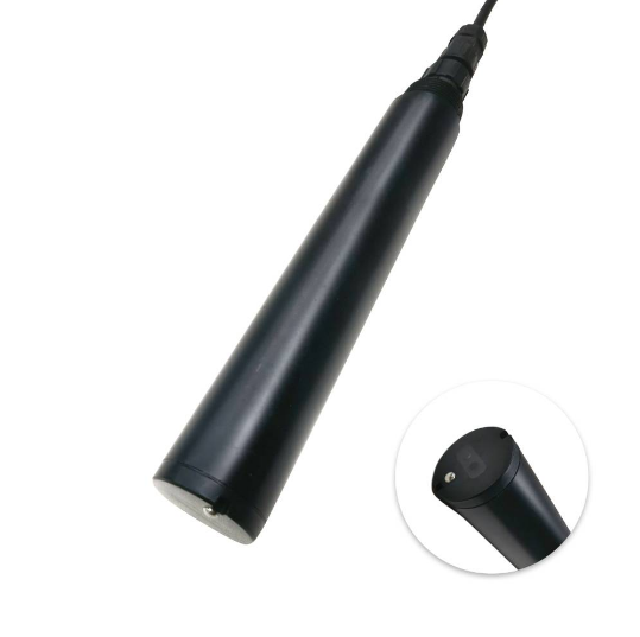
Online river turbidity monitoring sensor
1. Product overview of the online river turbidity monitoring sensor
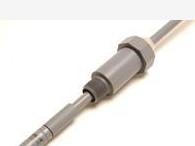
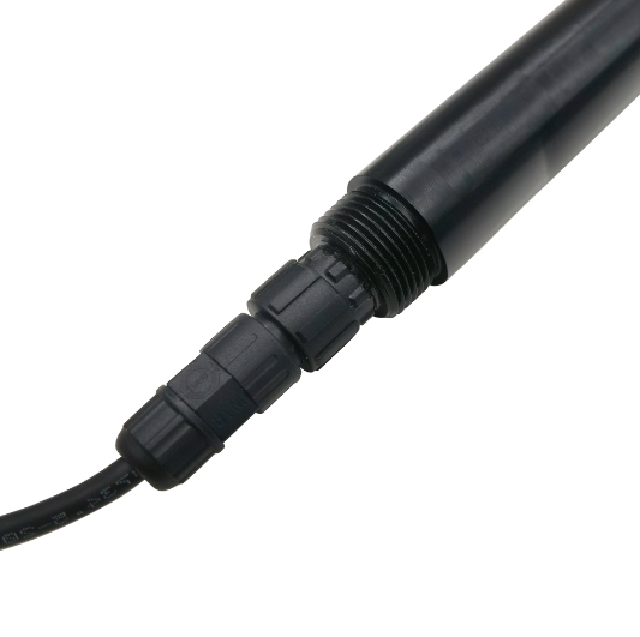
This industrial online turbidity sensor uses optical scattering detection principles, employing infrared light scattering to precisely capture light scattering signals from suspended particles, sediment, algae, and colloidal impurities in water. Equipped with built-in temperature compensation and digital processing chips, it enables long-term continuous online monitoring of water turbidity. The entire unit features a corrosion-resistant cylindrical housing with high-seal waterproof design, resisting water corrosion and environmental interference, and can operate stably in various complex water quality conditions, collecting and transmitting turbidity data in real time, providing reliable data support for water purification, pollution control, and water environment management. Widely used in tap water supply, sewage treatment, surface water ecological monitoring, aquaculture, and industrial production water.
2. Working principle of the online river turbidity monitoring sensor
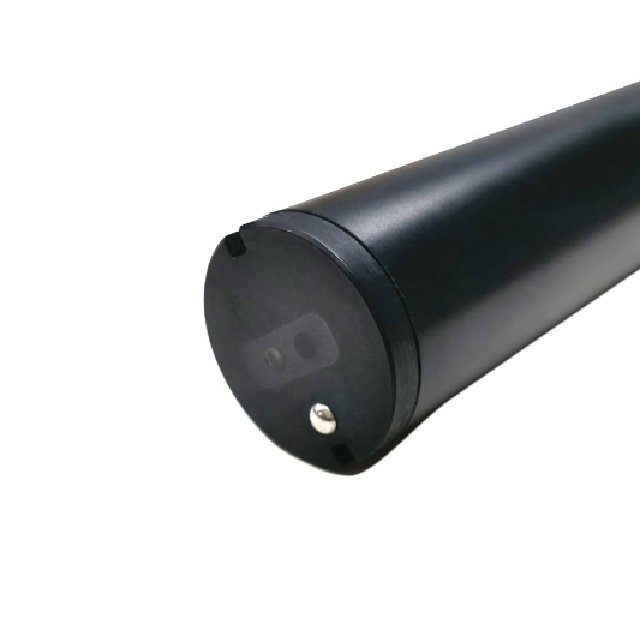
The infrared light source inside the sensor emits a beam into the water, where suspended particles cause light scattering, and the photoelectric receiving component collects the scattered light intensity. The more suspended impurities in the water, the higher the scattered light value. The device converts the photoelectric signal to output the corresponding turbidity value; integrated temperature compensation algorithm eliminates errors caused by water temperature changes in optical measurements, ensuring stable and accurate detection results in different environments.
3. Core advantages of the online river turbidity monitoring sensor
- Optical non-destructive detectionNo chemical reagents required, no secondary pollution, lower maintenance costs in the long run;
- High-precision detection solution, rapid measurement response, real-time data output;
- Anti-corrosion sealed body, supports long-term immersion installation, suitable for harsh water qualities such as sewage and high-sediment surface water;
- Standardized RS485 Digital signal output, can interface with data collectors,PLCOnline monitoring platform for easy system integration;
- Comes with self-cleaning adapter interface, can be paired with automatic wiper device to reduce sludge adhesion and lower manual cleaning frequency;
- Flexible installation forms, adaptable to immersion, pipeline, and pool wall bracket types.
4. Main application scenarios
✅ Monitoring turbidity of raw water, sedimentation tank, and effluent in water plants to ensure water supply safety; ✅
Inlet and outlet water monitoring of municipal sewage treatment plants to assess the effectiveness of flocculation and sedimentation processes; ✅
Ecological monitoring of surface water environments such as rivers, lakes, and reservoirs; ✅
Aquaculture water quality control to reduce the impact of suspended impurities on aquatic organisms; ✅
Monitoring of production wastewater and circulating water quality in chemical, electroplating, and food processing industries.
5. Basic usage and maintenance points
During installation, immerse the optical detection window in water, avoiding areas with strong direct water flow and impacts from large debris. Regularly inspect and clean the optical lens to remove attached sludge and biological films, preventing light path obstruction that could cause data deviations; before long-term storage, rinse the probe clean and store it in a dry, dark environment. The device supports on-site rapid calibration, is simple and convenient to operate, and meets industrial long-term automated monitoring needs.
Main Application Areas
- River and Surface Water Monitoring — Continuous monitoring of turbidity in rivers, lakes, and reservoirs to assess water quality and detect pollution events.
- Drinking Water Treatment — Real-time turbidity measurement in raw and treated water to ensure compliance with safety standards and optimize coagulation and filtration processes.
- Wastewater Treatment — Monitoring turbidity in influent and effluent to evaluate treatment efficiency and control discharge quality.
- Industrial Process Water — Monitoring turbidity in cooling water, boiler feed water, and other industrial process waters to prevent scaling and fouling.
Keywords:online turbidity sensor, river water monitoring, water quality sensor, industrial turbidity sensor, suspended solids sensor, wastewater turbidity sensor, drinking water turbidity, real-time turbidity measurement