Product Introduction
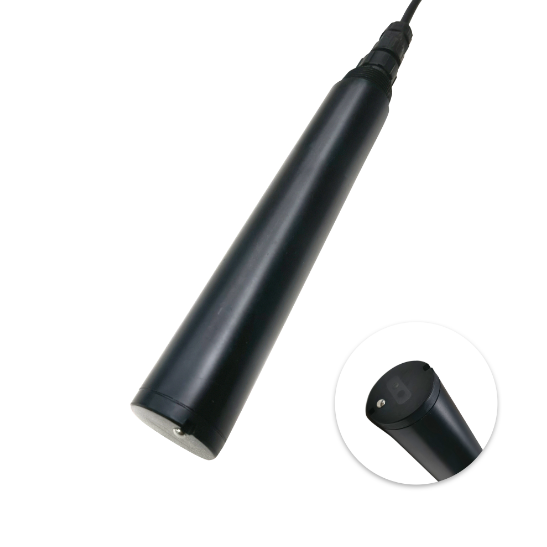
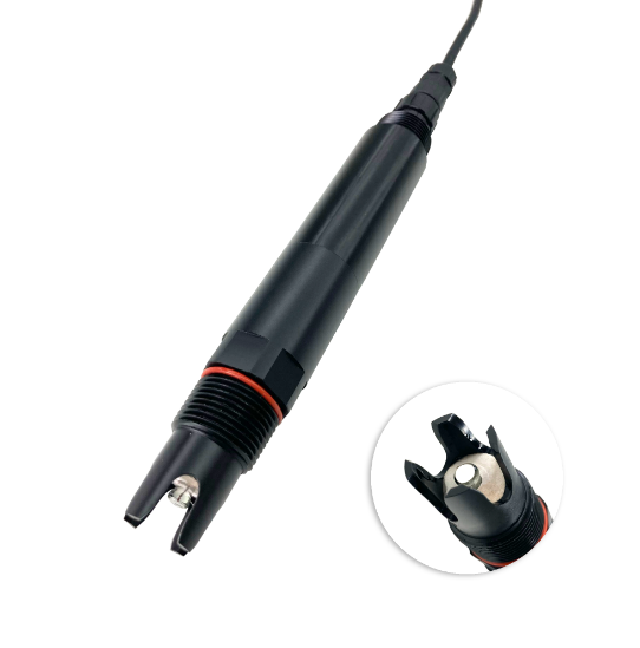
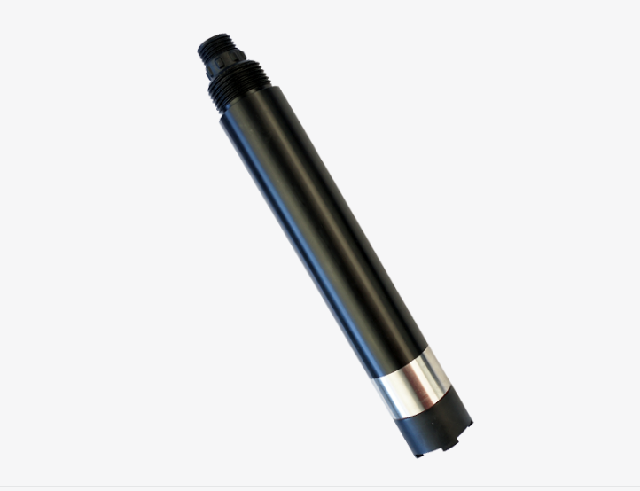
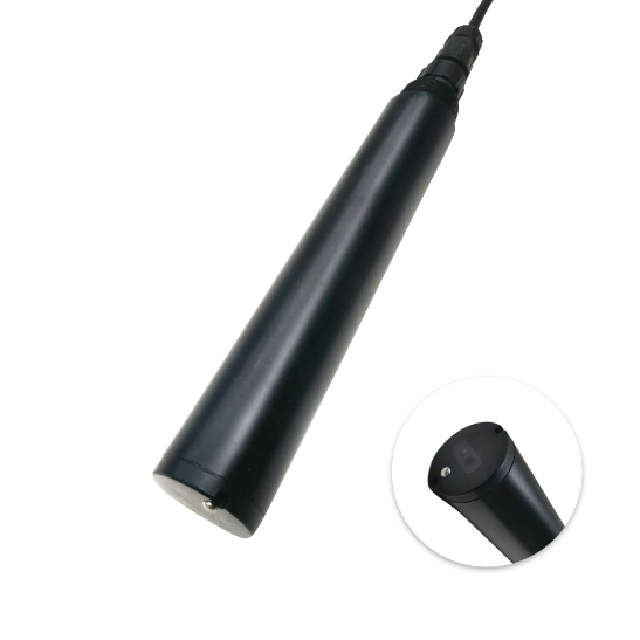
Online turbidity transmitter for groundwater well monitoring
一、产品概述
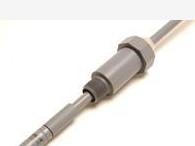
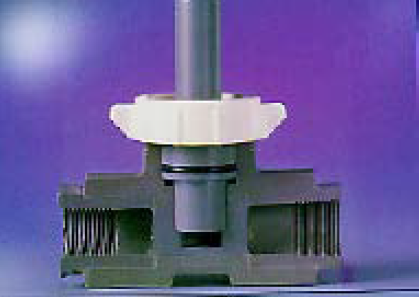
The online turbidity transmitter for groundwater well monitoring is aIndustrial-grade online real-time water quality monitoring equipment, integrates high-precision sensing detection, automatic temperature compensation, and digital signal processing technology, enabling long-term, continuous, and stable monitoring of key water quality indicators. The equipment has a compact structure, high protection rating, and strong anti-interference capability, suitable for various complex water environments, achieving real-time collection, accurate analysis, and remote transmission of water quality data. Widely used in environmental monitoring, wastewater treatment, industrial processes, rivers and reservoirs, aquaculture, and drinking water supply scenarios.
2. Detection Parameters
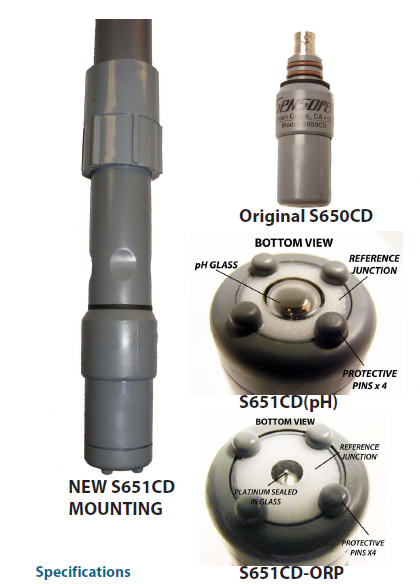
The online turbidity transmitter for groundwater well monitoring can be configured with single-parameter or multi-parameter integrated detection as needed, with routine monitoring indicators including:pH/ORP, dissolved oxygen, conductivity, turbidity, water temperature, ammonia nitrogen, residual chlorine,COD, suspended solidsand other core water quality parameters, meeting water quality control standards across different industries.
3. Core Advantages
- High-precision stable detection: Equipped with imported sensing core, built-in temperature compensation algorithm, effectively offsetting detection errors caused by environmental water temperature fluctuations, providing accurate and repeatable measurement data.
- Long-term online maintenance-free: Optimized waterproof and anti-fouling structure, resistant to sediment and algae attachment, supports long-term submerged online monitoring, significantly reducing manual calibration and maintenance frequency.
- Industrial-grade stable output: StandardRS485Digital interface, supportsModbusUniversal protocol, stable data transmission, strong compatibility, direct integrationPLCIndustrial control systems, IoT monitoring platforms
- Strong protection, wide adaptability: High-sealing waterproof design of the whole machine, resistant to high and low temperatures, corrosion-resistant, suitable for complex conditions such as wastewater, surface water, industrial circulating water, and aquaculture water bodies.
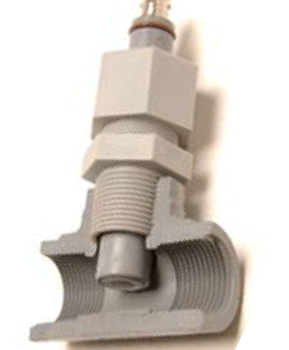
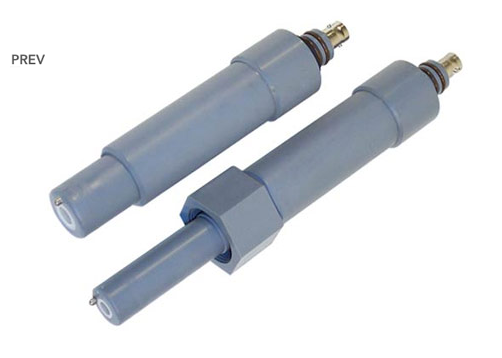
- Simple and flexible installation: Supports immersion, pipeline, and wall-mounted installation methods, plug-and-play, easy commissioning, suitable for upgrading new and existing monitoring systems.
4. Application Scenarios
- Online monitoring of municipal wastewater and industrial wastewater treatment
- Ecological water quality monitoring for rivers, lakes, reservoirs, and groundwater
- Real-time control of water quality in water plants and secondary water supply
- Water quality monitoring for aquaculture and swimming pool water bodies
- Industrial circulating water, pure water, process water monitoring
5. Product Value
The online turbidity transmitter for groundwater well monitoring equipment enables water quality2424-hour unattended real-time monitoring, timely capture abnormal water quality fluctuations, early warning of exceedance risks, helping enterprises comply with discharge regulations, refined water treatment control, and intelligent water environment supervision, effectively reducing operation and maintenance costs and improving the intelligence level of water quality management.
6. Full Parameter Selection Table
Covers mainstream water quality monitoring parameters on the market, suitable for full-scenario selection in wastewater, tap water, surface water, aquaculture water bodies, etc. Core technical parameters are as follows:
| Monitoring parameters |
Measurement range |
Measurement accuracy |
Core configuration |
| pH/ORP |
0~14pH / -2000~+2000mV |
±0.02pH / ±1mV |
Automatic temperature compensation, anti-interference |
| Dissolved Oxygen |
0~20mg/L |
±0.2mg/L |
Fluorescence method detection, no membrane covering required |
| Conductivity |
0~200mS/cm |
±1%FS |
Wide range adaptation, automatic temperature compensation |
| Turbidity |
0~1000NTU |
±3%FS |
Optical detection, built-in anti-fouling brush |
| Water temperature |
-10~60℃ |
±0.5℃ |
Global temperature compensation adaptation |
| Residual chlorine |
0~10mg/L |
±0.05mg/L |
Suitable for drinking water and swimming pool water monitoring |
| COD |
0~100mg/L |
±3%FS |
UV spectroscopy method, reagent-free detection |
| Ammonia nitrogen |
0~50mg/L |
±2%FS |
Dedicated detection for industrial wastewater |
| Suspended solids |
0~5000mg/L |
±3%FS |
Suitable for sludge and wastewater conditions |
| Salinity |
0~70PPT |
±1%FS |
Seawater/Dedicated for saline water, temperature and salinity compensation |
| Chlorophyll |
0~200μg/L |
±2%FS |
Fluorescence method detection, dedicated to algae monitoring |
| Color |
0~500PCU |
±3%FS |
Color monitoring for pure water and tap water |
| Oil in water |
0~100mg/L |
±2%FS |
UV fluorescence method, industrial water oil contamination monitoring |
| Transparency |
0~1000cm |
±5cm |
Ecological monitoring of rivers, lakes, and surface water |
General electrical and whole-machine parameters (common to all sensor series)
- Supply voltage: StandardDC12V~24VWide voltage power supply, compatible with industrial DC power systems, supports voltage fluctuation adaptation, not prone to tripping or crashing
- 信号输出: StandardRS485Digital signal, long transmission distance, strong anti-interference, supports parallel networking of multiple sensors
- Communication protocol: StandardModbus-RTUUniversal protocol, extremely strong compatibility, direct integrationPLCIndustrial PCs, industrial gateways, environmental monitoring platforms, IoT cloud platforms
- 防护等级整机IP68Highest waterproof and dustproof rating, can be fully submerged underwater for long-term operation, waterproof, moisture-proof, corrosion-resistant, suitable for outdoor, underwater, and humid harsh conditions
- Working environment temperature:0℃~45℃, supports low-temperature and normal-temperature routine water body monitoring, adaptable to most municipal, industrial, and ecological water environment scenarios
- Storage temperature:-20℃~60℃, equipment is not easily damaged during idle storage and transportation
- 响应速度: Routine detection response time≤1sFast data updates, real-time capture of water quality dynamic changes
- 设备材质: Main body made of anti-corrosion engineering materials/Stainless steel material, acid and alkali resistant, scale resistant, seawater corrosion resistant, long service life
- 安装方式: Supports immersion, pipeline, wall-mounted, and submerged installation methods, suitable for upgrading new and existing monitoring systems
- Operation and maintenance characteristics: Built-in automatic temperature compensation and data filtering algorithm, high stability, long-term online operation without frequent calibration, low maintenance cost
Main Application Areas
- Groundwater Well Monitoring — Continuous real-time turbidity measurement in groundwater wells to detect contamination and ensure water quality.
- Environmental Monitoring — Used in rivers, lakes, and reservoirs to monitor turbidity levels for environmental protection and research.
- Water Treatment Plants — Monitors influent and effluent turbidity to optimize coagulation, filtration, and disinfection processes.
- Industrial Process Water — Ensures quality of process water in industries such as food and beverage, pharmaceuticals, and manufacturing.
Keywords:online turbidity transmitter, groundwater turbidity sensor, water quality monitoring, AMT-300, turbidity analyzer, well water monitoring, real-time turbidity measurement, industrial water quality sensor