Product Introduction
I. Product Introduction of Grain Near-Infrared Online Moisture Detector for Conveyor Belt
The near-infrared online moisture meter is aNon-contact, non-destructive, continuous real-time moisture content detection equipment, based on the principle of near-infrared spectral absorption-diffuse reflectance of water molecules. The probe is installed above belt conveyors, chutes, or dryer discharge outlets. No sampling or material contact is required, with millisecond-level real-time moisture reading. It can directly interface with PLC and DCS control systems to achieve closed-loop automatic control of drying and humidification processes, eliminating the lag of offline laboratory analysis, stabilizing product moisture content, and reducing drying energy consumption. It is a dedicated instrument for intelligent moisture management in industrial production lines.
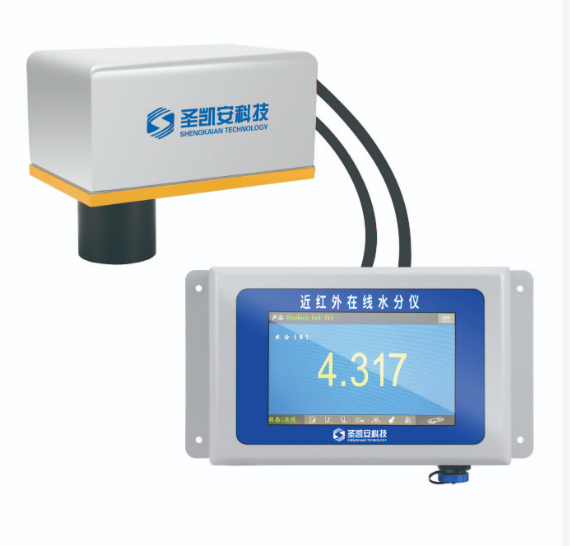
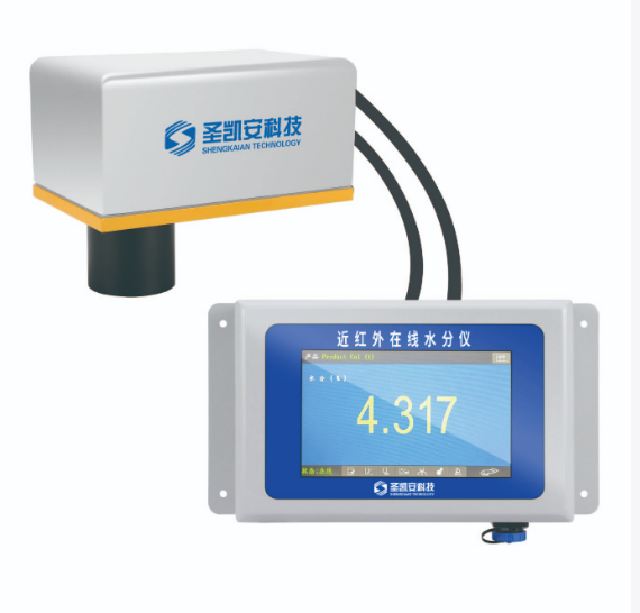
The entire equipment consists ofDetection probe + control host + signal cableComposed of three parts; supports multi-material curve storage, temperature and dust compensation, adapting to harsh workshop conditions such as dust, high temperature, and high humidity, with 24-hour continuous operation.
Core principle: Water molecules absorb specific bands of near-infrared light. The instrument emits a light source to irradiate the material surface, receives reflected light signals, and calculates the material moisture content value through built-in algorithm models. Detection processNo damage to materials, no consumables.
II. Main Functions of Grain Near-Infrared Online Moisture Detector for Conveyor Belt
- Real-time continuous detection: Continuous measurement of dynamic materials on the production line, real-time display of moisture content, fast response speed, no detection delay
- Non-contact non-destructive measurement: Probe does not touch material, no sample loss, no material contamination
- Multi-material curve storage: Built-in multiple calibration curves, one-click switching between different materials, one machine for multiple uses
- Intelligent compensation algorithm: Temperature compensation, dust compensation, material color/thickness compensation, reducing environmental interference, stable measurement
- Real-time data output: 4-20mA analog, RS485-Modbus digital signal, interfacing with PLC, industrial control screens, and host computer systems. Can be linked to dryers for automatic adjustment of drying parameters, enabling closed-loop control of production line moisture.
- Data storage and traceability: Historical moisture data saved, report export, production quality records traceable
- Over-limit alarm: Sound and light alarm when moisture is above/below the set threshold, timely warning of non-conforming materials
- Touch operation: Host color touch screen, parameter settings, curve calibration, and real-time data viewing are simple and convenient
- Remote monitoring(Optional): Supports IoT cloud platform, remote viewing of production line moisture data via computer or mobile phone
- No frequent maintenance required: Probe window comes with purge interface (optional), reducing dust adhesion and cleaning frequency
III. Technical Parameters of Grain Near-Infrared Online Moisture Detector for Conveyor Belt (General Standard Version, Modifiable as Needed)
Table
| Item | Parameter specifications |
|---|---|
| Measurement principle | Near-infrared diffuse reflectance spectroscopy |
| Measurement moisture range | 0-60% (customizable range 0-100% based on material) |
| Measurement accuracy | ±0.1% to ±0.5% (affected by material type and surface condition) |
| 分辨率 | 0.01% |
| Repeatability | ≤±0.2% |
| Response time | Millisecond level, 0-60s adjustable filtering time |
| Measurement spot diameter | Φ60‑90mm |
| Standard measurement distance | 250mm±100mm (installation height adjustable) |
| 信号输出 | 4‑20mA、RS485(Modbus‑RTU) |
| Calibration curves | Up to 100 material curve storage |
| Display screen | 7-inch industrial touch screen |
| Probe protection level | IP65 |
| Working environment temperature | 0℃‑50℃ |
| Ambient humidity | 5-90% RH, non-condensing |
| Power supply | AC220V 50Hz |
| 安装方式 | Bracket installation, above belt/chute |
| Explosion-proof version | Customizable explosion-proof type (Ex) |
IV. Industry Applications and Applicable Materials of Grain Near-Infrared Online Moisture Detector for Conveyor Belt
1. Grain and feed industry
Wheat, corn, rice, flour, soybean meal, pellet feed, premix, straw, etc.; moisture monitoring in drying sections and belt conveyors to stabilize finished feed moisture and reduce mold risk.
2. Lithium battery / new energy materials
Lithium iron phosphate, lithium carbonate, graphite powder, anode materials, ceramic powder; online moisture control of dried powder discharge to ensure battery material quality.
3. Chemical powder industry
Fertilizer, urea, calcium carbonate, titanium dioxide, inorganic salts, resin powder, pigments; real-time moisture monitoring on production lines to reduce caking.
4. Food processing
Starch, white sugar, milk powder, tea, nuts, seasonings, fruit and vegetable powders; non-destructive testing to ensure food safety.
5. Tobacco industry
Tobacco leaves, cut tobacco, redrying production lines; closed-loop moisture control for humidification and drying processes.
6. Building materials, mining, and coal
Coal, limestone, slag, sand, clay; moisture detection on belt conveyors to optimize drying and calcination processes.
7. Papermaking and wood
Online moisture monitoring for wood chips, sawdust, pulp, cardboard, and paper coating.
8. Textile
Online moisture detection for yarn, fabric, and non-woven fabrics.
Main Application Areas
- Grain Processing — Monitor moisture levels in grains like wheat, corn, and rice during processing to ensure optimal storage and milling conditions.
- Agriculture — Used in harvesting and post-harvest handling to quickly assess grain moisture for proper drying and storage decisions.
- Food Industry — Ensures consistent moisture content in raw materials for food production, improving product quality and shelf life.
- Feed Manufacturing — Controls moisture in feed ingredients to maintain nutritional value and prevent spoilage during storage.
Keywords:grain moisture analyzer, online moisture detector, NIR moisture sensor, conveyor belt moisture meter, grain moisture sensor, industrial moisture analyzer, AMT-SFY-HW, PrimeIndu