Product Introduction
I. Industrial Explosion-proof Alarm, Real-time Gas Leak Monitoring Product Overview
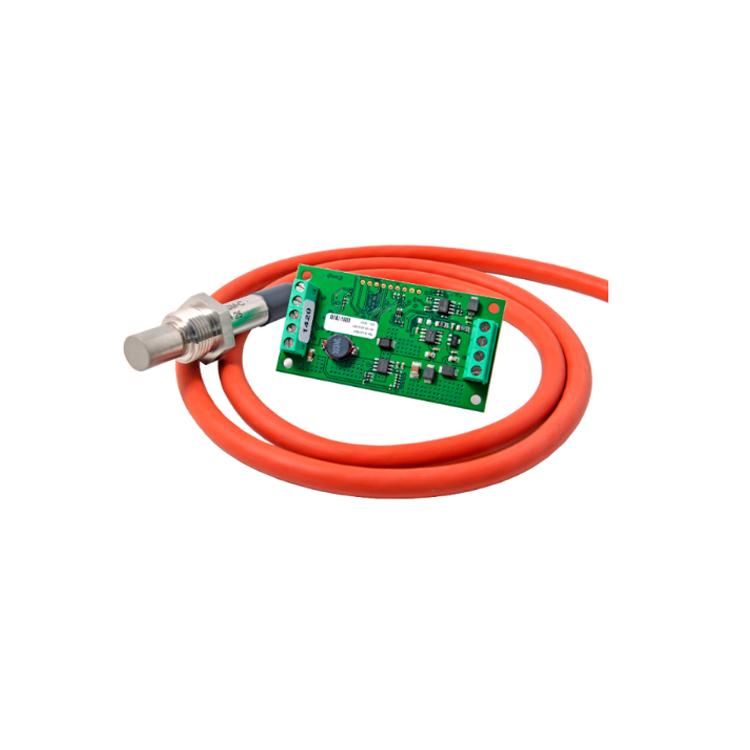
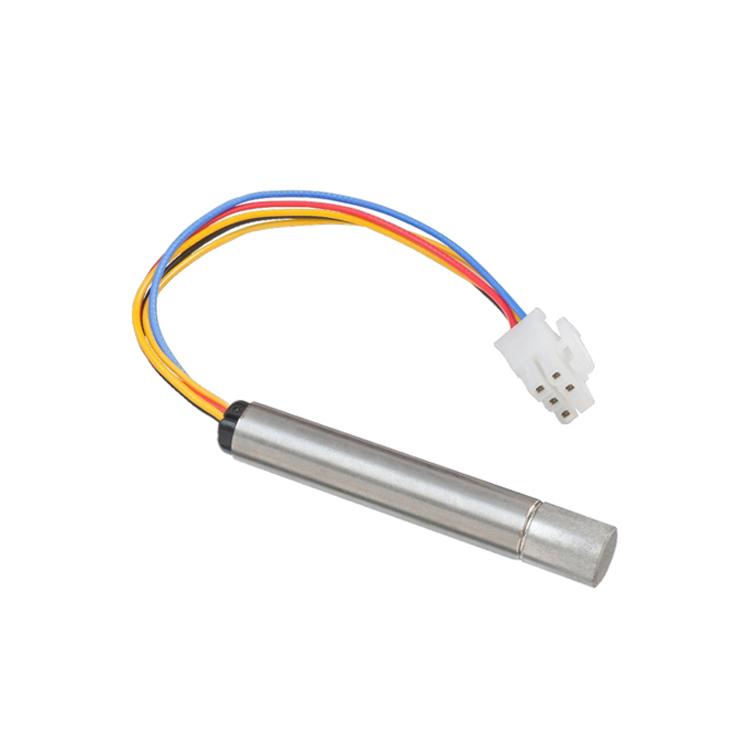
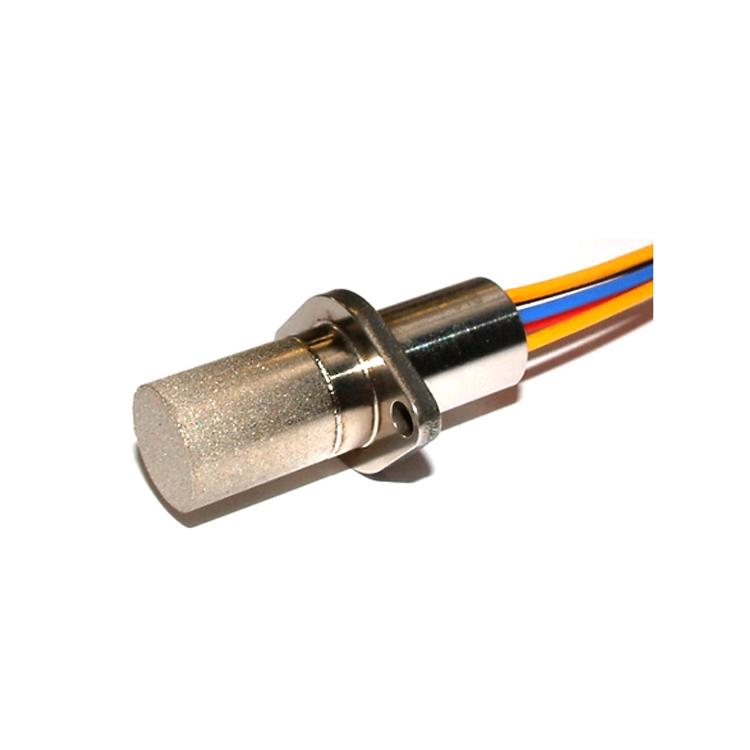
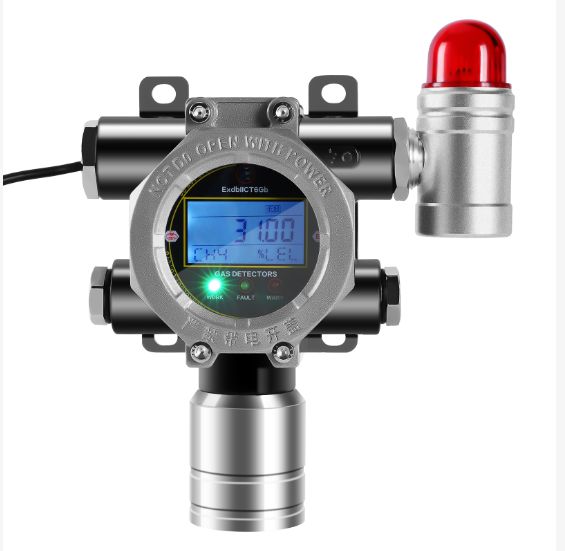
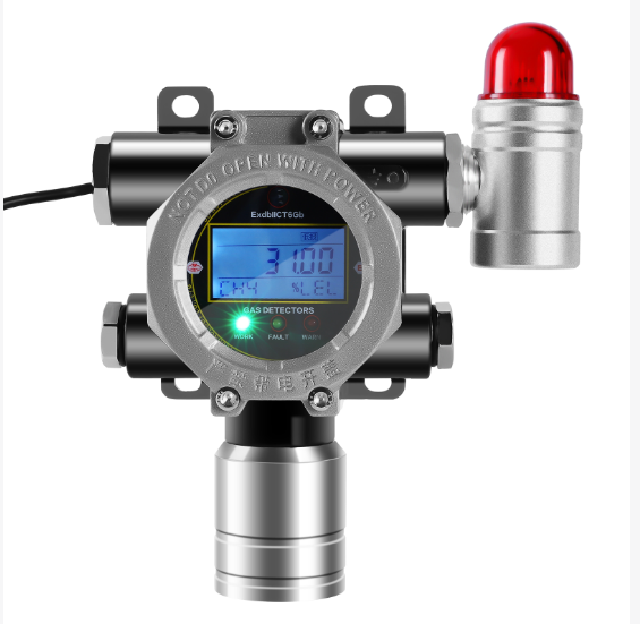
The combustible gas alarm consists of a detector and an alarm controller, and is an industrial explosion-proof safety monitoring device. It detects the concentration of combustible gases such as natural gas, liquefied gas, methane, and propane in real time. When the gas concentration reaches the preset alarm threshold, it automatically triggers audible and visual alarms and can link with solenoid valves, exhaust fans, and other equipment to quickly eliminate explosion hazards. Widely used in chemical plants, gas stations, boiler rooms, restaurant kitchens, coating workshops, and tank farms, meeting safety production acceptance requirements.
II. Industrial Explosion-proof Alarm, Real-time Gas Leak Monitoring Product Introduction
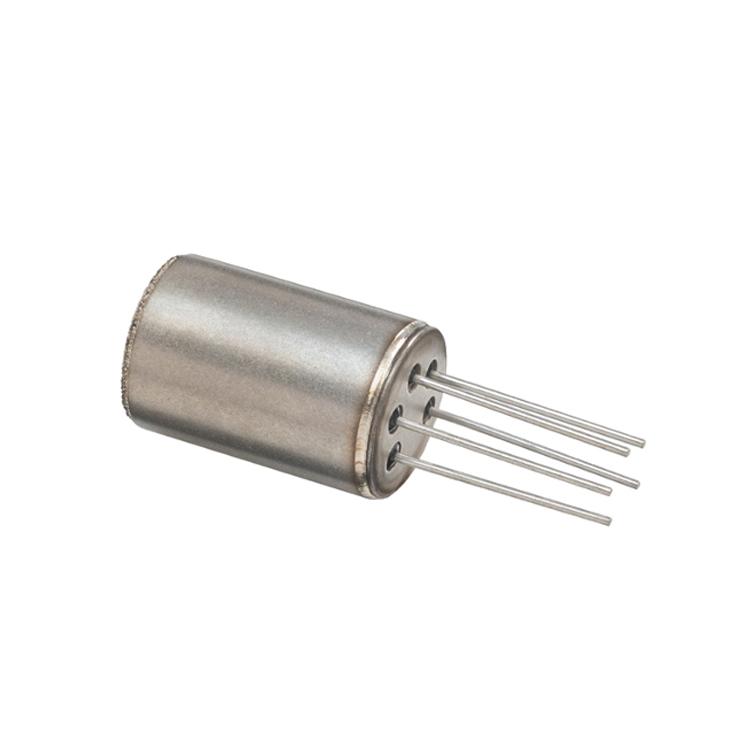
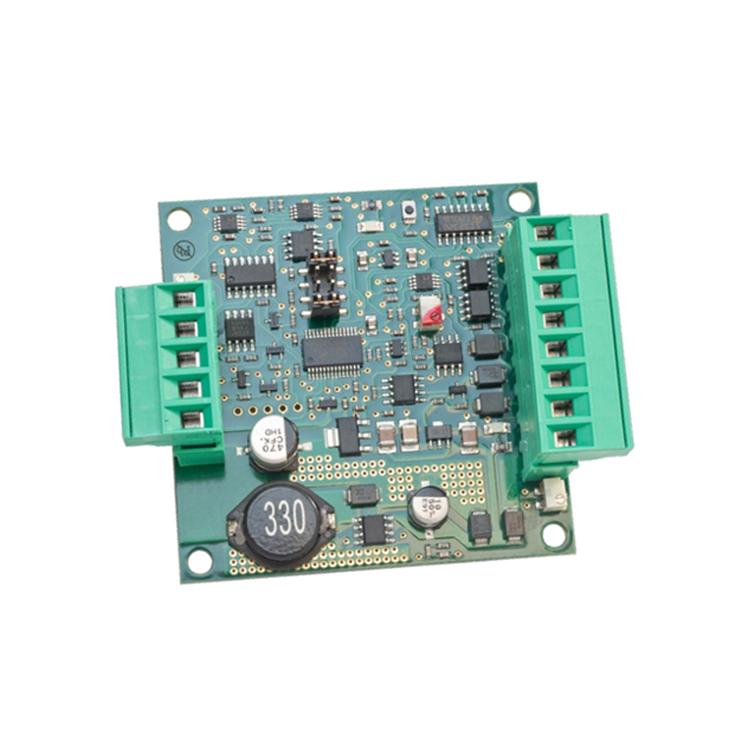
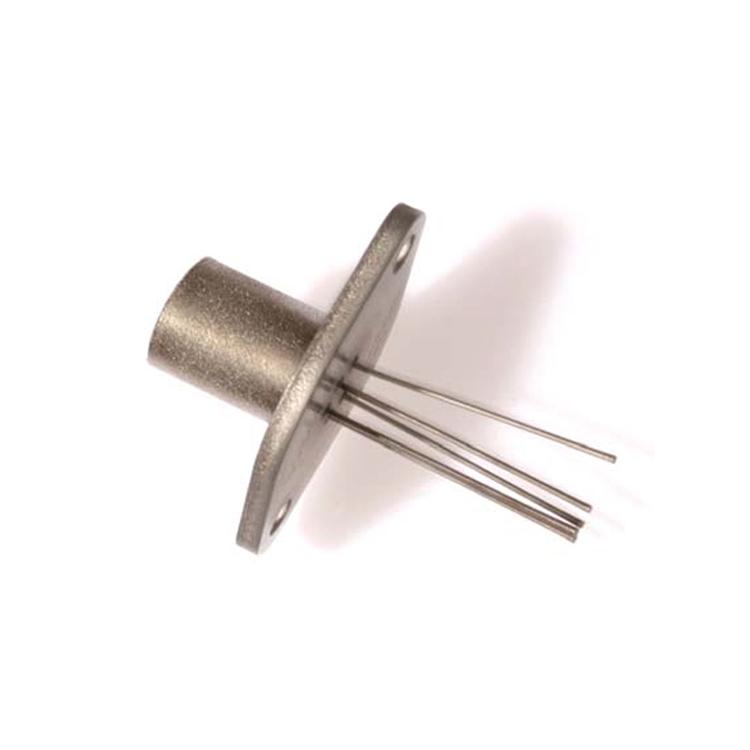
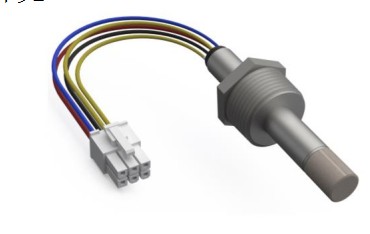
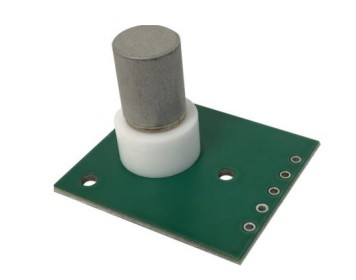
The complete system includes现场探测器withAlarm hostTwo major units. The detector is installed in locations where gas tends to accumulate, collecting gas concentration signals in real time and transmitting them to the alarm host via cable; the host centrally displays the concentration at each monitoring point and saves alarm records. The equipment uses an explosion-proof enclosure, adaptable to harsh working conditions such as dust and humidity. The fixed model provides 24-hour uninterrupted online monitoring; the portable model is used for on-site inspection and leak detection. The product has explosion-proof certification, supports engineering installation, prevents fire and explosion accidents caused by combustible gas leaks, and ensures the safety of plant equipment and personnel.
III. Industrial Explosion-proof Alarm, Real-time Gas Leak Monitoring Features
- High-sensitivity catalytic combustion sensor, fast response, accurate combustible gas concentration detection
- Two-level alarm settings, pre-alarm + high alarm, audible and visual alerts simultaneously when exceeding limits
- Explosion-proof structural design, IP65 protection, waterproof and dustproof, suitable for complex industrial environments
- Digital screen displays real-time concentration values, intuitive readings, supports multi-point centralized monitoring
- Supports linkage with exhaust ventilation and gas solenoid valves, automatically cutting off gas source and starting ventilation
- Strong signal anti-interference capability, effectively reducing false alarm and missed alarm probability
- Alarm data storage and recording, convenient for safety inspections and project acceptance review
- Easy installation and commissioning, low subsequent maintenance workload, long sensor service life
- Multiple gas options: methane, liquefied petroleum gas, propane, ethanol, etc.
- 4-20mA/RS485 signal output, can be connected to PLC, DCS industrial control systems
IV. Industrial Explosion-proof Alarm, Real-time Gas Leak Monitoring Technical Parameters
Table
| Item | Parameter |
|---|---|
| Detection gas | Combustible gases such as methane, liquefied petroleum gas, propane, ethanol, etc. |
| Detection principle | Catalytic combustion type sensor |
| Measurement Range | 0~100%LEL |
| 分辨率 | 0.1%LEL |
| Response time | ≤30s |
| Alarm method | Audible and visual alarm, two-level adjustable alarm |
| Explosion-proof grade | Ex d IIC T6 Gb |
| 防护等级 | IP65 |
| 工作电压 | Detector DC24V; alarm host AC220V |
| 信号输出 | 4-20mA / RS485 |
| 工作温度 | -20℃~+50℃ |
| Relative humidity | 10%~95% RH (non-condensing) |
| Transmission distance | ≤1000m (shielded cable) |
| 安装方式 | Wall-mounted fixed installation |
Main Application Areas
- Oil and Gas Industry — Continuous gas leak monitoring on offshore platforms, refineries, and pipelines to prevent accidents.
- Chemical Plants — Detection of toxic and flammable gas leaks in chemical processing and storage areas.
- Mining Operations — Monitoring methane and other hazardous gases in underground mines for worker safety.
- Pharmaceutical Manufacturing — Ensuring safe environments by detecting solvent vapors and other flammable gases.
- Wastewater Treatment — Monitoring hydrogen sulfide and methane in treatment facilities to protect personnel.
Keywords:explosion-proof alarm, gas leak detector, industrial gas monitor, real-time gas monitoring, hazardous area alarm, gas leak alarm, explosion-proof sensor, industrial safety alarm