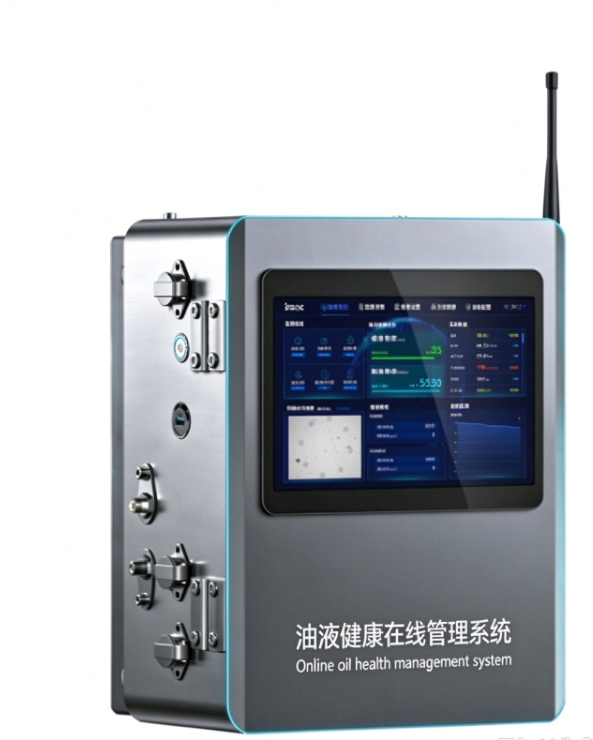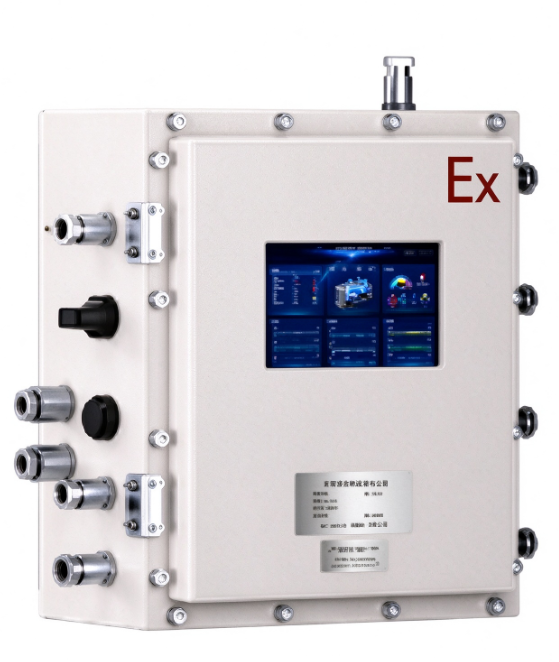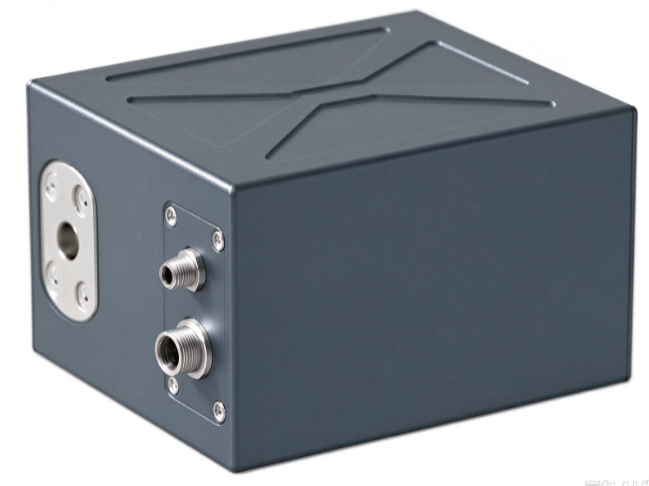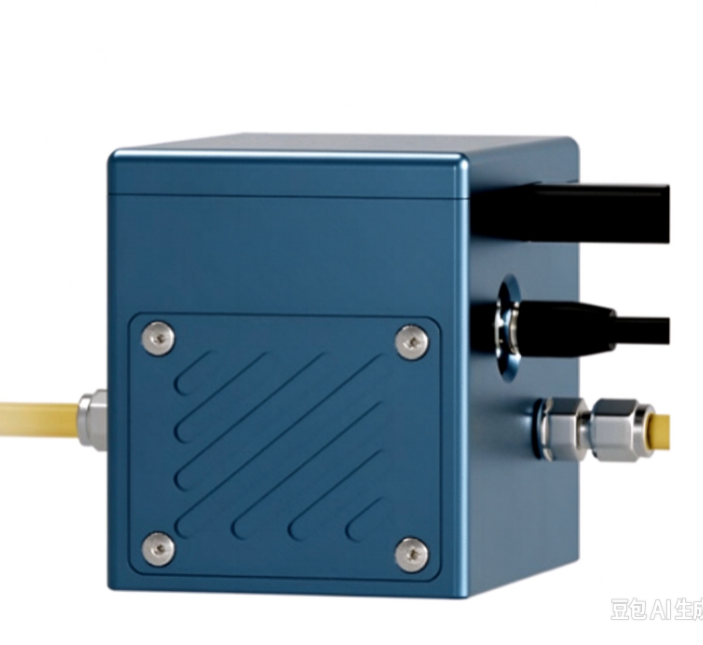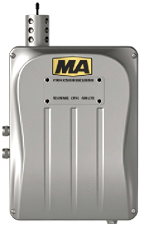
Mine intrinsically safe online oil monitoring instrument - SKA YJY12
| Specifications and indicators | |
|---|---|
| Technical Specifications | Viscosity, density, temperature, oil quality, water content (free water), contamination level, metal wear, water content (dissolved water), saturation |
| Explosion-proof enclosure | alloy |
| Circulation Mode | Equipped with explosion-proof pump circulation/differential pressure circulation |
| Remote monitoring | 4G/5G/WIFI/Ethernet/RS485/232 optional |
| Cloud Platform | WeChat Mini Program/Web Portal |
| Sensor Range | |
|---|---|
| Physical and Chemical Indicators | Viscosity (10-1500cP) / density (600-1500kg/m³) / oil quality (1-100) / temperature (-35~+85℃) |
| Moisture | Water saturation (0.03-1Aw), water content (0.03 - 100%), water content (1-10000ppm) |
Product Introduction
SKA YJY12The mine intrinsically safe online oil monitoring instrument is composed of an oil quality data acquisition module (wear, viscosity, moisture, dielectric constant, temperature, density, and cleanliness sensors), an equipment status acquisition module (pressure, vibration, flow), a data processing module, and an IoT remote communication module. By installing online oil monitoring in the circulating return oil line of coal mine equipment, the system can realize real-time monitoring of the oil aging state of the lubrication system, gearbox transmission system, hydraulic system, etc. of coal mine mechanical equipment. With the internal oil aging model algorithm, it provides scientific monitoring data in real time on oil life status and equipment operating status, ensuring safe equipment operation. At the same time, the design of multiple communication protocols provides strong data support for data visualization in intelligent coal mines.
-
Track and monitor changes in oil quality to determine the degree of oil degradation and external contamination;
-
Real-time condition monitoring throughout the equipment's full life cycle, enabling condition-based maintenance and reducing maintenance costs;
-
Early fault identification and advanced alarms for preemptive system failure, improving operational safety;
-
Assist in equipment fault diagnosis and cause analysis, predict equipment failures, and reduce overall costs;
-
Avoid unplanned downtime and prevent major accidents;
-
Automatic vibration protection: when the set vibration value is exceeded, the system's oil monitoring automatically activates protection;
-
Automatic flow protection: oil monitoring data automatically activates protection with an accuracy of 1 ml/min;
-
Automatic leakage protection: when leakage is detected, the system structure automatically cuts off flow for protection with an accuracy of 0.1 ml;
-
It overcomes the deviation in monitoring results caused by uncertain changes in on-site working conditions such as pressure, flow, and vibration;
Main Application Areas
- Hydraulic Systems — Real-time monitoring of hydraulic oil condition in mining hydraulic supports and hydraulic pumps to prevent failures caused by oil contamination or aging.
- Gearbox Transmission Systems — Online tracking of gear oil quality in mining conveyors, crushers, and hoists to ensure reliable transmission and extend equipment life.
- Lubrication Systems — Continuous assessment of lubricant degradation in centralized lubrication systems of mining machinery to reduce wear and maintenance costs.
- Coal Mining Equipment — Oil condition monitoring for shearers, roadheaders, and other coal mining equipment to ensure safe and efficient operation.
- Industrial Machinery — Applicable to various industrial machines requiring oil monitoring, such as compressors, turbines, and hydraulic power units.
Keywords:intrinsically safe oil monitor, mining oil monitoring instrument, online oil analysis system, oil condition monitoring, oil contamination sensor, oil viscosity sensor, oil moisture sensor, mining equipment oil monitoring